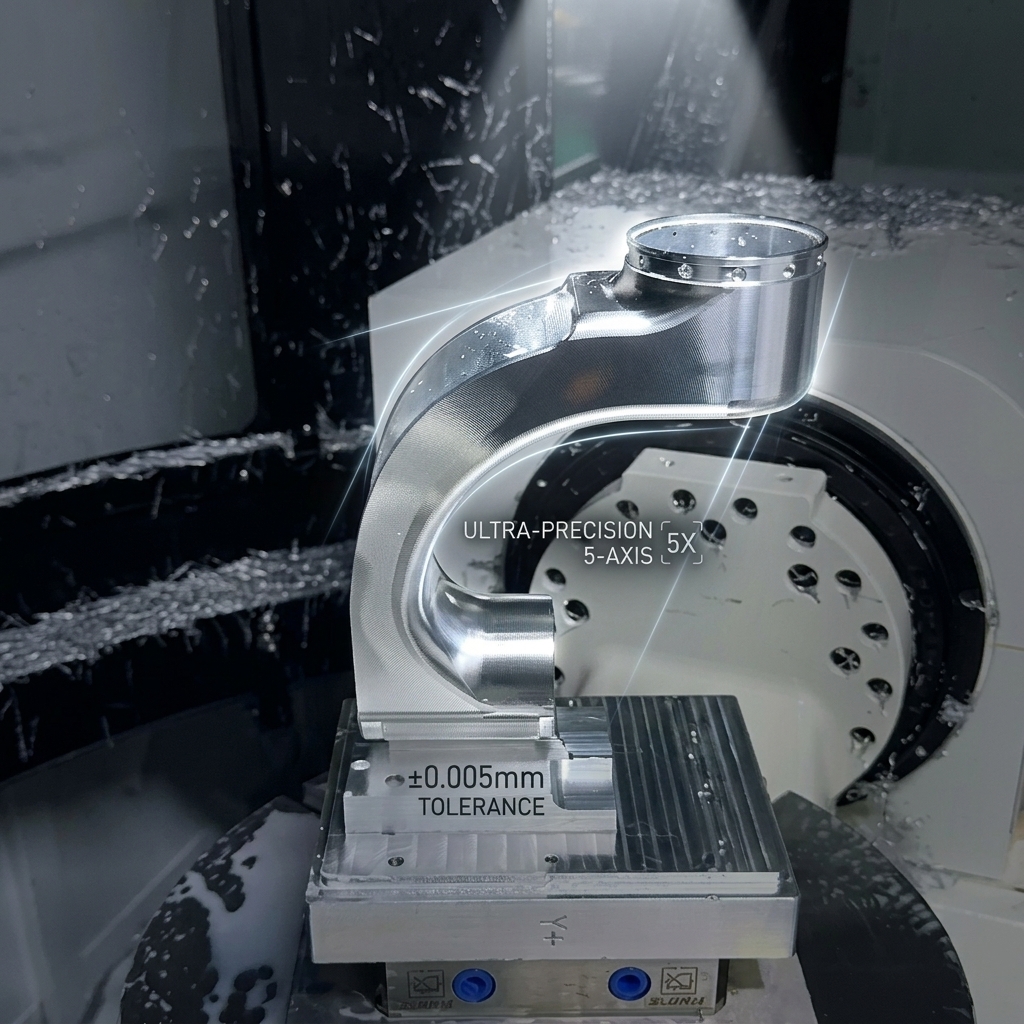
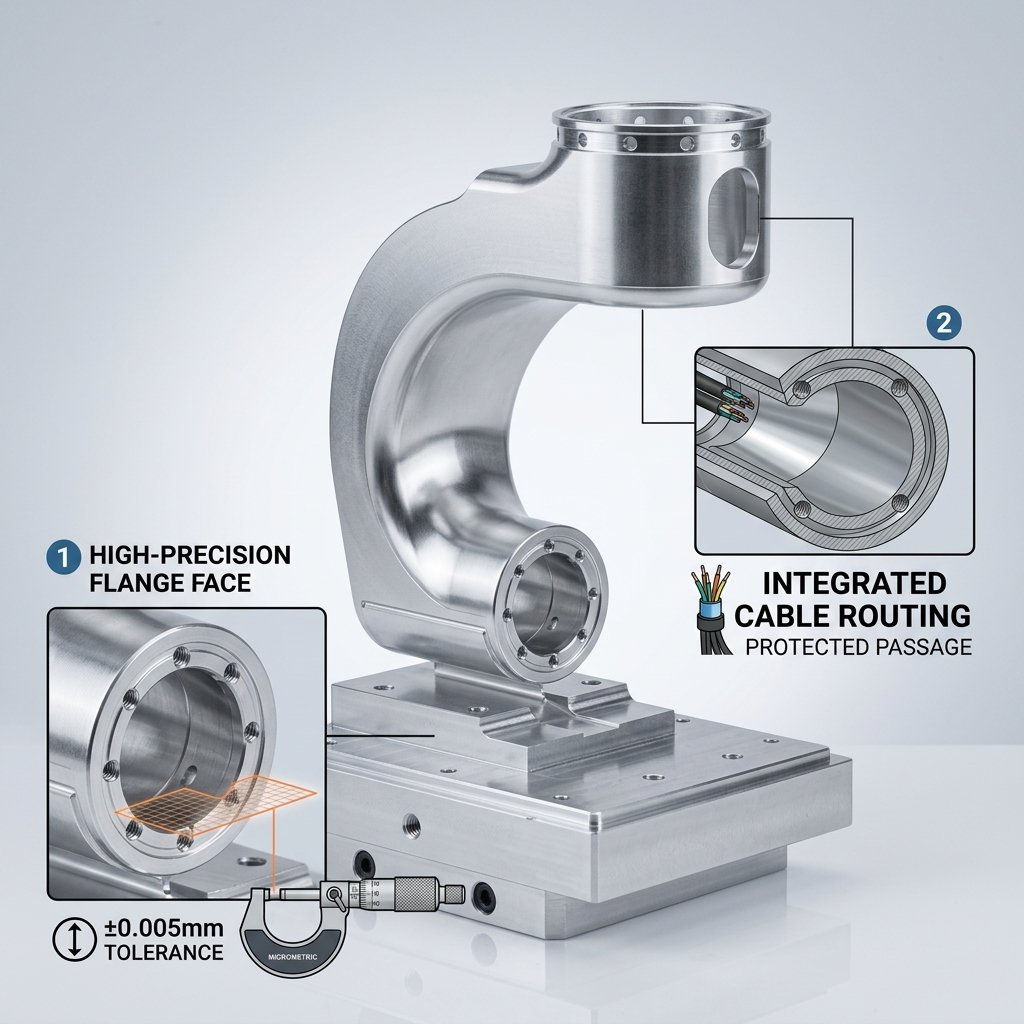
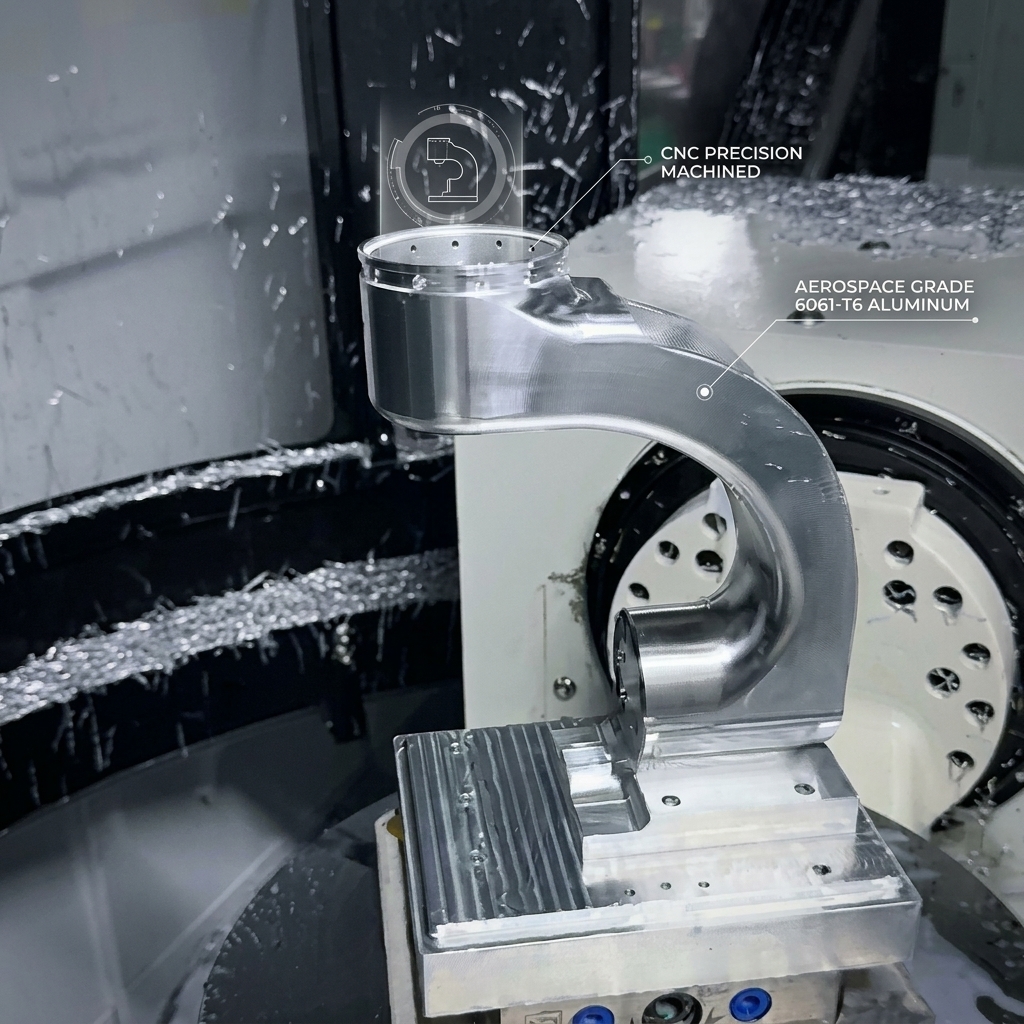
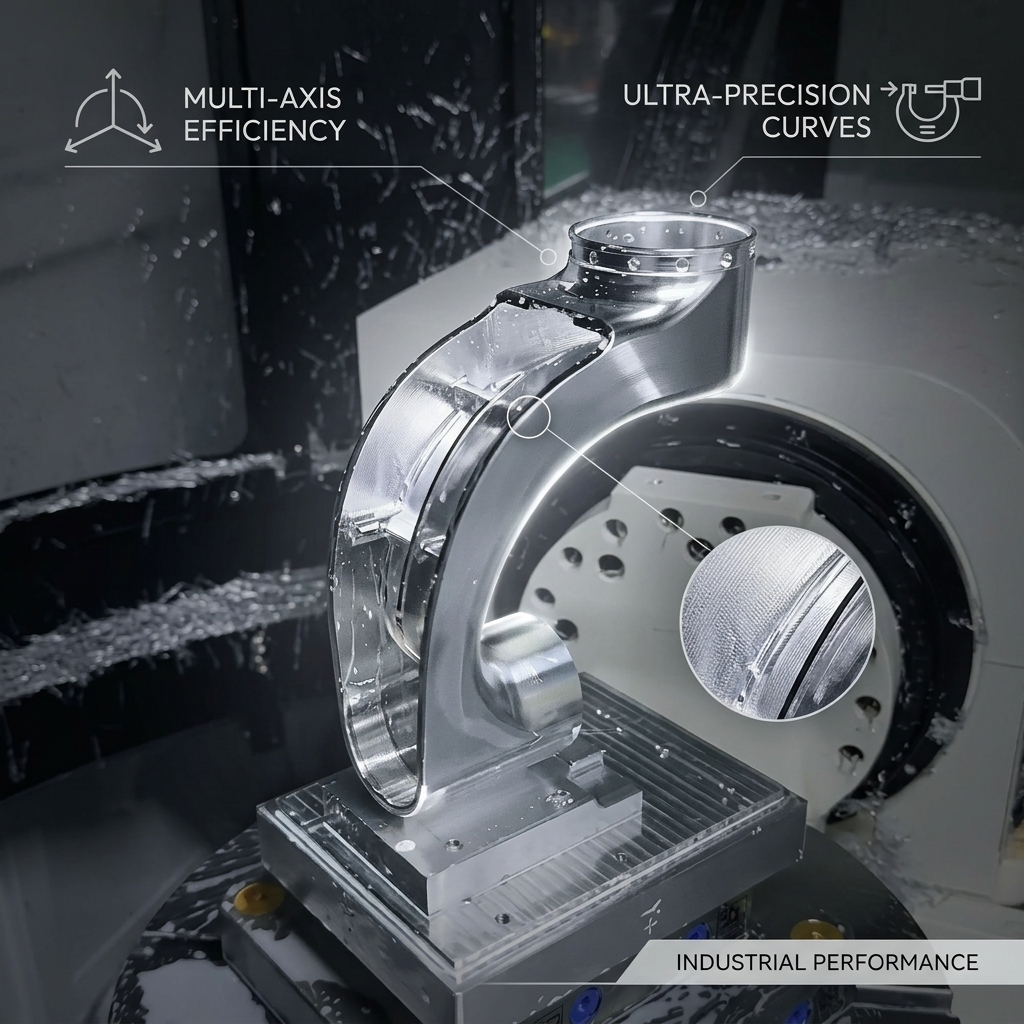
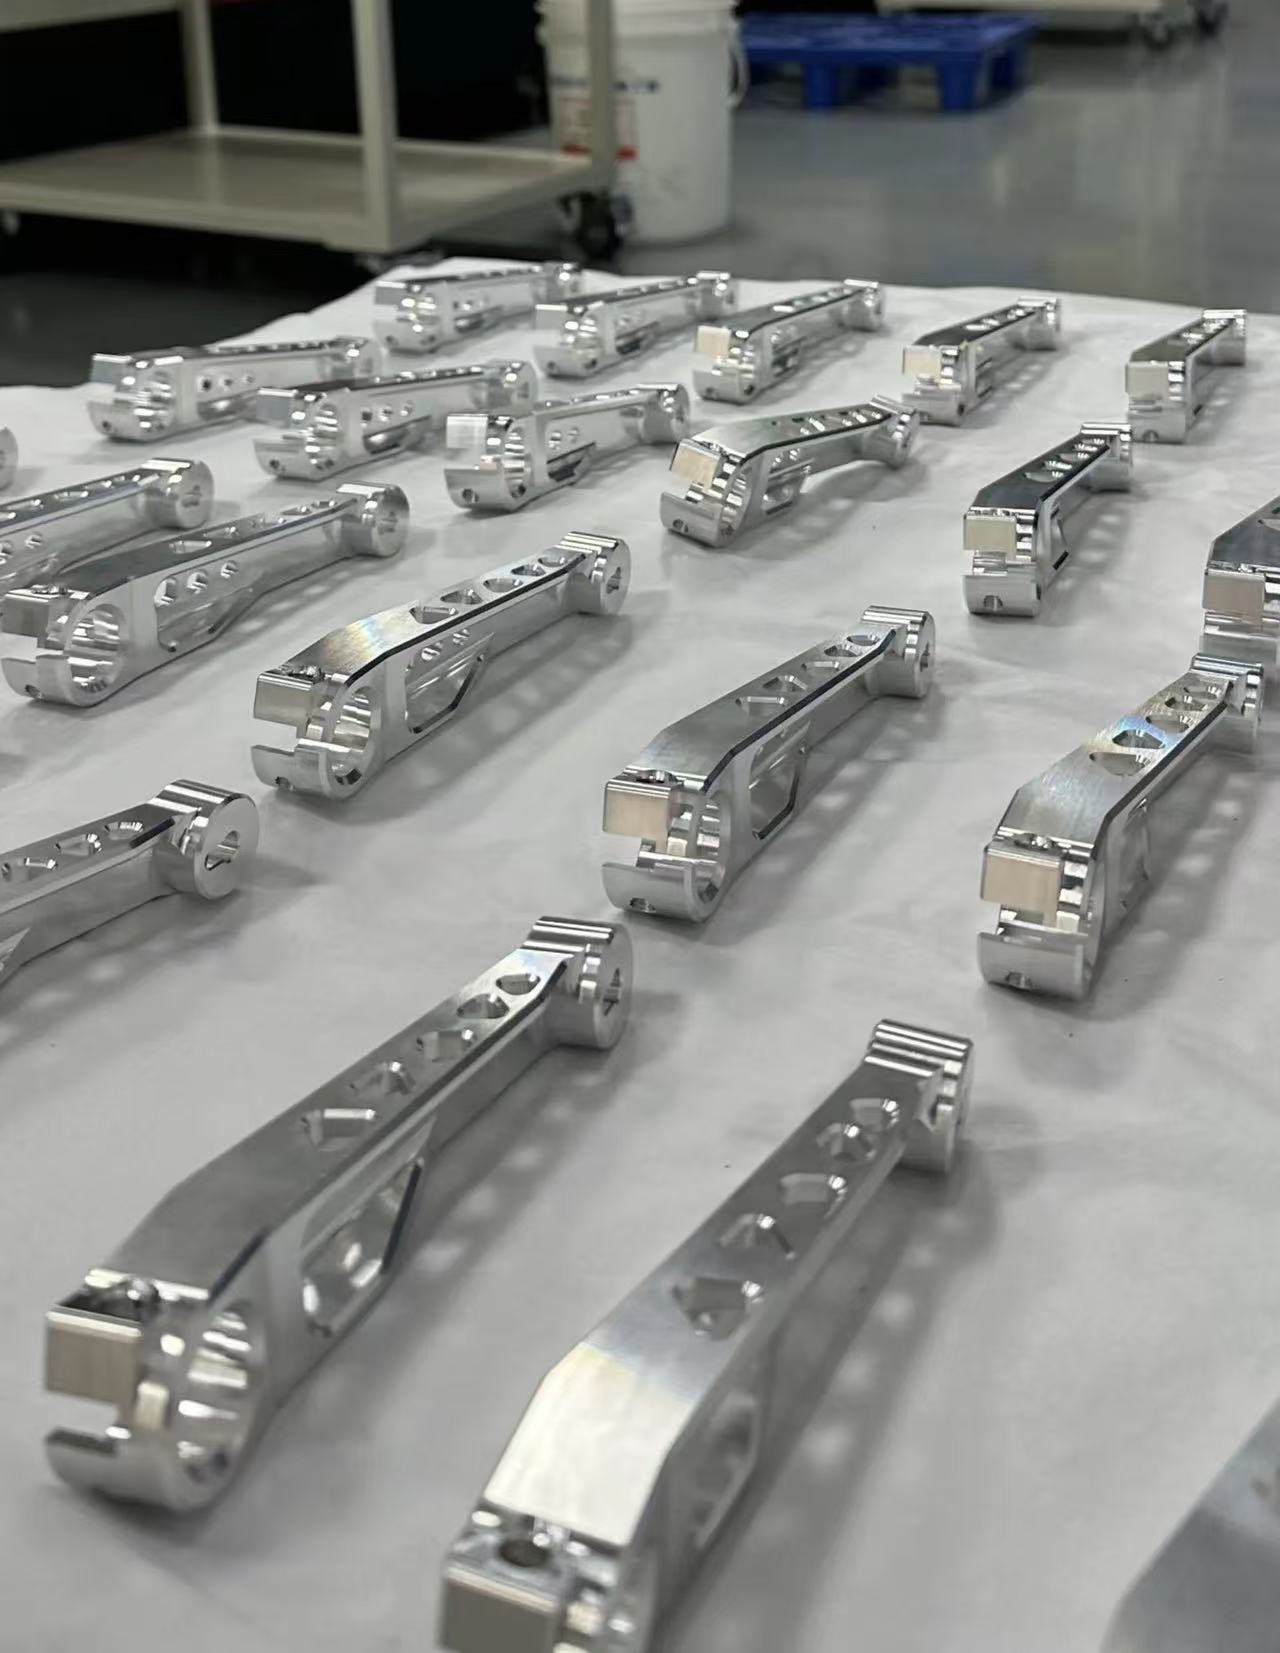
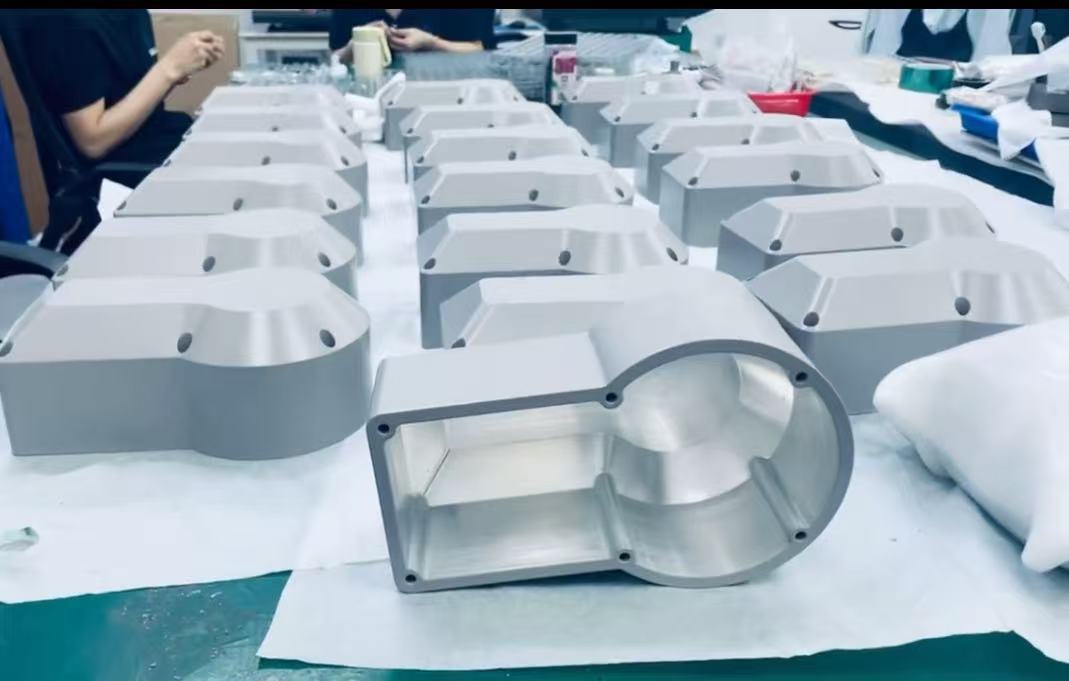
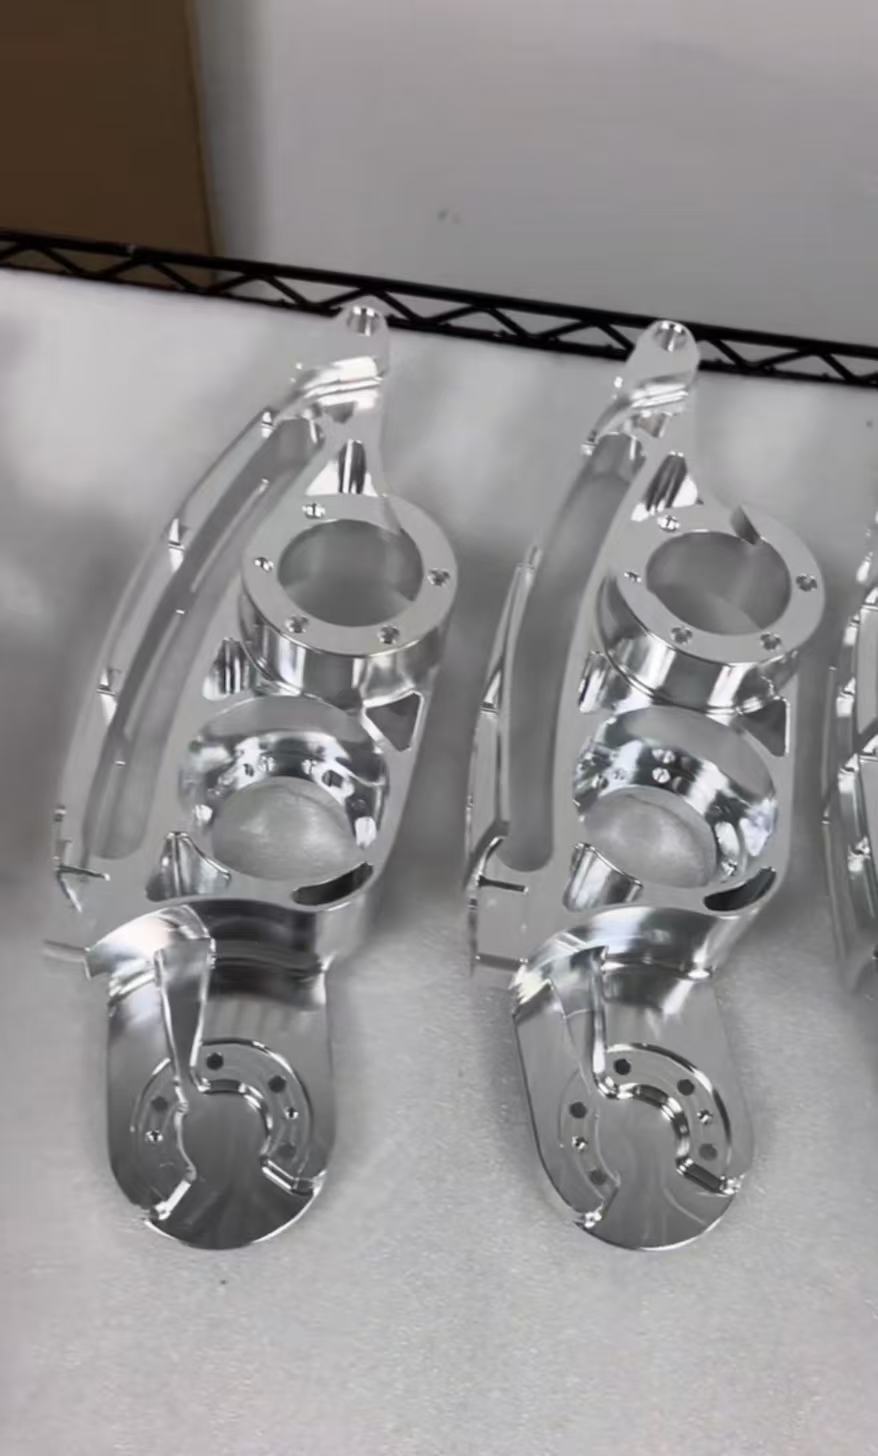
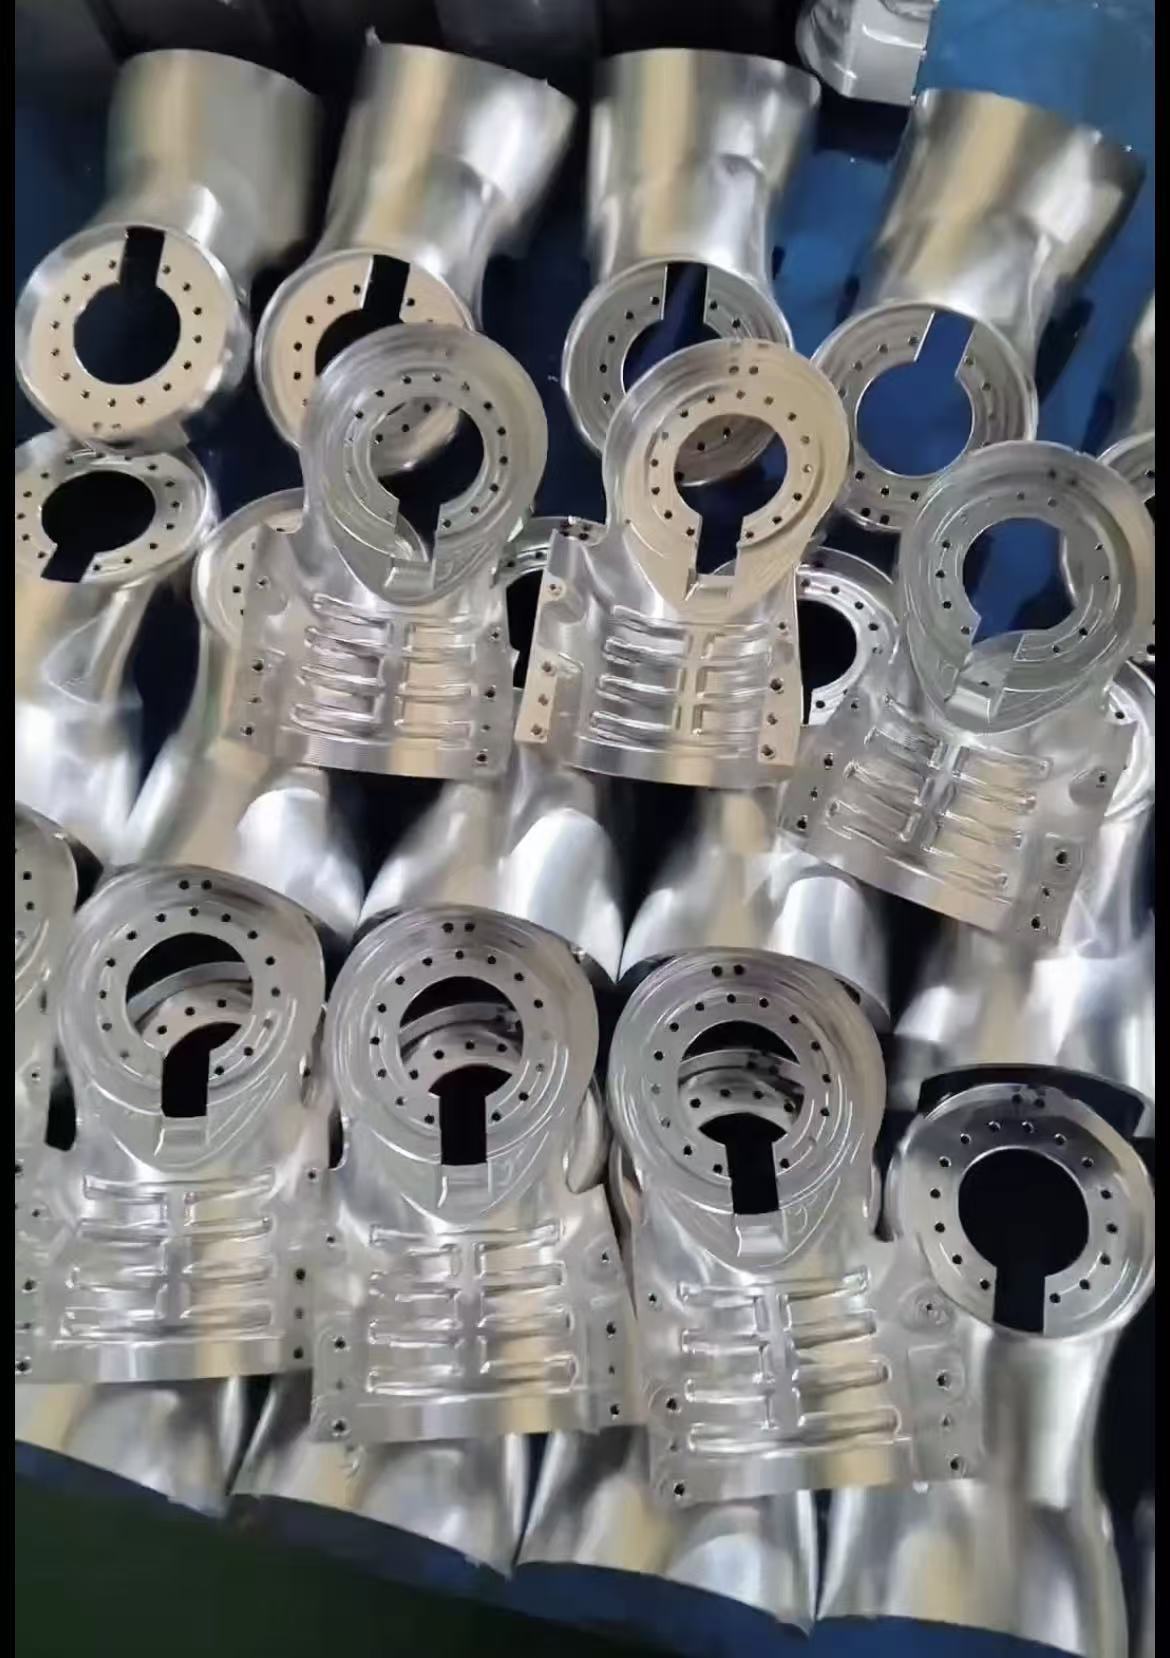
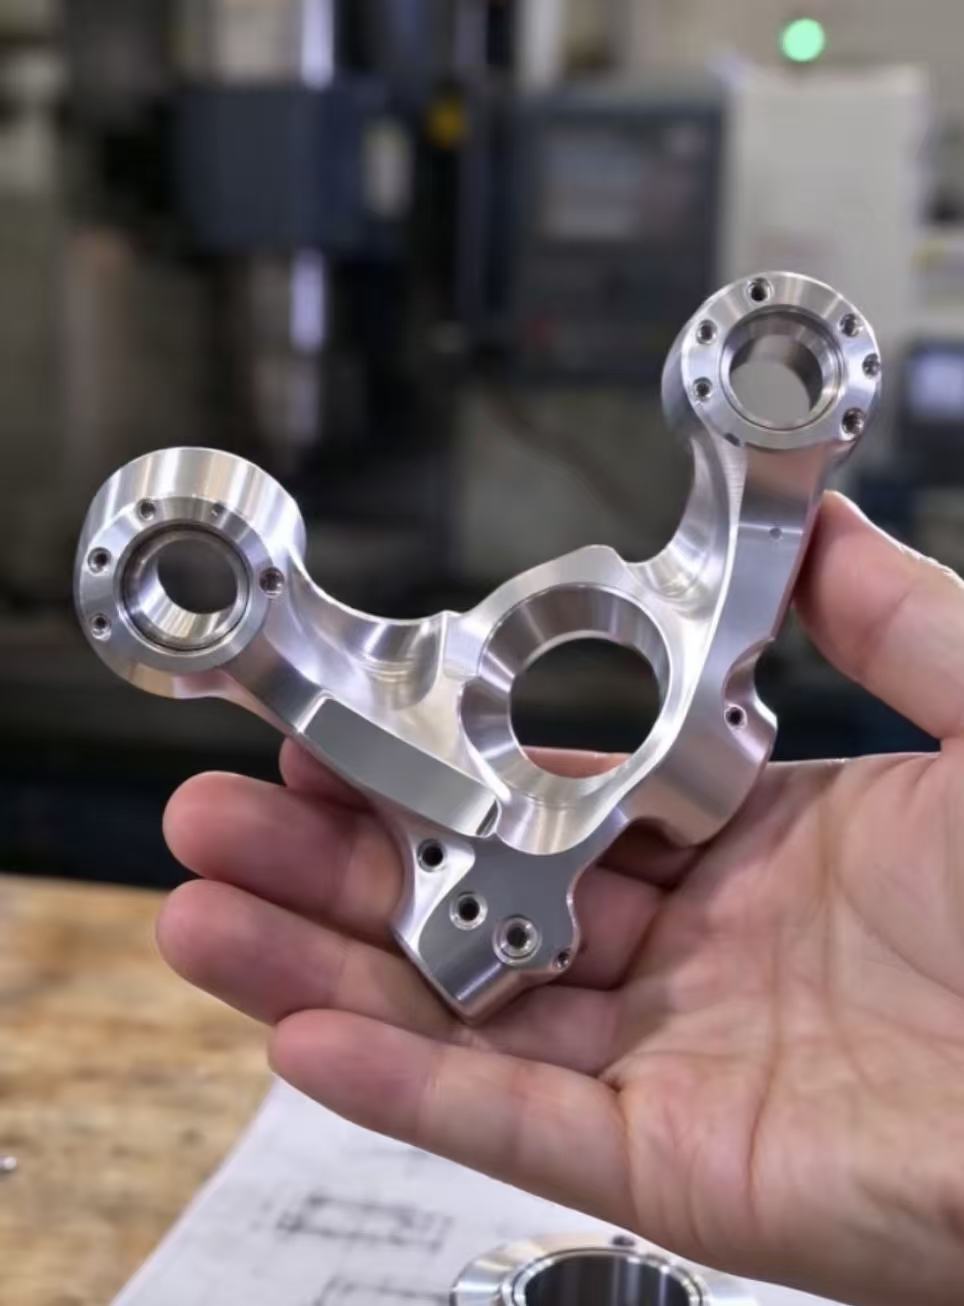
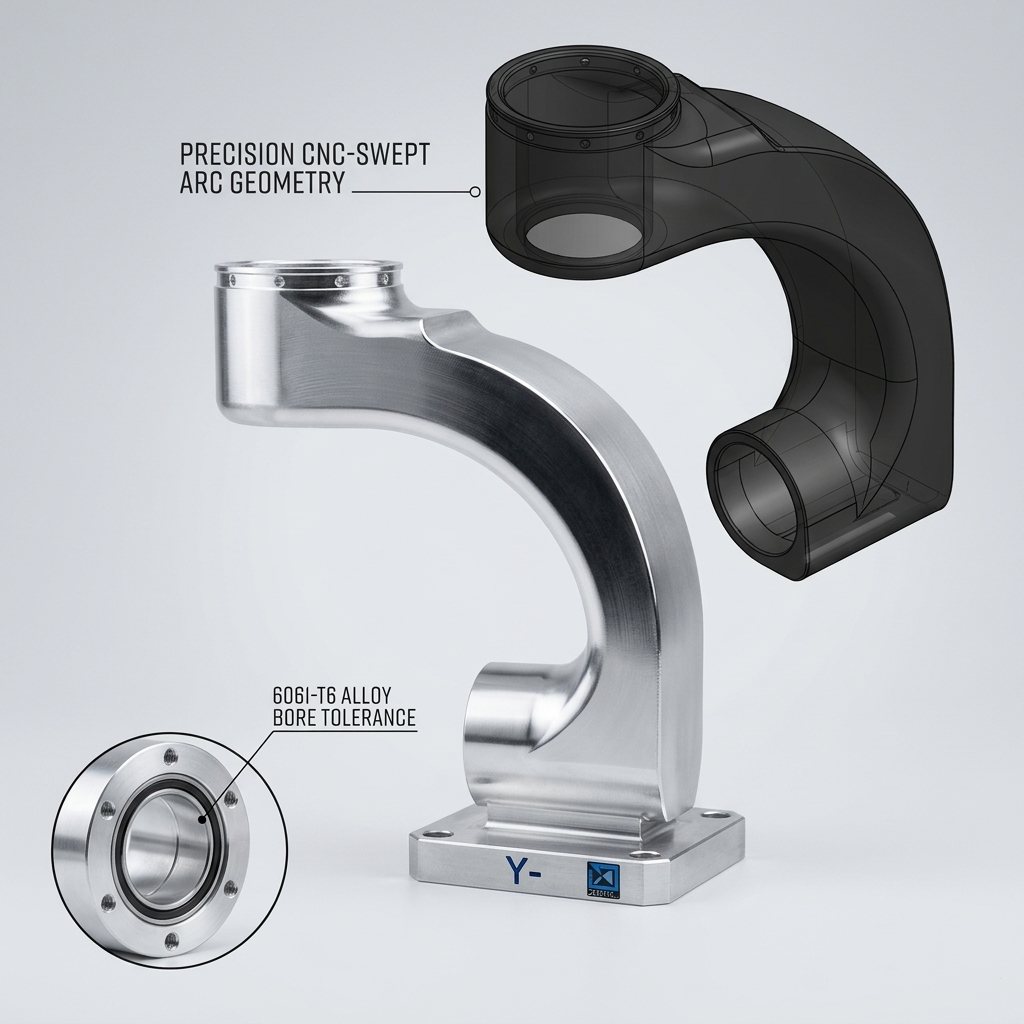
This wrist flange arm housing closes the kinematic chain at the end of a robot arm: the flange face carries the tool or gripper, the hollow barrel routes the cable harness, and the offset mounting pad picks up the wrist reducer. Machining is done from 6061-T6 aluminium in a single five-axis setup so the flange register, the barrel bore and the offset pad stay in one coordinate system; a second setup here would shift the tool centre point and show up as run-out at the gripper.
The housing is delivered with a CMM report covering flange perpendicularity, bore roundness and pad position, and with the material certificate matched to the batch.
The barrel wall between the cable window and the flange is the weak point: removing that window leaves an interrupted, unsupported shell that deflects under side milling force, and the flange face then springs out of flat after the part is released from the fixture. We pre-machine the window in the roughing stage rather than after finishing, support the barrel with an expanding mandrel, keep axial depth light and constant around the window, and add a stress-relief pause before the finish pass. The result is a flange that stays within 0.02 mm flatness and a bore that stays round within 0.01 mm after clamping is released.
Flange register, barrel bore and reducer pad machined in one clamping, so run-out at the tool centre point is minimised.
Internal barrel window passes encoder and motor cables without external conduit or abrasion risk.
Expanding mandrel support and staged roughing keep the window shell stable through finishing.
Hard anodized flange face resists fretting where grippers are changed many times per shift.
| Material | 6061-T6 aluminium block (7075-T6 available for higher stiffness) |
|---|---|
| Machining | Five-axis CNC milling, one clamping, indexed plus simultaneous motion |
| Flange flatness | 0.02 mm after release from fixture |
| Bore roundness | 0.01 mm, concentricity to flange register 0.015 mm |
| Threads | Metric coarse and fine, verified with go/no-go gauges |
| Finish options | Bead blasting, clear or black anodizing, hard anodizing on flange face |
| Inspection | CMM report, thread gauge record, material certificate |
| Packing | Flange face protected with PE film, foam cradle, export carton on pallet |
Provide a 3D model with the flange standard you use, the payload rating, the cable bundle diameter and the required anodizing colour. We quote sampling and series price separately, machine the first article for your fit check, and keep the program and fixture on file so repeat orders run without a new setup. Both prototype quantities and monthly series batches are handled in the same shop.
Upload your wrist housing model and quantity - we will confirm feasibility, finish options and lead time the same week.