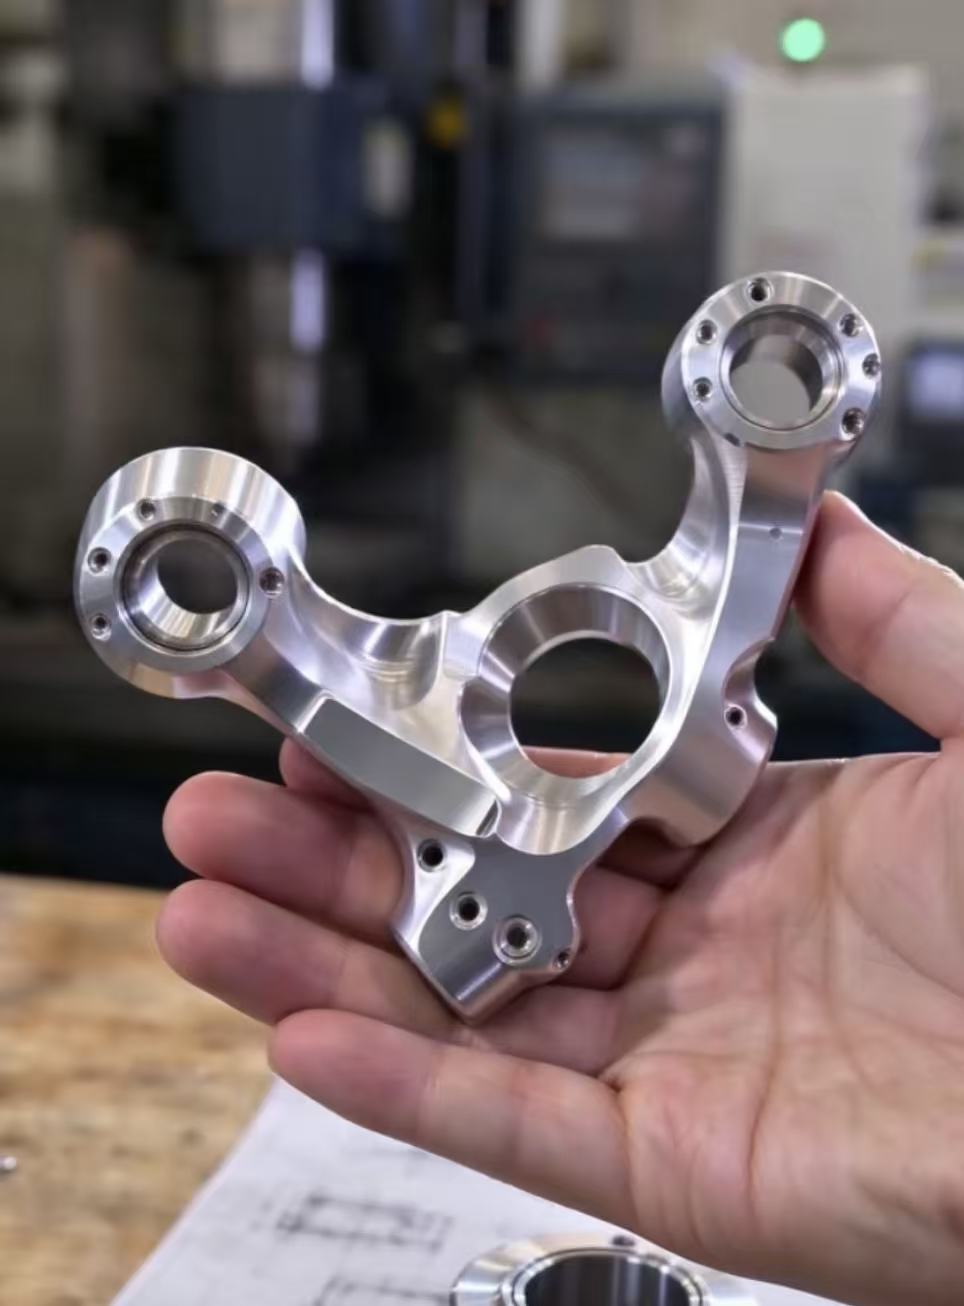
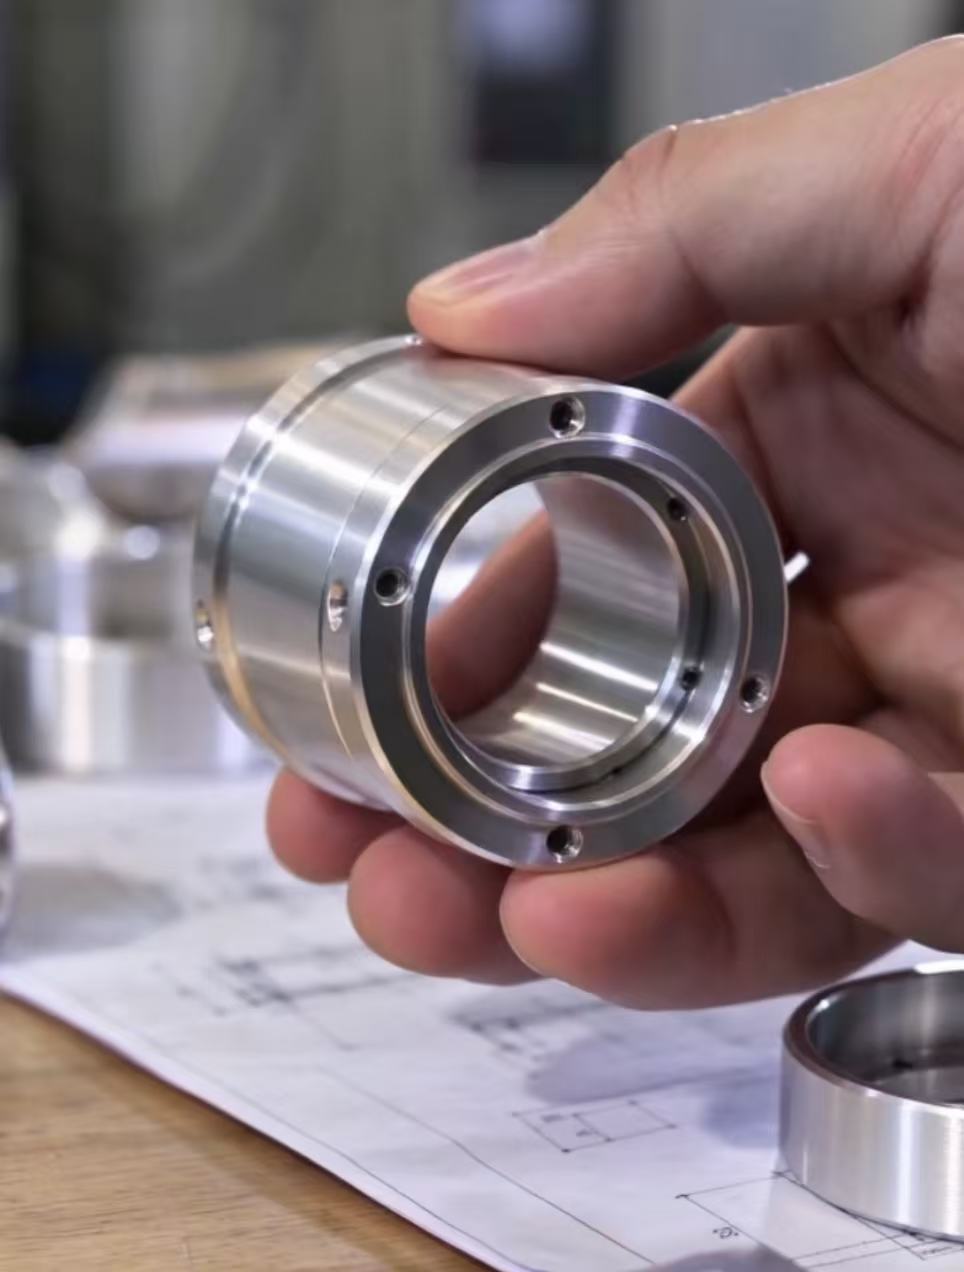
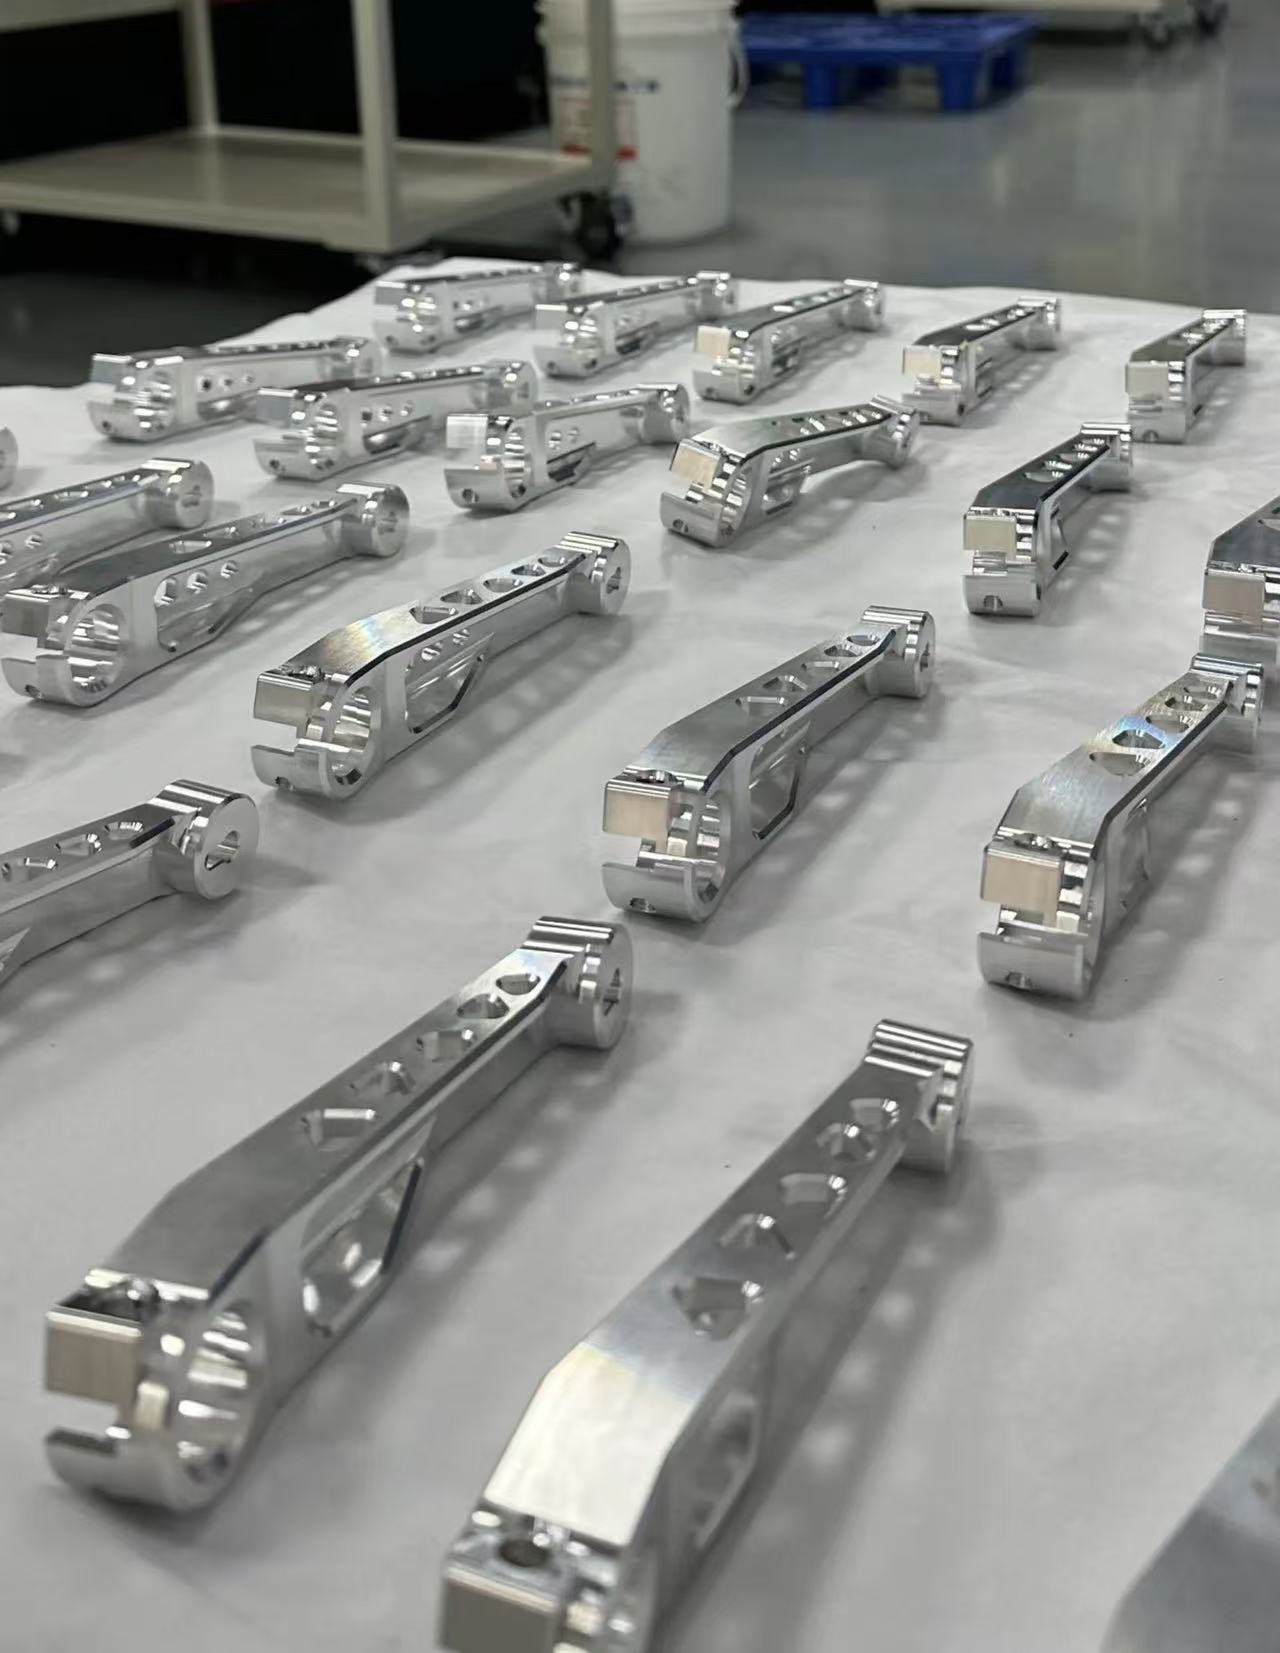
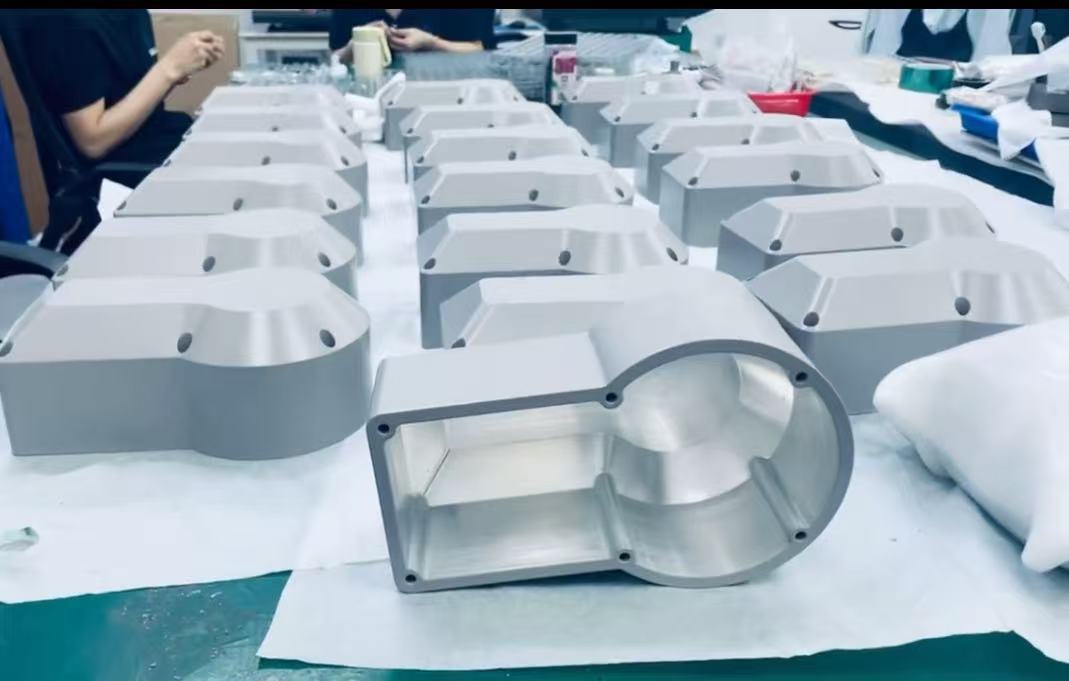
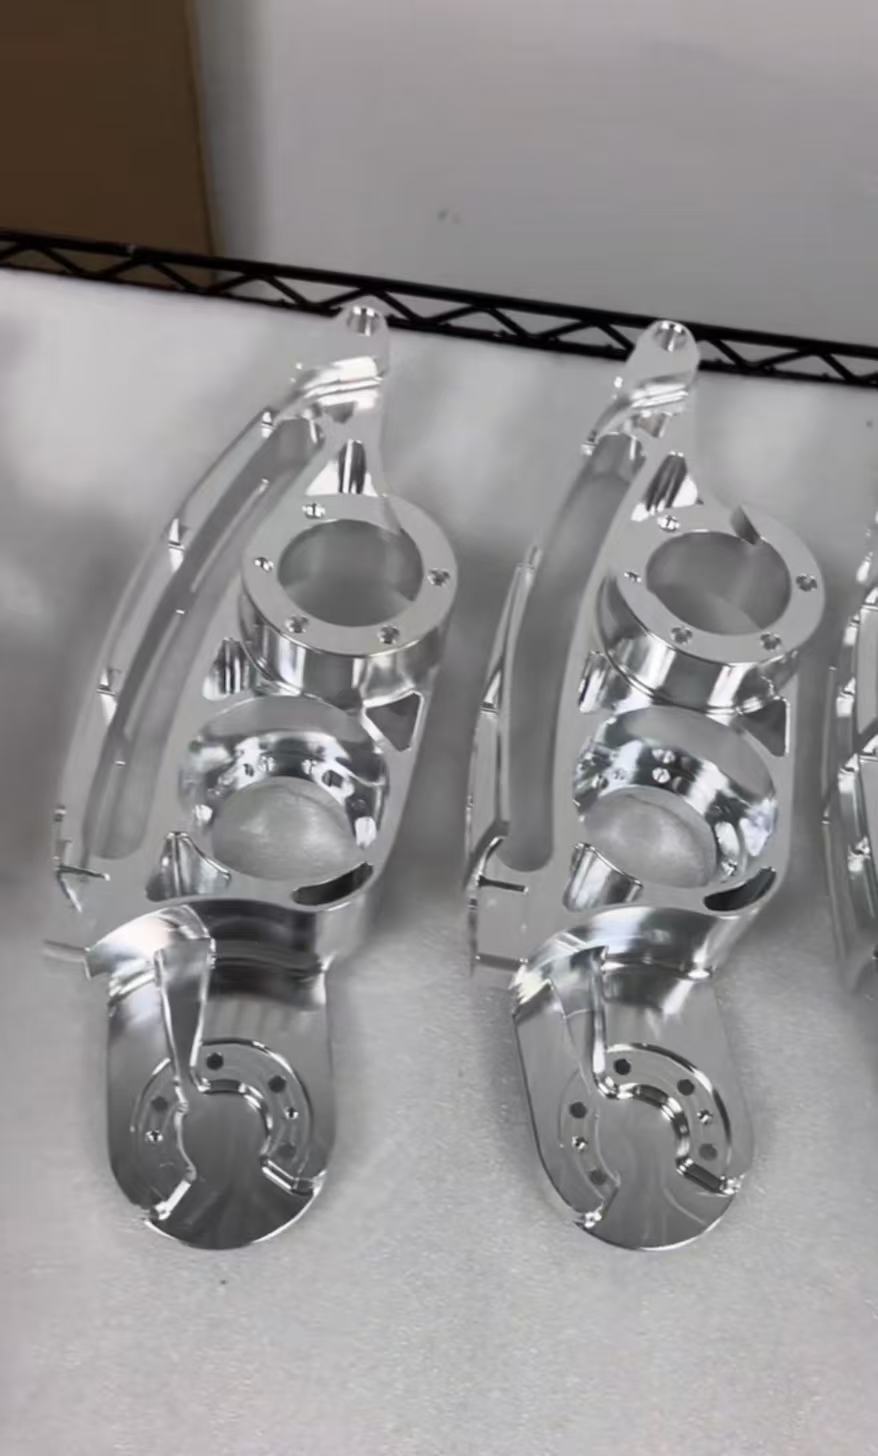
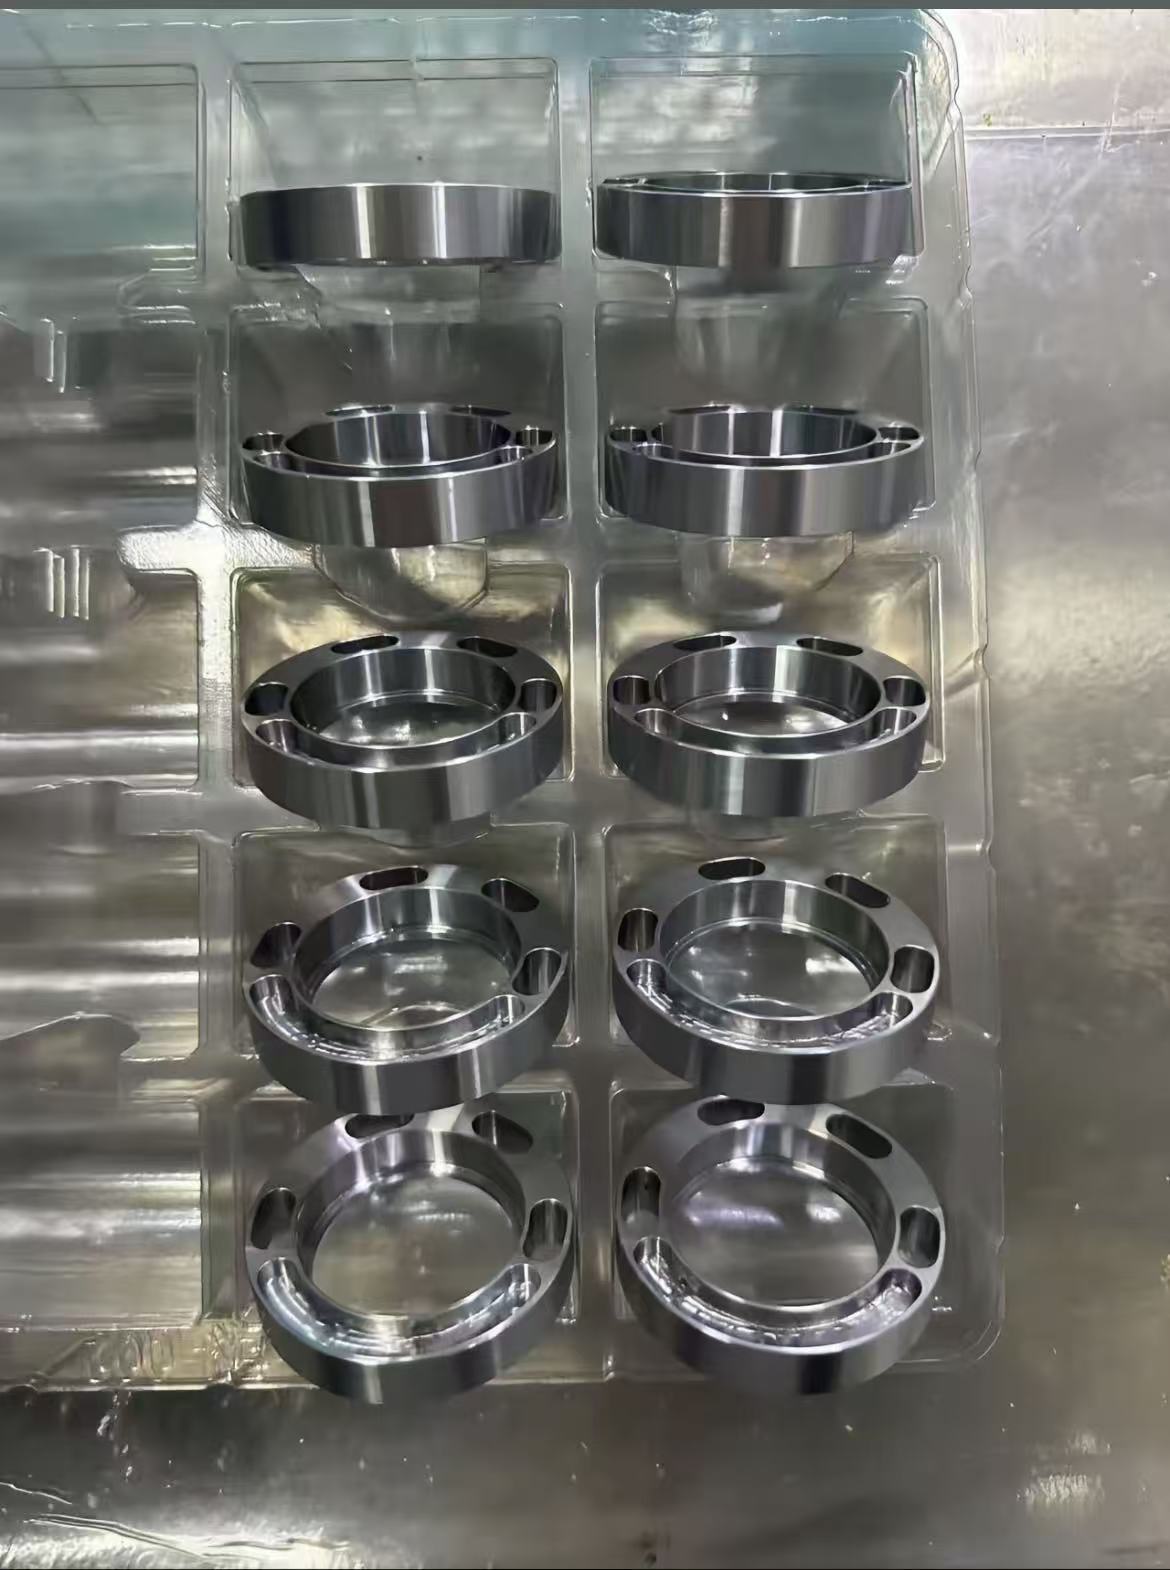
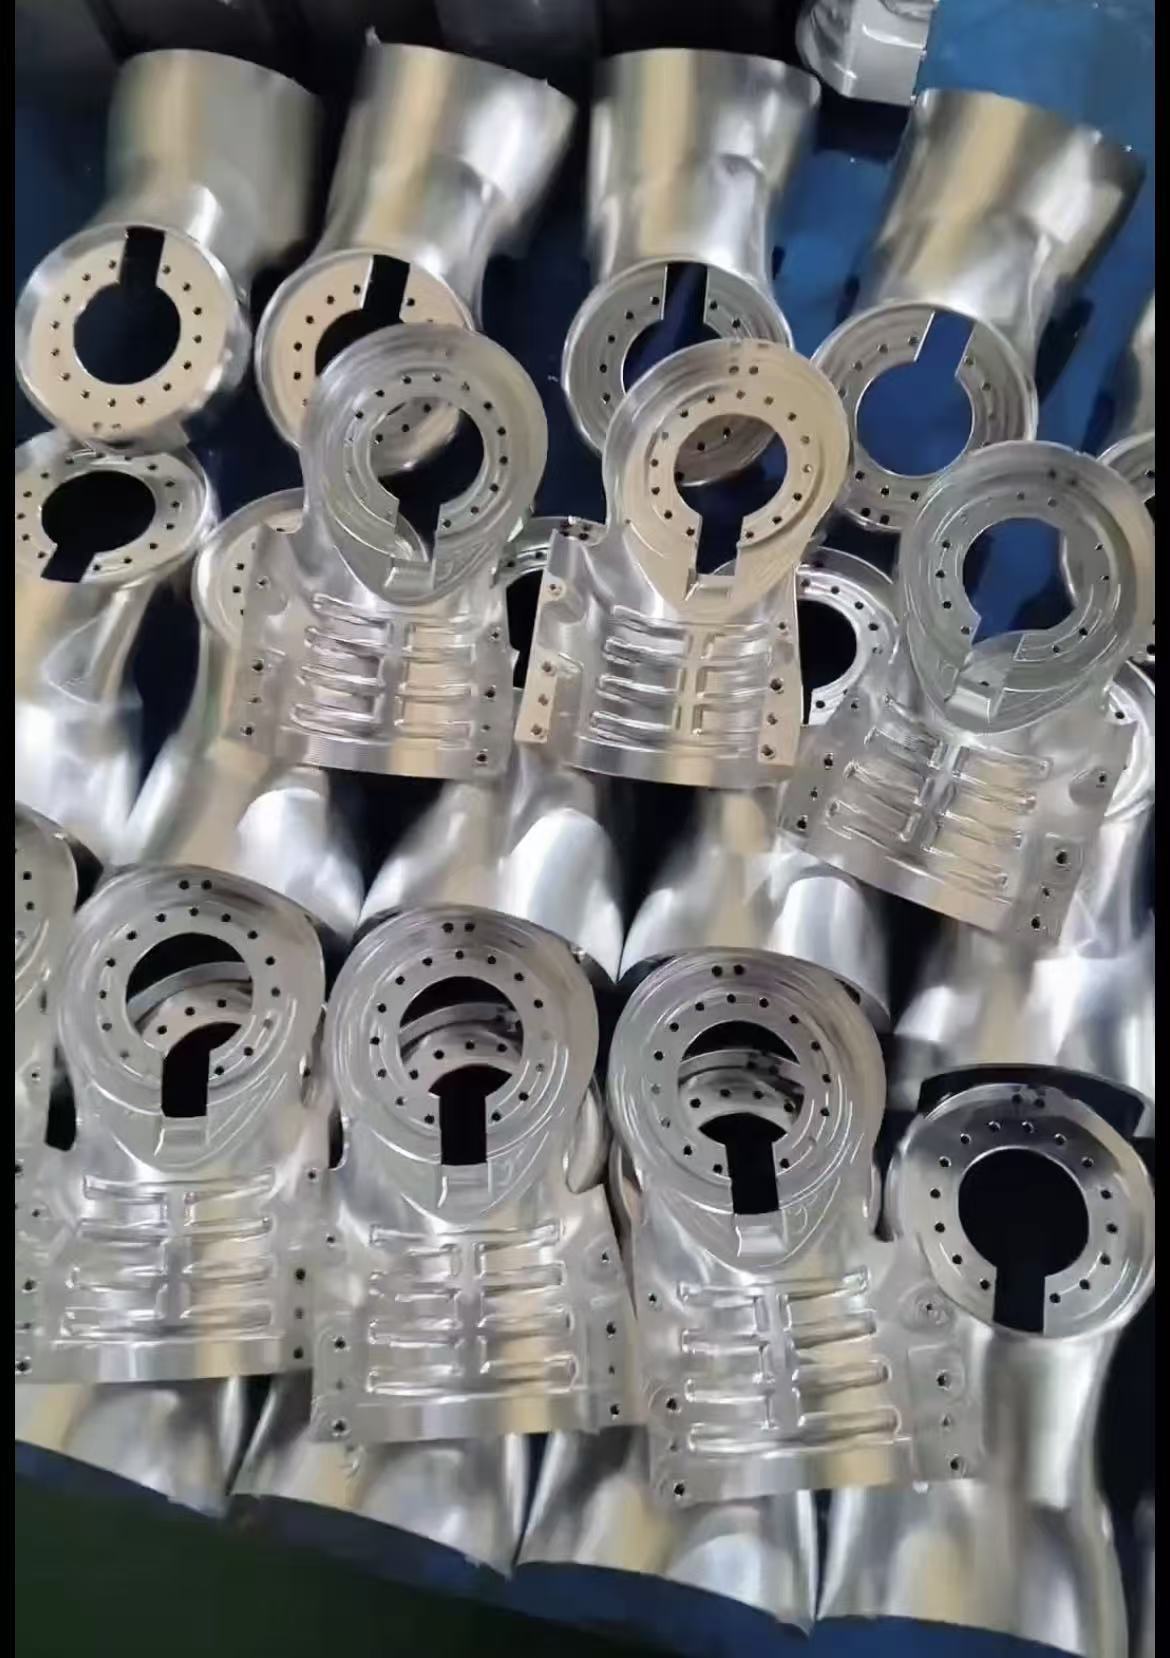
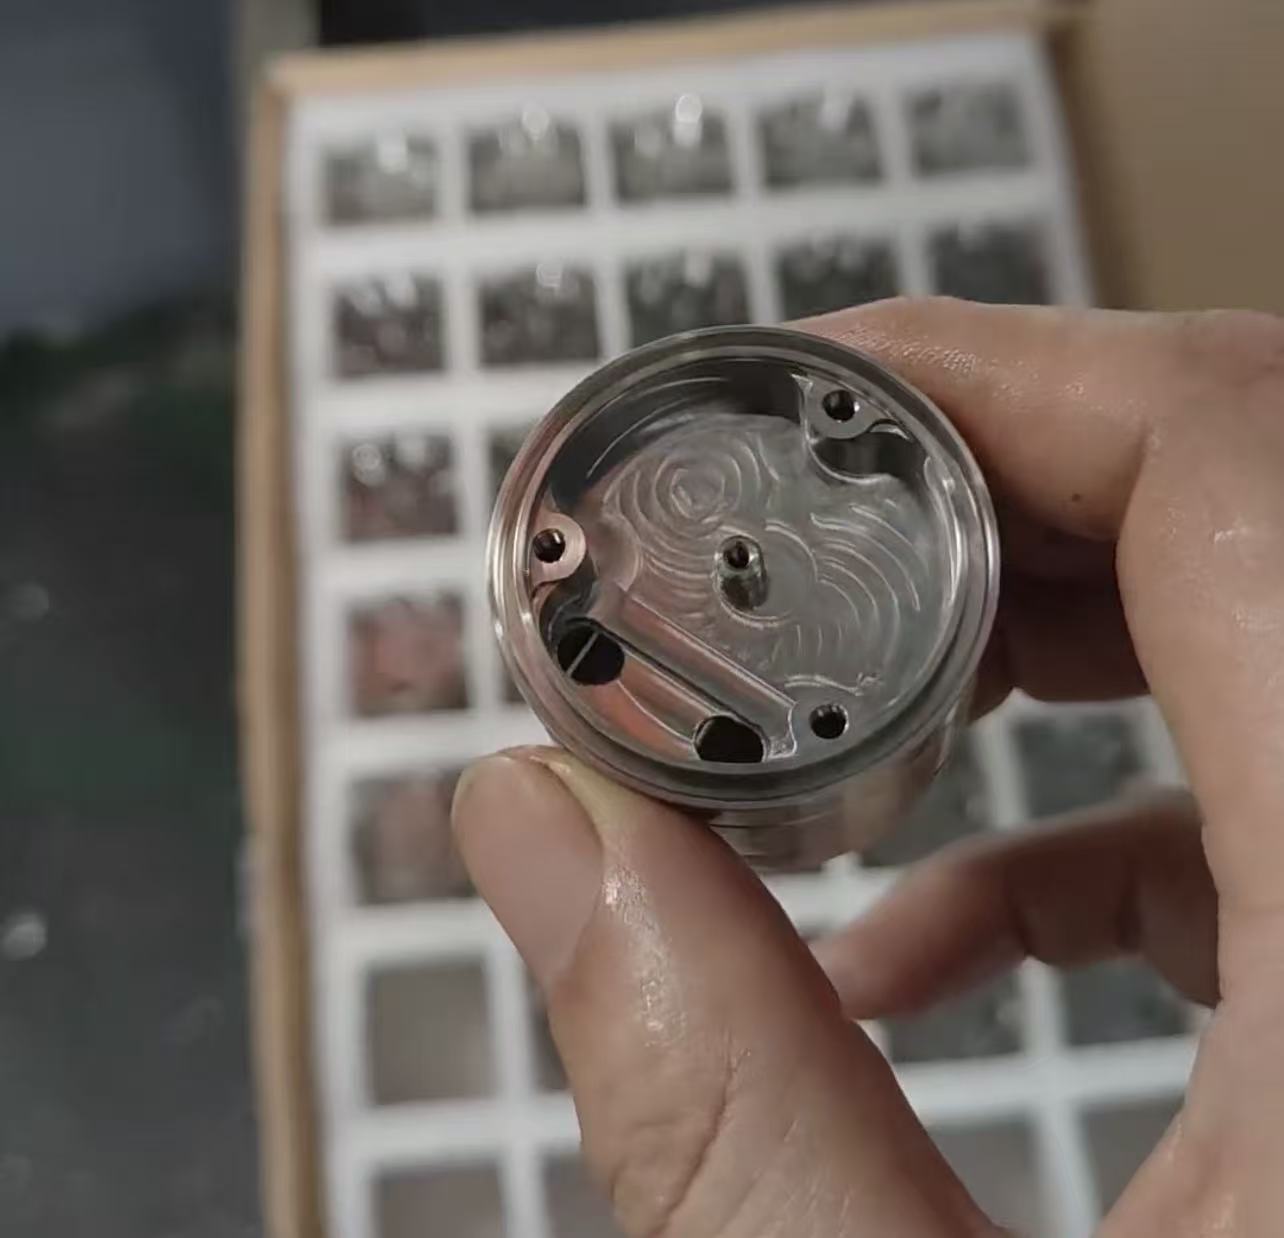
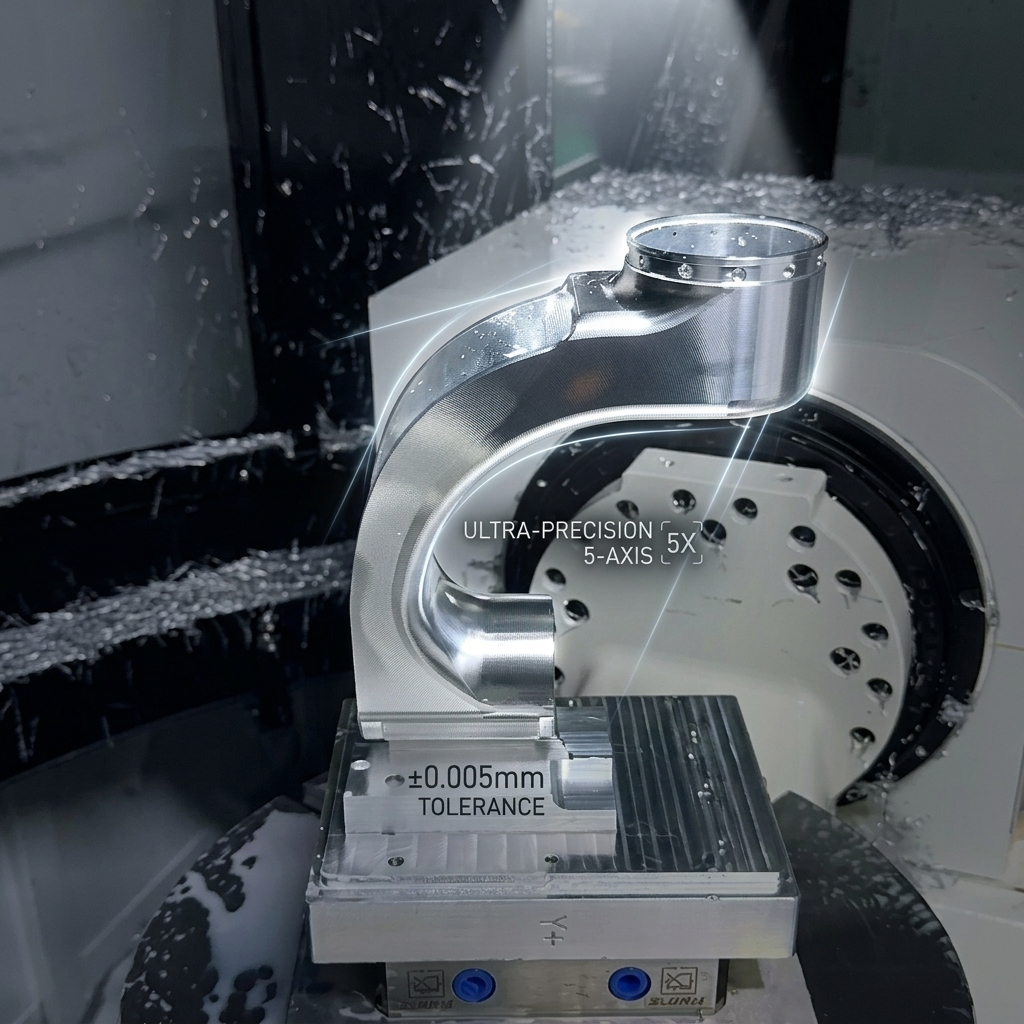
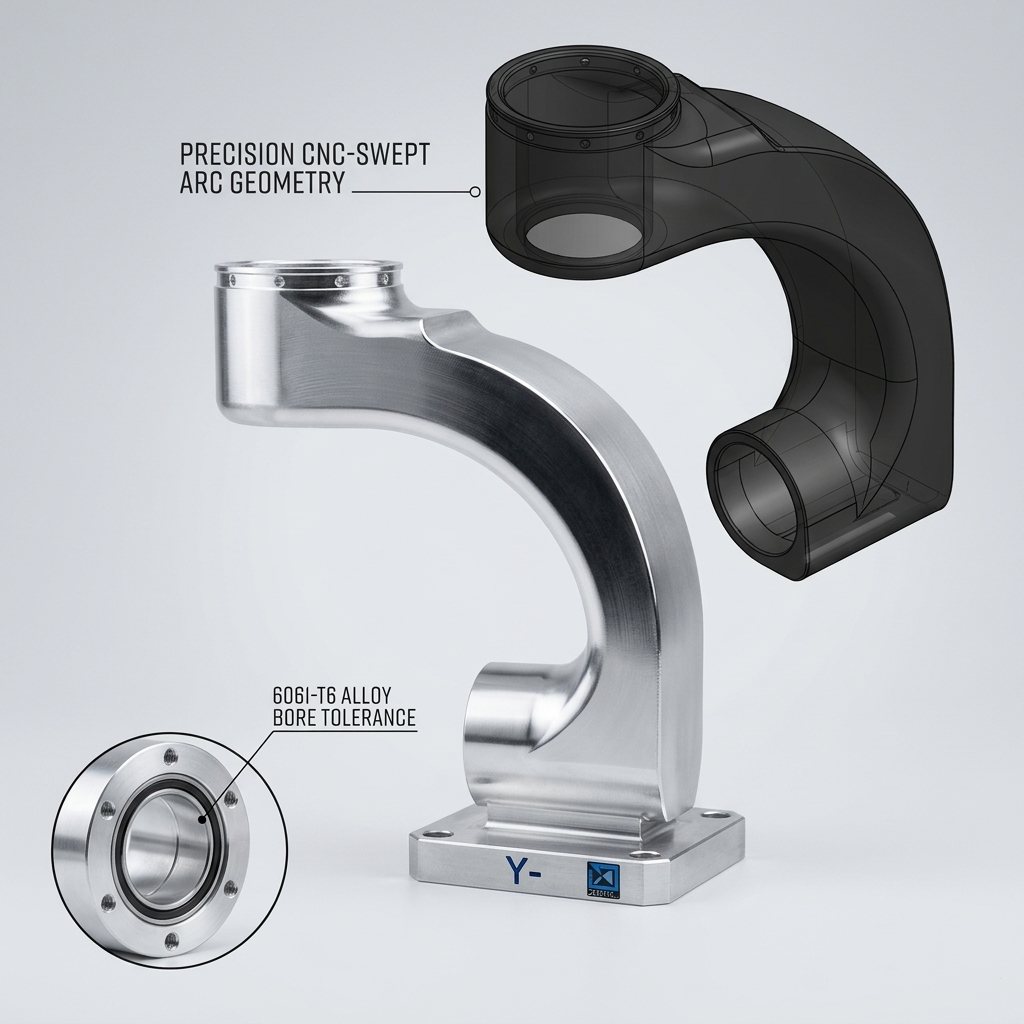
These machined parts are the structural hardware of a working robot: joint links, mounting plates, reducer housings, base brackets and end-effector fixtures that carry load, hold alignment and survive thousands of cycles without play. Our machine shop has built its business around exactly this kind of component, and we machine them from 6061 and 7075 aluminium, 304 and 316 stainless steel, brass and engineering plastics, holding ±0.01 mm on critical features and delivering on a schedule we commit to in writing.
We work from your 3D model, not from a verbal description. Every project starts with drawing analysis and process planning so that datums, clamping strategy, tool paths and inspection method are decided before the first chip is cut.
Held on bores, spigots, bearing seats and mating faces, verified on a coordinate measuring machine and recorded per batch.
Simultaneous five-axis milling for curved shells, angled ports and complex cavities that cannot be reached in three setups.
Dedicated fixtures and soft jaws control clamping distortion, so thin walls stay round and flat after the part is released.
Material certificate, program revision, finish batch and CMM report are filed against every delivery.
Phone, tablet and notebook housings, heat sinks, camera brackets, VR and AR headset structural parts, smart wearable shells.
Automation fixtures, jigs, module frames, linear guide blocks, motor mounts, sensor housings, production line components.
Vacuum chambers, vacuum fittings, precision bases, thermal and insulating parts, inspection tooling.
Surgical instrument bases, diagnostic instrument housings, endoscope components, aesthetic device frames in medical-grade aluminium and stainless steel.
New energy motor housings, battery end plates, sensor brackets, lighting structural parts, aftermarket components, hydraulic valve blocks.
Aircraft structural parts, drone frames, landing gear components, avionics instrument housings in lightweight precision aluminium.
Lens barrels, lens mounts, light source heat sinks, camera module brackets, optical inspection platforms.
5G heat dissipation cavities, filter components, signal transition parts, telecom equipment housings.
Robot arm joint parts, robot bases, reducer housings, AGV structural components, end effector and gripper hardware.
Test equipment housings, precision gauge bases, flow meter parts, laboratory equipment components.
Every tool path mark you see on a finished surface is a record of a decision: spindle speed, step-over, radial engagement, fixture support. That is why our parts hold tolerance at the hundredth of a millimetre and why the tenth batch measures the same as the first.
One-off prototypes are handled with the same fixtures and inspection routine as a ten-thousand-piece program, so design validation data stays meaningful. Small batches from ten to a few hundred pieces are economically machined because our setup time is planned rather than improvised. For series production we lock the program, keep the fixture on file, and run first-article approval before volume starts.
Send a 3D model with the tolerance callouts, material grade, surface finish and annual demand. You will receive a manufacturability review, a quotation and a lead time commitment, usually within two working days. If you are still at design stage, we can quote from a 2D drawing and propose geometry changes that reduce machining cost.
Upload your drawing for a DFM review and quotation - prototypes in days, series production on a committed schedule.