TEMA Heat Exchanger HP LT Preheater Shell and Tube Heat Exchanger Straight Tube Bundle
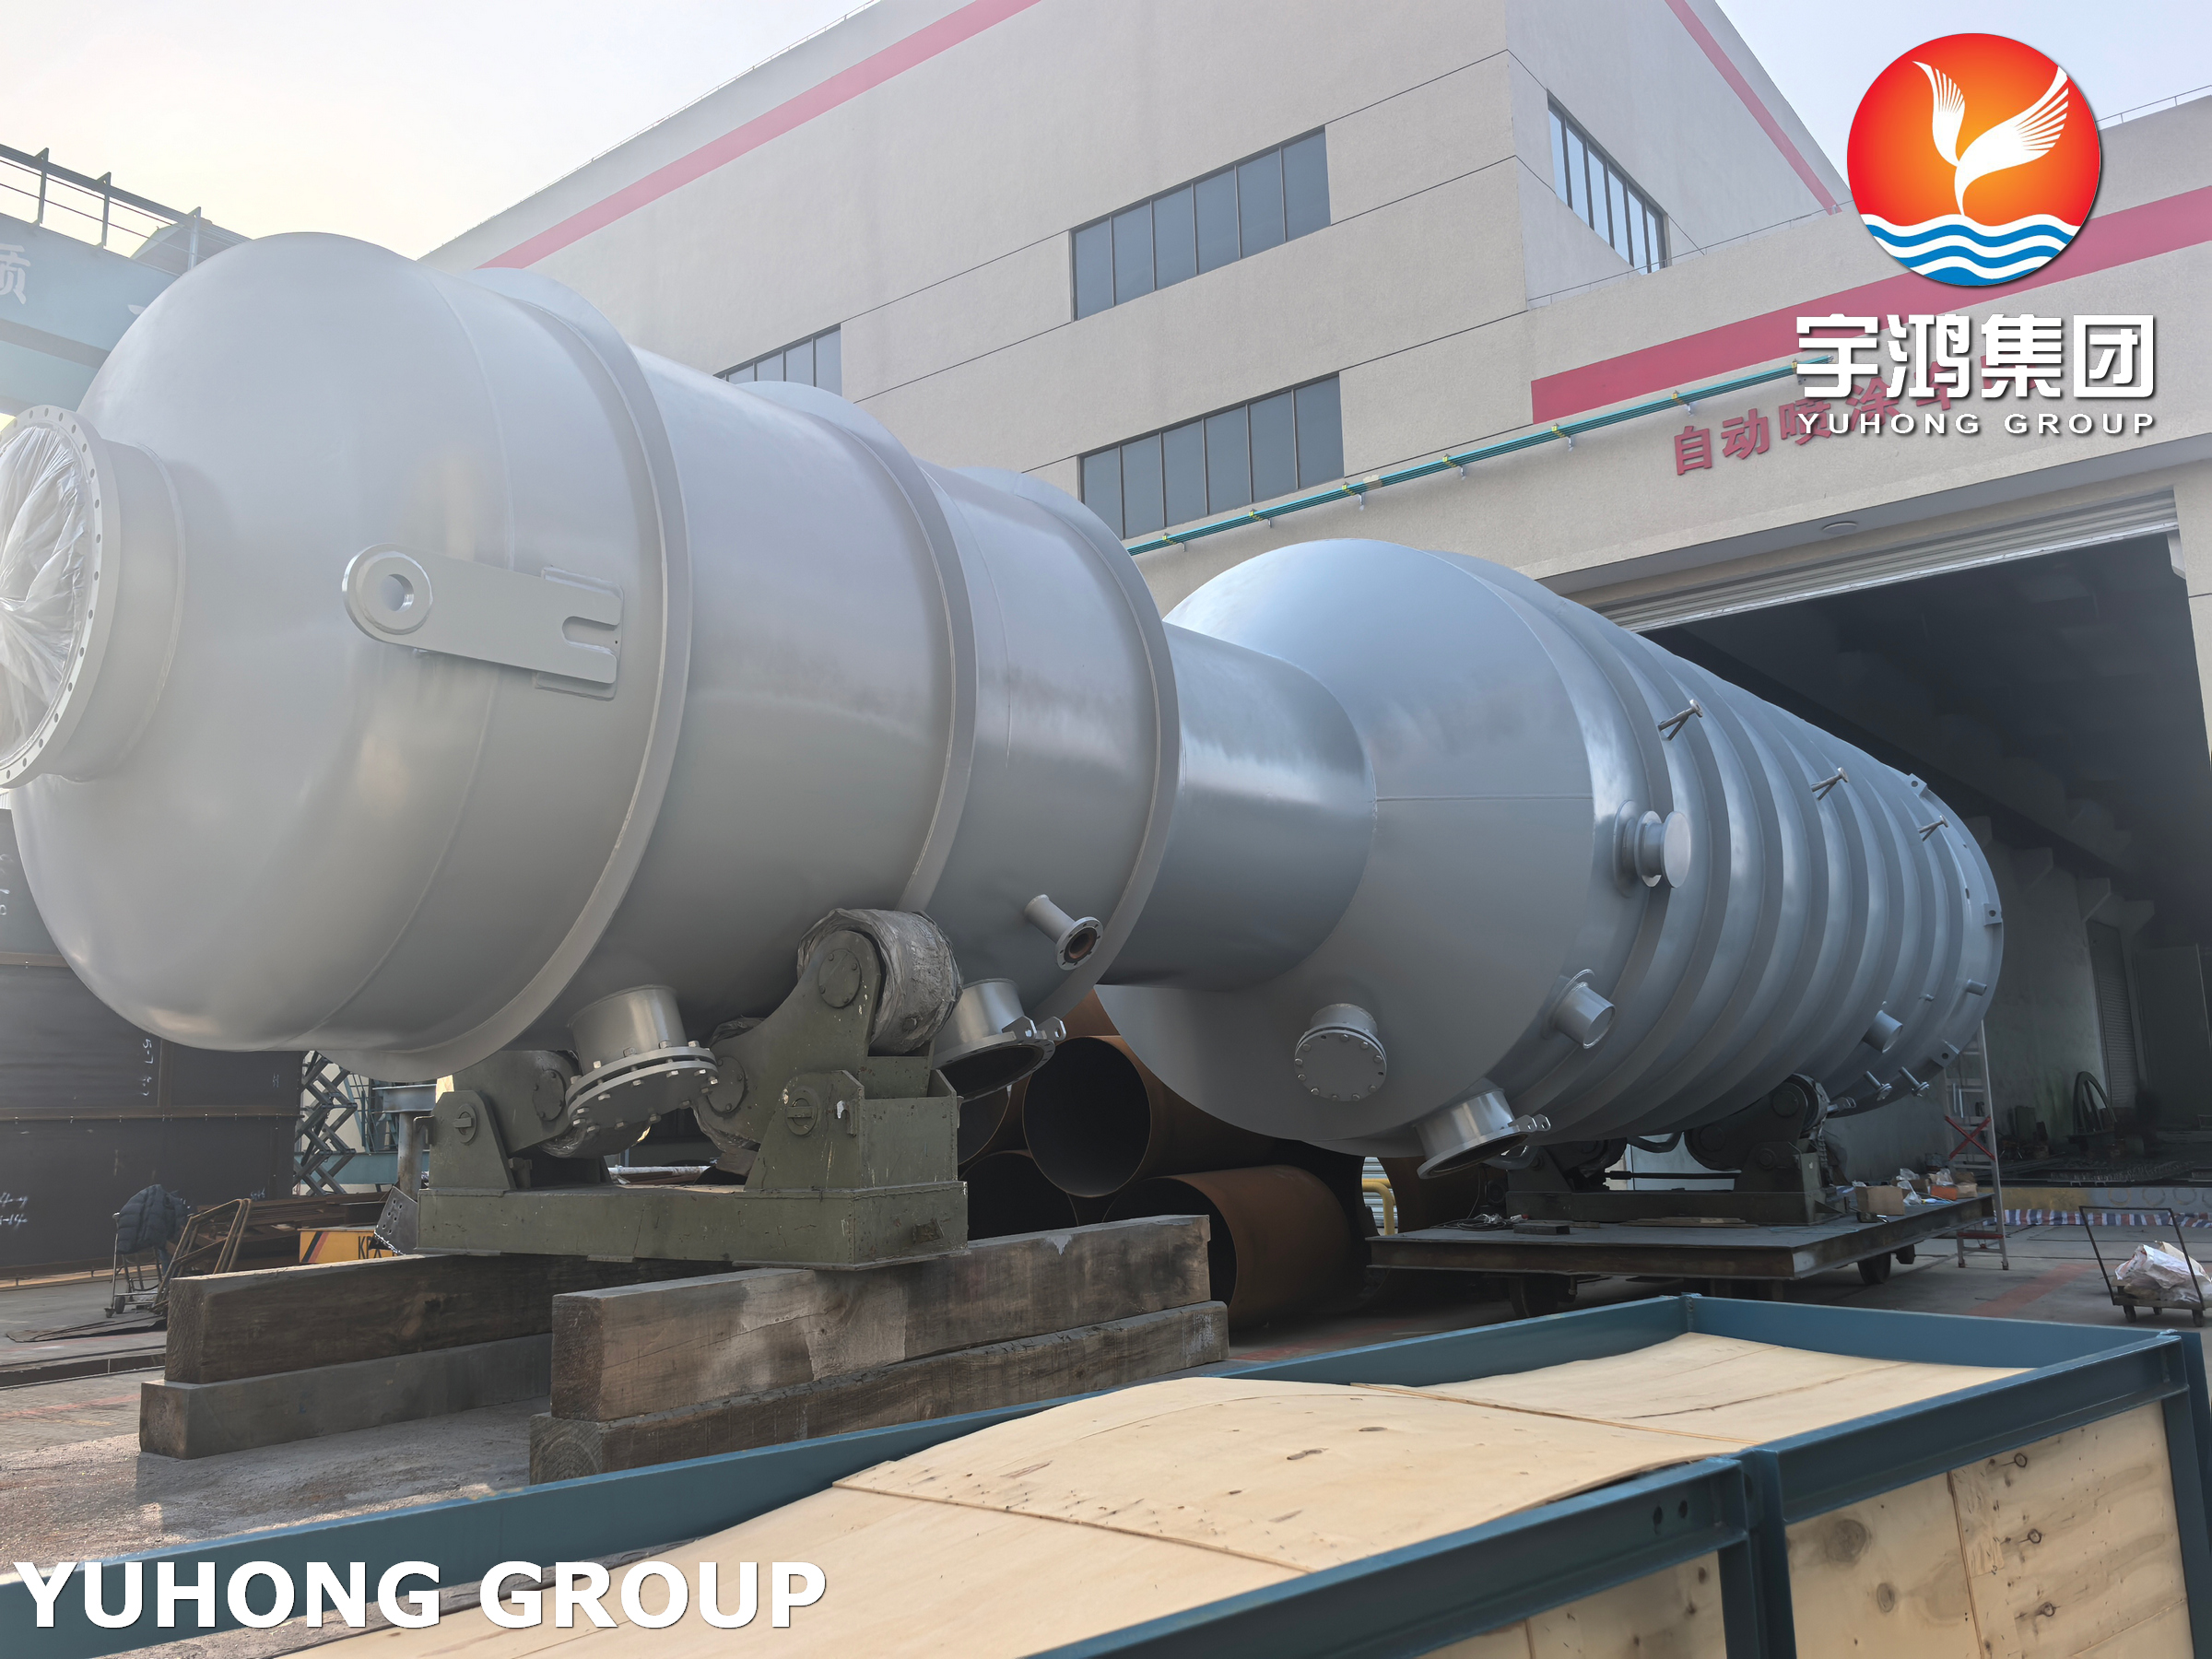
A High-Pressure Low-Temperature (HP-LT) preheater shell and tube heat exchanger engineered for binary geothermal power plant operations. Built as an ASME Section VIII Division 1 stamped TEMA heat exchanger, the unit handles n-Butane C.G. on the shell side and geothermal brine on the tube side. Heat exchange occurs via a straight tube matrix, with each individual shell offering 2,605m² of active thermal surface area.
Note: High-density finned tube bundle options can be adapted for specialized gas-phase applications requiring enhanced external surface area per project criteria.
Core Components & Material Specifications
| Component Part |
Material Grade / Standard Specification |
ASME / ASTM Code |
| Pressure Shell & Cover |
SA-516 Grade 70 Carbon Steel Plate |
ASME SA-516 Grade 70 |
| Channel / Head |
SA-516 Grade 70 + SS 316L Cladding (3 mm min. thickness) |
ASME SA-516 / SA-240 |
| Heat Transfer Tubes |
UNS S31803 / 2205 Duplex Stainless Steel (19.05 mm OD x 0.889 mm AW) |
ASME Sec. II Part A |
| Stationary Tubesheet |
SA-266 Class 2N Forging with SS 316L Weld Overlay (10 mm min. thickness) |
ASME SA-266 Class 2N |
| Baffles & Supports |
Carbon Steel (NTIW-Seg Baffle Type, Cut 16.21, Spacing 1060 mm) |
ASME Sec. II / TEMA Class C |
| Bolting (Studs / Nuts) |
SA-193 Grade B8M Studs / SA-194 Grade 8M Nuts |
ASME SA-193 / SA-194 |
| Gaskets |
Kamprofile 316L with Graphite Facing |
ASME B16.20 |
| Nozzles & Connections |
SA-106 Grade B / Flanged per ASME B16.5 & ASME B16.47 Series B |
ASME B16.5 / B16.47 |
Core Technical & Fabrication Features
- ASME Code Stamped Structural Design: Designed, fabricated, and stamped in full compliance with ASME Boiler and Pressure Vessel Code Section VIII, Division 1 and TEMA Class C standards.
- Optimized Tube Layout Pattern: Contains 19.05 mm OD tubes arranged in a 30° triangular pitch pattern 25.4mm pitch to achieve uniform fluid velocity and thermal efficiency.
- Corrosion-Resistant Weld Overlay & Cladding: Features 10 mm minimum SS 316L weld overlay on the SA-266 Class 2N tubesheet and 3 mm minimum SS 316L explosion/weld cladding across internal channel surfaces.
- Tube-to-Tubesheet Joints: Tubes are expanded and strength-welded to the tubesheet, accompanied by a helium leak test and hydrostatic validation.
- Dual-Shell Stacked Configuration: Structural saddle layout and nozzle orientations support both standalone horizontal mounting and two-shell stacked arrangements (PH1001A bottom, PH1001B top).
Quality Assurance & Testing Specifications
- Radiographic Testing (RT): 100% full radiographic examination (RT-1) on all longitudinal and circumferential pressure-retaining butt welds.
- Non-Destructive Examination (NDE): Ultrasonic Testing (UT), Liquid Penetrant Testing (PT), and Magnetic Particle Testing (MT) performed per code and contractual specifications.
- Hydrostatic Pressure Testing: Factory shop hydrostatic test calculated by the vendor to the maximum value required between ASME Code and project specification rules.
- Tube Joint Verification: Strength-welded tube-to-tubesheet connections subjected to helium leak testing prior to final hydrostatic pressure testing.
- Material Traceability: All pressure-retaining parts, internal components, and welded attachments supplied with EN 10204 Type 3.1 material test certificates.
Engineering Support & Global Project Services:
For custom ASME design verification, HTRI thermal calculations, or urgent RFQ processing, our lead sales engineer Max Zhang (Yuhong Group) provides direct technical assistance.
-
Direct Line / WhatsApp: +86-153-8196-4640
-
Engineering Mail: max [at] steelseamlesspipe [dot] com
-
Official Spec Portal: www [dot] tema-heatexchanger [dot] com