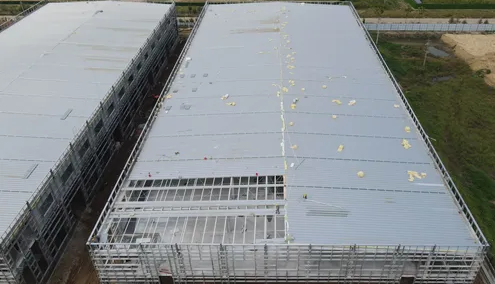
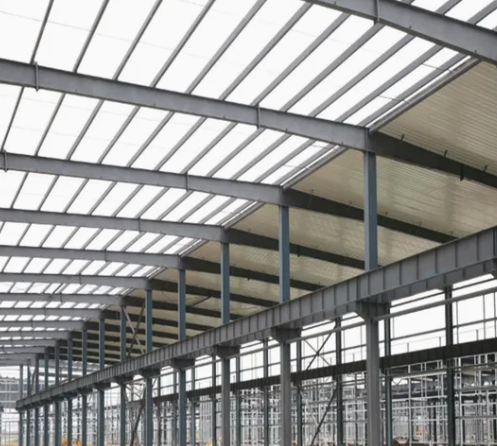
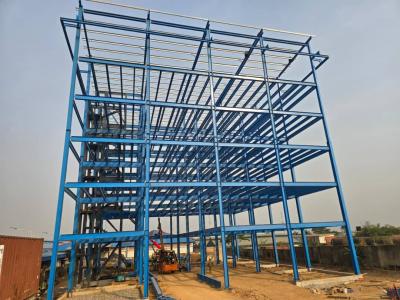
Professional Modular Design Fast Installation Seismic Resistance Prefab/Prefabricated Metal Frame/Steel Structure Warehouse/Workshop Building
Basic Information
| Model NO. |
KXD-SSB54 |
| Color Reference |
Ral |
| Member of Engineering Team |
20 |
| Quality Control |
Daily |
| Life Cycle |
50 Years |
| Construction Period |
60 Days |
| Customer Service |
Aftersale Service |
| Porject Management |
Turnkey Solution |
| Engineering Tools |
Autocad |
| Type |
H-Section Steel |
| Standard |
GB |
| Forming |
Hot-Rolled Steel |
| Carbon Structural Steel |
Q235 |
| Residential Wall Structure |
Wall Support |
| Warranty |
30 Year Limited Warranty |
| Transport Package |
Seaworthy Package |
| Specification |
SGS / ISO/ BV |
| Trademark |
KXD, Low-alloy High-tensile Structural Steel |
| Origin |
China |
| HS Code |
9406900090 |
| Production Capacity |
5000ton/Month |
Pre-engineered Structural Steel Industrial Real Estate Building Construction
What is Pre-engineered Steel Building?
Pre-engineered steel buildings are steel structures built over a structural concept of primary members, secondary members, roof and wall sheeting connected to each other and various other building components.
These buildings can be provided with different structural and non-structural additions such as skylights, wall lights, turbo vents, ridge ventilators, louvers, roof monitors, doors & windows, trusses, mezzanine floors, fascias, canopies, crane systems, insulation etc., based on customer requirements. All steel buildings are custom designed to be lighter in weight and high in strength.
Model of Pre-engineered Steel Buildings
Applications of Pre-engineered Steel Buildings
Pre-Engineered Buildings are the most flexible solutions for contractors and owners. With advantages of low cost, high durability, perfect quality control and fast erection; PEBs are used for various applications:
Industrial: Factories, Workshop, Warehouses, Cold Storages, Steel Mills, Assembly Plant
Commercial: Showrooms, Supermarkets, Offices, Shopping Centers, Exhibition Halls, Restaurants, Logistic Centers, Multi-purpose Buildings
Public: Schools, Hospitals, Conference Halls, Laboratories, Museums, Stadiums
Others: Farms, Utility Shelters, Pump Stations, Aircraft Hangars, Airport Terminals
Why Choose Pre-engineered Steel Buildings?
1. Cost Savings
Price per square meter can be 25%-30% lower than conventional steel buildings. Site erection cost is low because of faster erection times and easier erection process.
2. Quick Erection
All steel components are fabricated at the factory and linked by bolts at the site. So the erection process is fast, step by step, easy to install and requires simple equipment. 60% less construction time required compared with traditional R.C.C building.
3. Flexibility
Pre-engineered steel buildings are flexible in any requirement of design, easy to expand in the future and also economically with low transportation costs.
4. Energy Efficiency
Nowadays, pre-engineered buildings are the green solution for the environment with CO2 reduction, energy efficiency, and recyclability.
Components of Pre-engineered Steel Building
Pre-engineered metal buildings consist of following components:
- Primary Members / Main Frames
- Secondary Members / Cold Formed Members
- Roof & Wall Panels
- Accessories, Buyouts, Crane System, Mezzanine System, Insulation, etc.
- Sandwich Panels
Primary Members / Main Frames
Primary members are the main load carrying and support members of a pre-engineered building. The main frame members include columns, rafters and other supporting members. The shape and size of these members vary based on the application and requirements.
Secondary Members / Cold Formed Members
Secondary structural framing refers to purlins, girts, eave struts, wind bracing, flange bracing, base angles, clips and other miscellaneous structural parts.
Purlins, girts and eave struts are cold formed steel members which have a minimum yield strength of 345 MPa (50,000 psi) and will conform to the physical specifications of GB/ISO/CE or equivalent.
Roof & Wall Sheets/Panels
Standard steel panels are 0.3, 0.4, 0.5 mm or 0.6 mm thick and have a minimum yield strength of 345 MPa. Steel panels are hot dipped and galvanized with zinc or zinc-aluminium coating. The base material is pretreated, before applying a corrosion resistant primer and top coat. The combined thickness of the painted film is 25 microns on the front side and 12 microns on the reverse side.
Other Building Accessories
Other building accessories include anchor bolts, fasteners (bolts, nuts, turnbuckle, expansion bolts), gutters, downspouts, doors, windows, ventilators, skylight panels, louvers and all other building-related materials.
Manufacturing Process and Method Statement
The purpose of method statement is to describe the guidelines and methodology followed by our company during the fabrication, blasting, painting and supply of pre-engineered structure for any steel building project.
A: Material Receiving Procedure
- Verify the receiving documents and quantity of the received material by stores
- Submit the load for QC inspection by stores
- QC performs visual inspection to confirm surface condition and check for damages
- QC performs dimensional inspection if material passes visual inspection
- Verify supporting documents like MTC to ensure heat number matching
- QC prepares Incoming Material Inspection Report
B: Preparation of Material
Preparation of Plates:
- Design department creates structural drawings
- Drawings transferred to plate processing machine
- Automated machine processes plates according to NC files
- Punching of part mark on plates
- Drilling of plates as per NC files
- Plasma cutting of plates
Preparation of Beams/Tubes:
- Fabrication drawings prepared by design department
- Automated cutting and drilling machine processes components
- Components transferred to fit-up section after processing
C: Fit-up
- Fabrication drawings issued by production engineer
- Fabricators collect prepared beams and connection details
- End plates, gusset plates, stiffeners, purlin cleats fixed by tack welding
- Production department offers completed fit-up to QC for inspection
D: Welding & Grinding
Procedure - Submerged Arc Welding:
- Production supervisor plans welding jobs
- Only QC-accepted items taken for welding
- Clean welding locations free of dust, oil, grease
- Set wire feed and voltage for welding
- Maintain fillet size parameters per GB50661-2011 standard
- Remove spatters and slag after welding
- Grind off burrs, sharp edges and excessive reinforcements
- Offer to QC for inspection
Procedure - MIG Welding:
- Production supervisor plans welding jobs
- Only QC-accepted items taken for welding
- Clean welding locations free of dust, oil, grease
- Set wire feed and voltage for welding
- Maintain fillet size parameters per GB50661-2011 standard
- Remove spatters and slag after welding
- Grind off burrs, sharp edges and excessive reinforcements
- Offer to QC for inspection
E: Blasting
- Tool Box Talk performed by Foreman before work commencement
- Working area barricaded with information notices
- ID of fabricated steel recorded for traceability
- Raw material cleaned with high pressure air
- Material fed into automated blasting chamber
- Six internally mounted wheels throw steel shot at high velocity
- Material emerges fully cleaned (Grade - SA 2/2.5)
- Personnel wear full PPE including ear protection
F: Painting of Fabricated Material
- QC inspects blasted surfaces before primer application
- Ambient conditions checked and recorded before application
- Surface must be at least 3˚C above dew point temperature
- Relative humidity must be 85% or below
- Surface must be dry and free from oil, grease and soluble salts
- Paint applied by Airless spray where possible
- Paint material checked for conformity with shelf life restrictions
- WFT (Wet Film Thickness) readings taken during application
Specification of Painting System:
- Primer coat: Per project requirement
- Second coat: Per project requirement
- Third coat: Per project requirement
- Touchup at site - after erection
G: Loading and Shipping
- Receive finished components from painting department
- Store components properly job-wise in yard
- Arrange trucks from contract signed truck companies
- Start loading after all details confirmed
- Keep copies of all documents in Job file
Quality Standard & Control
With 20 year warranty in the steel building industry, our company maintains high quality standards. We have acquired ISO9001 and CE certificates. We strictly follow these standards for design and fabrication:
- GB/T1591-2008/2018
- GB/T11263-2010
- GB/T 2518-2008
- GB/T12754-2006
- GB/T 1228-2006
Fillet Weld Size Quality Control
1. Purpose
To ensure the quality of fillet weld, meeting technical requirements of welded members and improve standardization of our fabrication.
2. Application Scope
This manual applies for design, fabrication and inspection of fillet weld size.
3. Fillet Weld Leg Size Requirements
Minimum fillet weld size: K≥1.5×t (t = thickness of thicker welding member)
Maximum fillet weld size: K≤1.2t (t = thickness of thinner welding members)
When thickness t≤4mm, minimum fillet weld size should be same with member thickness
Selection of Fillet Weld Size
| Form of Fillet Weld Leg |
K (Fillet Weld Size) Value |
Note |
| Fillet weld without groove |
K=(0.7~1)t and ≤15mm |
For most steel structure buildings |
| Fillet weld without groove |
K=(0.5~0.6)t |
For strengthening ribs and secondary members |
| Fillet weld with groove (CJP and PJP) |
K=t/4 and K≤10mm |
For most steel structure buildings |
| Fillet weld with groove (CJP and PJP) |
K=t/2 and K≤10mm |
Important members (crane beams) |
Minimum Fillet Weld Size Chart
| Parent Metal Thickness (t) (mm) |
Minimum Fillet Weld Size |
| t≤6 |
3 (minimum value being 5 for crane beam) |
| 6 |
5 |
| 12 |
6 |
| t>20 |
8 |
KXD's H Section Manufacturing Equipment and Process
Steel plate cutting → H section assembly → Automatic welding → H section strengthening → Assembly → Manual welding → Shot blasting → Painting → Storage
Manufacturing Equipment
Portable CNC Fire-cutting machine
Model No.: CNCDG-1530
Application: Steel plate cutting (5-100mm thickness), beveling of edge. Advantageous in small equipment and easy-to-move.
Straight flame cutting machine
Model No.: DZCG-4000A
Application: Steel plate cutting (5-100mm thickness), Y flange plate, web plate cutting, effective cutting width: 3200mm
CNC cutting machine
Model No.: CNC-4000C
Application: Steel plate cutting (5-100mm thickness), Y flange plate, web plate and irregular component cutting, effective cutting width: 3200mm
Radial drilling machine
Model No.: Z3050*16/1
Application: Maximum drilling diameter φ50mm, mainly for processing of component bolt-connection holes
Puncher machine
Model No.: JH21-400
Application: Maximum stamping pressure-400 ton, mainly for plate punching, blanking, bending and shallow stretching
Shearing machine
Model No.: Q11Y-25*2500
Application: Cutting width 2500mm and cutting thickness 3-25mm
H section steel assembly machine
Model No.: Z20B
Application: Mainly for H type assembly, flange width 150-800mm, web height 160-2000 mm
Gantry-type submerged arc automatic welding machine
Model No.: LHA5ZB
Application: Mainly for assembly welding of H section steel with maximum cross section up to 800mm×2000mm
H section steel strengthening machine
Model No.: YTJ60B
Application: Correcting deformation of I beam or H section steel flange plate during welding process
H section flange strengthening machine
Model No.: HYJ-800
Application: Correcting deformation of I beam or H section steel flange plate during welding process
10-ramming heads shot blasting machine
Model No.: QH1525
Application: Shot blasting of section steels including H section steel, welded members and steel plate
Airless sprayer
Model No.: CPQ9CA
Application: Surface paint of structural members, Pressure ratio: 32:1