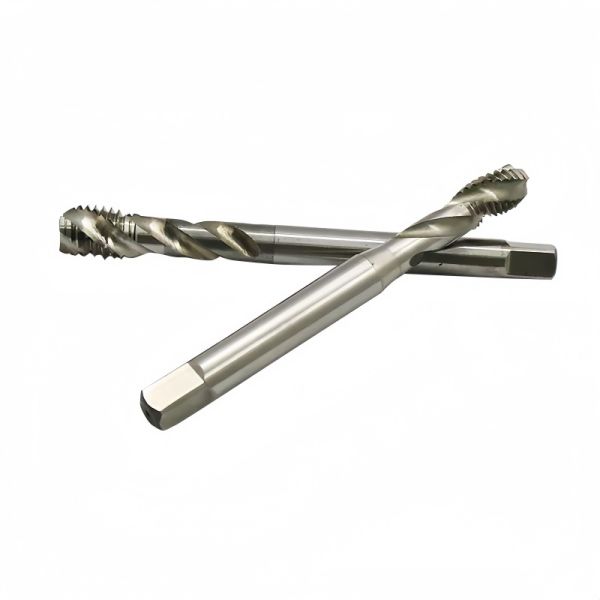
The DIN 371/376 HSS-E M35 Spiral Flute Machine Taps are the definitive solution for high-speed, automated blind hole tapping. Featuring a precision-engineered 35° helix angle, these taps lift chips upward and out of the hole, preventing the catastrophic "chip-packing" that leads to tool breakage.
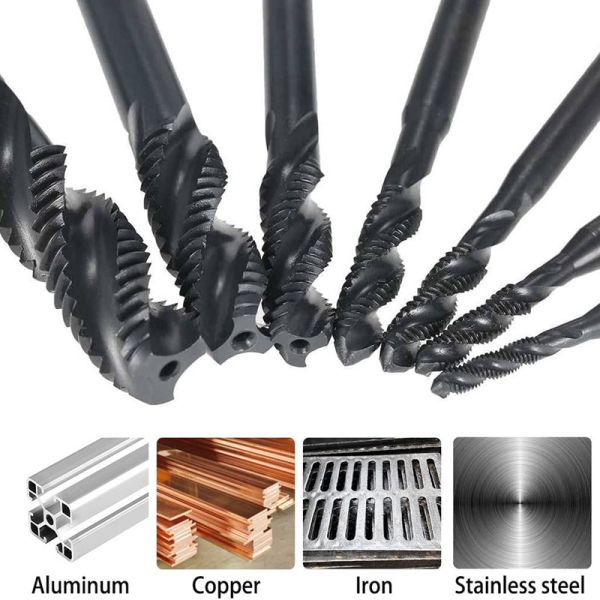
Forged from premium M35 Cobalt Steel (5% Co), this series offers the thermal stability required for machining work-hardening materials like Stainless Steel (304/316) and high-tensile alloys. Whether you are tapping delicate M2 electronics components or massive M42 industrial housings, our taps deliver consistent 6H precision.

Our production range covers the entire industrial spectrum, divided by DIN standards for optimized shank strength:
A. Large & Medium Sizes: DIN 376 (Reduced Shank)
| Size | Pitch (P) | Total Length (L1) | Thread Length (L2) | Shank Ø (D2) | Square (K) |
| M42 | 4.50 | 200 mm | 45 mm | 32.0 mm | 24.0 mm |
| M36 | 4.00 | 200 mm | 40 mm | 28.0 mm | 22.0 mm |
| M30 | 3.50 | 180 mm | 35 mm | 22.0 mm | 18.0 mm |
| M27 | 3.00 | 160 mm | 30 mm | 20.0 mm | 16.0 mm |
| M24 | 3.00 | 160 mm | 30 mm | 18.0 mm | 14.5 mm |
| M20 | 2.50 | 140 mm | 25 mm | 16.0 mm | 12.0 mm |
| M16 | 2.00 | 110 mm | 20 mm | 12.0 mm | 9.0 mm |
| M14 | 2.00 | 110 mm | 20 mm | 11.0 mm | 9.0 mm |
| M12 | 1.75 | 110 mm | 18 mm | 9.0 mm | 7.0 mm |
B. Small & Precision Sizes: DIN 371 (Reinforced Shank)
| Size | Pitch (P) | Total Length (L1) | Thread Length (L2) | Shank Ø (D2) | Square (K) |
| M10 | 1.50 | 100 mm | 15 mm | 10.0 mm | 8.0 mm |
| M8 | 1.25 | 90 mm | 13 mm | 8.0 mm | 6.2 mm |
| M6 | 1.00 | 80 mm | 10 mm | 6.0 mm | 4.9 mm |
| M5 | 0.80 | 70 mm | 8 mm | 6.0 mm | 4.9 mm |
| M4 | 0.70 | 63 mm | 7 mm | 4.5 mm | 3.4 mm |
| M3 | 0.50 | 56 mm | 5 mm | 3.5 mm | 2.7 mm |
| M2.5 | 0.45 | 50 mm | 4 mm | 2.8 mm | 2.1 mm |
| M2 | 0.40 | 45 mm | 4 mm | 2.8 mm | 2.1 mm |
High-Efficiency 35° Helix: Unlike standard 25° helixes, our 35° angle provides a faster "upward lift" for chips, specifically tested for long-chip materials like Stainless Steel and Aluminum.
Vacuum Heat Treatment: Every tap is hardened in a state-of-the-art vacuum furnace to HRC 64-66. This ensures zero surface decarburization and a metallurgically stable core.
Fully Ground Construction: Threads, flutes, and shanks are CNC-ground from a single hardened blank. This results in 6H Class Tolerance and a mirror-like surface finish that reduces friction heat.
Red Hardness Advantage: The 5% Cobalt (HSSE) content allows the tool to maintain its cutting edge even when friction temperatures in the blind hole reach 600°C.
CNC Machining Centers: The go-to choice for automated VMC/HMC tapping where manual chip clearing is impossible.
Critical Component Tapping: Used in automotive engine blocks, aerospace brackets, and hydraulic manifolds where blind-hole thread integrity is non-negotiable.
Difficult Materials: Engineered for Inox (304, 316), Titanium alloys, High-nickel alloys, and Structural Steel up to 1200 N/mm².