Specifications
Hardness :
62-66 HRC
Application :
Steel Stainless Steel Nut Thread Tapping
Flute type :
Straight Flute
name :
DIN371/376 hss Forming machine taps
Coating :
Tin Coated
Brand Name :
XRTOOLS
Model Number :
No.1-64
Certification :
ISO9000
Place of Origin :
CHINA
MOQ :
100 PCS
Price :
$1.35-$45.55/PCS
Payment Terms :
L/C, T/T, Western Union
Supply Ability :
30000PCS PER DAY
Delivery Time :
25-30 days
Packaging Details :
Plastic box
Material :
HSS-M35,HSS-E
Size :
M2-M42
Process :
Fully Ground
Tolerance :
6H
Hole type :
Blind Hole
Description

1. Introduction: The Revolution of Chipless Tapping

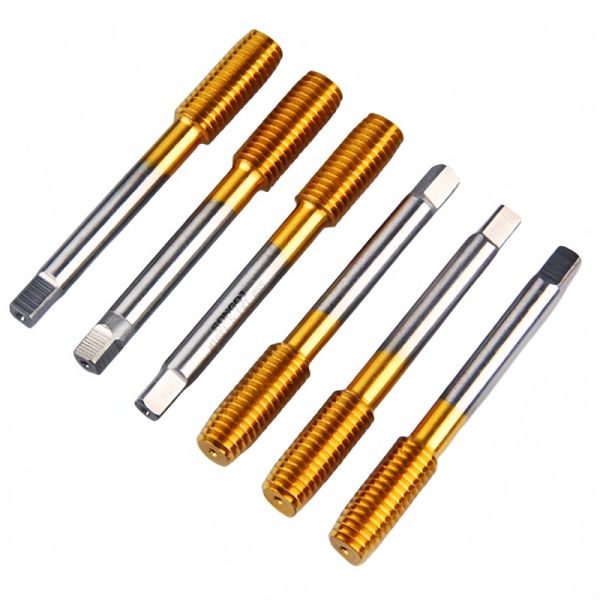
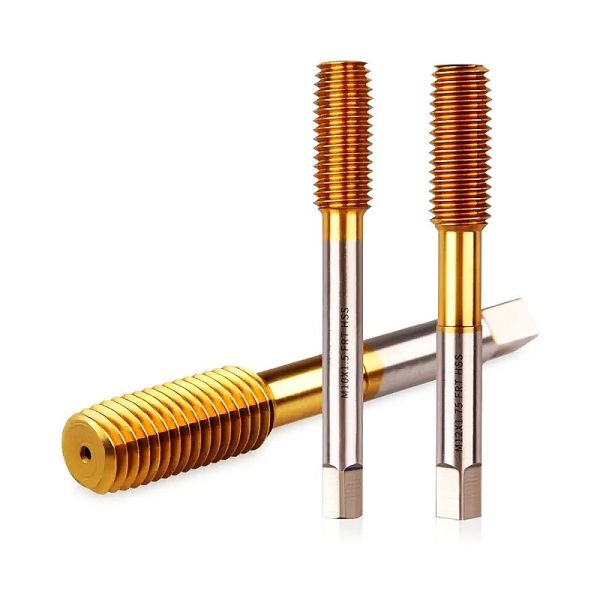
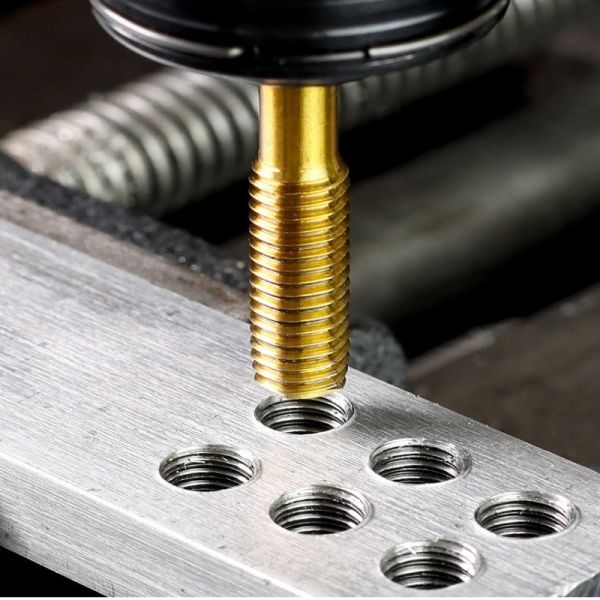
Our DIN 371/376 TiN Coated Form Taps (also known as Fluteless Taps or Cold Roll Taps) represent the most efficient threading solution for ductile materials. Unlike traditional taps, these tools do not cut the material; instead, they displace it to form the thread profile.

The result is a compressed, high-strength thread with a superior surface finish. Combined with a Titanium Nitride (TiN) coating, these taps offer an ultra-low friction coefficient, preventing material galling and allowing for incredibly high production speeds in both through and blind holes.

Industrial Gold TiN Coated HSSE Cold Form Taps | DIN 371 Reinforced Shank | High-Performance Zero-Chip Tapping

2. Technical Specifications (M2 - M20 Range)

Size Pitch (P) DIN Standard Shank Type Overall Length (L1) Thread Length (L2) Shank Ø (D2)
M2 0.40 DIN 371 Reinforced 45 mm 8 mm 2.8 mm
M3 0.50 DIN 371 Reinforced 56 mm 10 mm 3.5 mm
M4 0.70 DIN 371 Reinforced 63 mm 12 mm 4.5 mm
M5 0.80 DIN 371 Reinforced 70 mm 14 mm 6.0 mm
M6 1.00 DIN 371 Reinforced 80 mm 17 mm 6.0 mm
M8 1.25 DIN 371 Reinforced 90 mm 20 mm 8.0 mm
M10 1.50 DIN 371 Reinforced 100 mm 22 mm 10.0 mm
M12 1.75 DIN 376 Reduced 110 mm 24 mm 9.0 mm
M16 2.00 DIN 376 Reduced 110 mm 27 mm 12.0 mm
M20 2.50 DIN 376 Reduced 140 mm 32 mm 16.0 mm

3. Key Advantages of Form Tapping

  • Zero Chip Management: Since no chips are produced, there is zero risk of chip clogging in blind holes. This eliminates the #1 cause of tap breakage.

  • Superior Thread Strength: Because the metal grain flow is diverted rather than cut, the resulting threads have higher pull-out strength and resistance to stripping.

  • Exceptional Tool Life: Without sharp cutting edges to dull, and with the heat-shielding TiN coating, form taps typically last 3 to 10 times longer than cutting taps.

  • High-Speed CNC Performance: Optimized for synchronized tapping on modern VMC and HMC centers.

Industrial Gold TiN Coated HSSE Cold Form Taps | DIN 371 Reinforced Shank | High-Performance Zero-Chip Tapping

4. Strategic Applications: Best Materials

Form taps require materials with good "flow" characteristics (ductility).

  • Aluminum Alloys: Both cast and wrought aluminum (6061, 7075, etc.).

  • Low Carbon Steels: Mild steels and structural steels up to 900 N/mm².

  • Stainless Steel: High-ductility grades like 304 and 316.

  • Copper & Brass: Excellent results in non-ferrous, gummy materials.

Industrial Gold TiN Coated HSSE Cold Form Taps | DIN 371 Reinforced Shank | High-Performance Zero-Chip Tapping

5. Manufacturing Excellence & Packaging

  • HSSE-M35 Substrate: 5% Cobalt content provides the core toughness to handle the high pressure of the forming process.

  • TiN Gold Coating: Provides a surface hardness of 2300 HV, ensuring the lobes of the form tap maintain their precision for thousands of holes.

  • Rose-Box Packaging: Vacuum-sealed and protected in premium individual plastic tubes with high-viscosity anti-rust oil.

6. Professional FAQ for Buyers

Q: Is the pre-tap drill size the same as for cutting taps?

A: NO. This is critical. Because you are displacing material rather than cutting it, you need a larger hole. For example, for M6 x 1.0, a cutting tap uses a 5.0mm drill, but a form tap requires a 5.5mm drill. Using a 5.0mm drill with a form tap will break the tool immediately.

Q: Can I use form taps for any material?

A: Form taps are ideal for ductile materials. They are not suitable for materials with low ductility, such as Gray Cast Iron or hard steels (>HRC 35).

Q: Do I need special lubrication?

A: Yes. Form tapping is a high-pressure process. High-quality tapping oil or high-concentration coolant is recommended to maximize the lifespan of the TiN coating.

Send your message to this supplier
Send Now

Industrial Gold TiN Coated HSSE Cold Form Taps | DIN 371 Reinforced Shank | High-Performance Zero-Chip Tapping

Ask Latest Price
Watch Video
Hardness :
62-66 HRC
Application :
Steel Stainless Steel Nut Thread Tapping
Flute type :
Straight Flute
name :
DIN371/376 hss Forming machine taps
Coating :
Tin Coated
Brand Name :
XRTOOLS
Contact Supplier
video
Industrial Gold TiN Coated HSSE Cold Form Taps | DIN 371 Reinforced Shank | High-Performance Zero-Chip Tapping

Jiangsu Xingrui Precision Tools Co., Ltd.

Verified Supplier
6 Years
yangzhou
Since 2008
Business Type :
Manufacturer, Exporter, Trading Company
Total Annual :
500-600
Employee Number :
30~50
Certification Level :
Verified Supplier
Contact Supplier
Submit Requirement