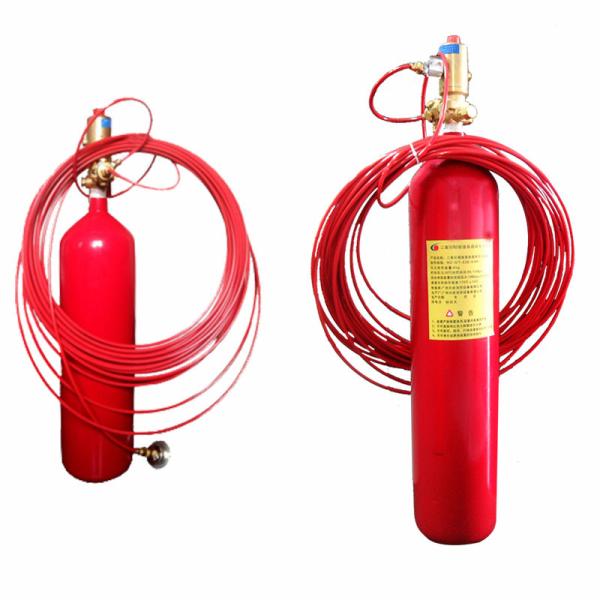
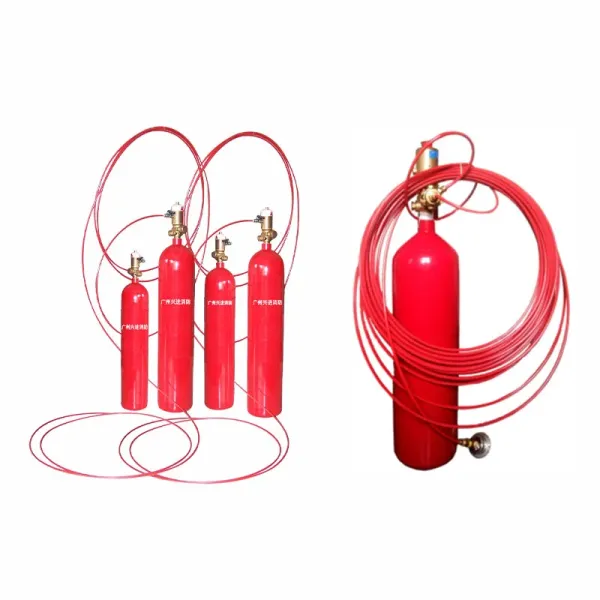
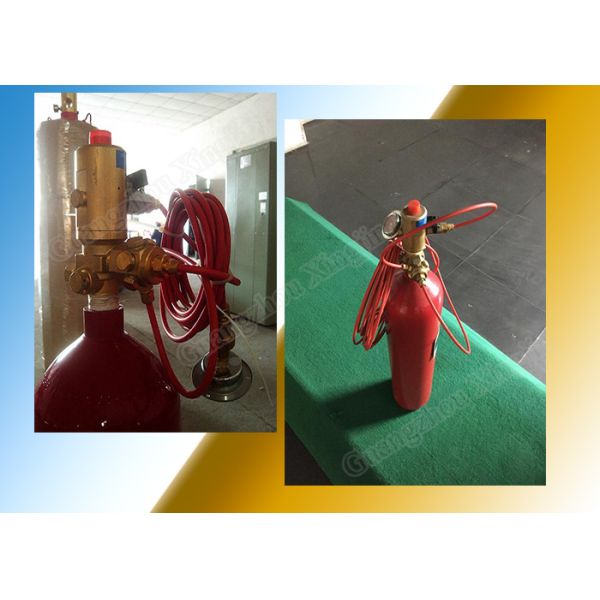
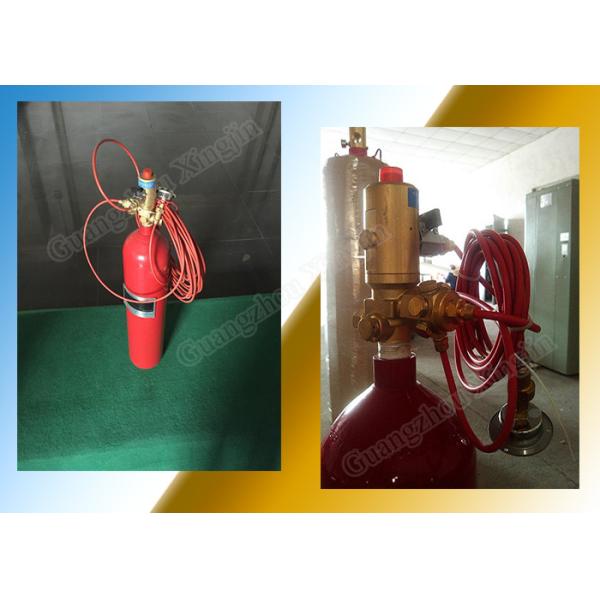
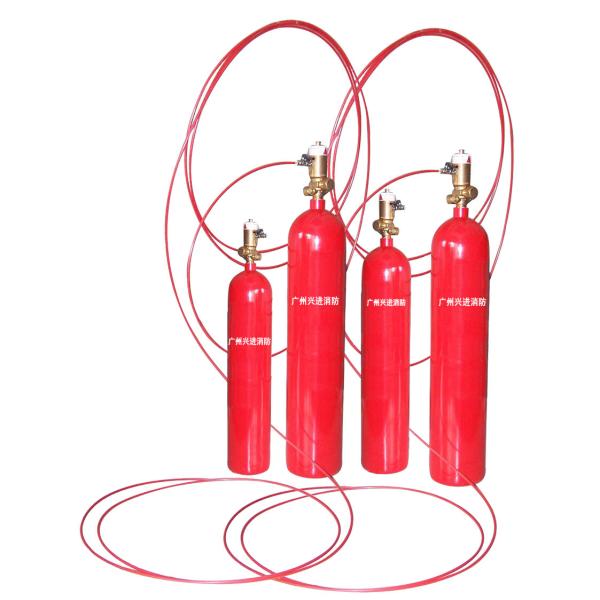
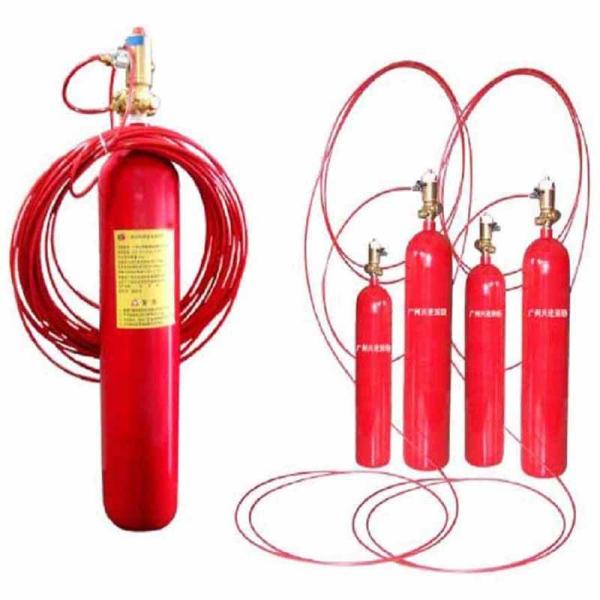
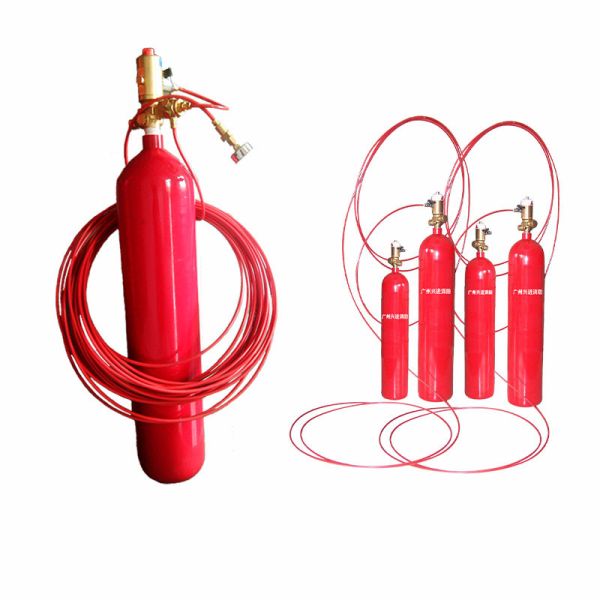
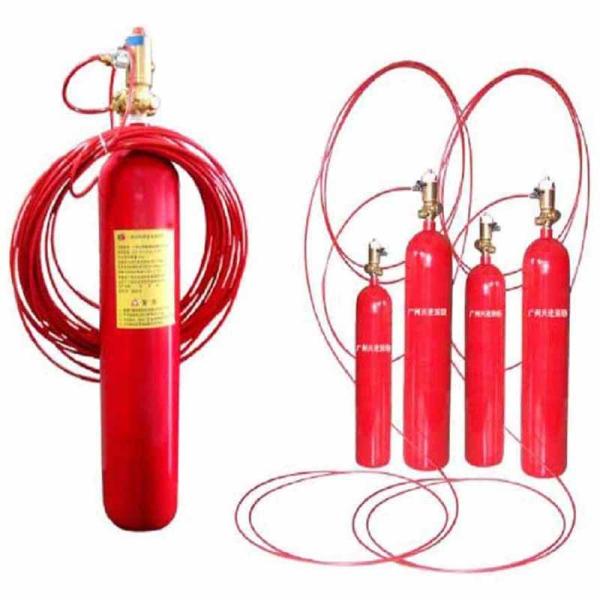
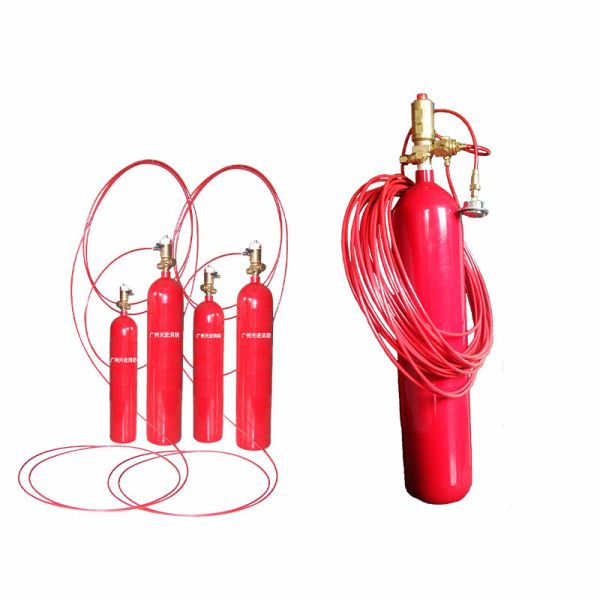
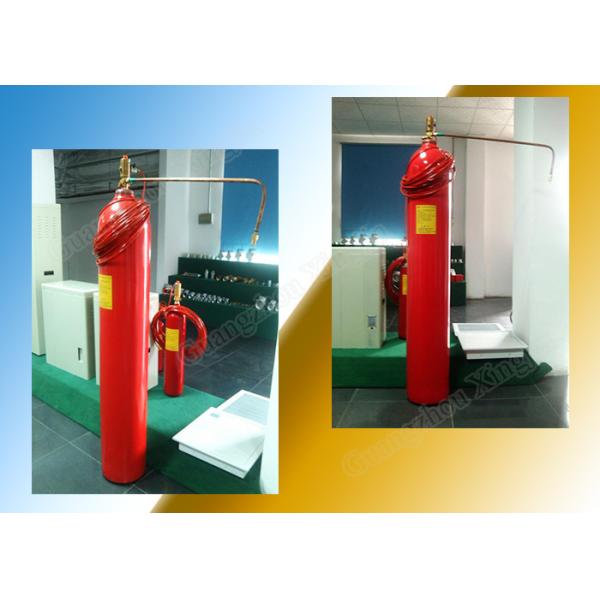
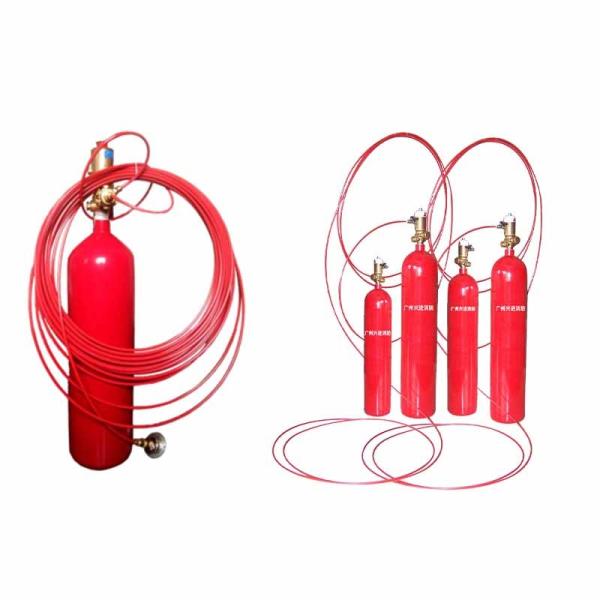
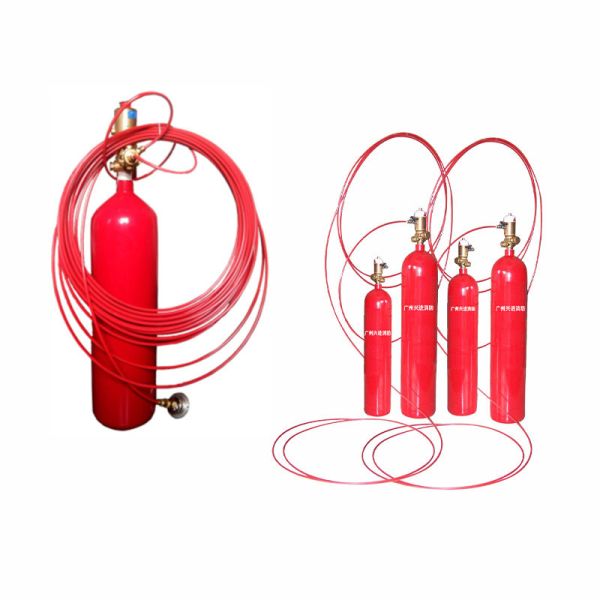
The Fire Detection Tube is an advanced safety solution engineered to deliver reliable and efficient fire detection across a wide range of environments. Housed in a sturdy aluminum alloy cylinder, the system maintains its storage pressure even at ambient temperatures of 20ºC. This robust construction guarantees durability and preserves system integrity, ensuring it is always ready to respond in the event of a fire.
A standout feature of the Fire Detection Tube is its ease of installation. Designed with the user in mind, the system can be fitted quickly and easily without specialized tools or professional expertise. This makes it an ideal choice for residential, commercial, and industrial applications where rapid deployment is essential.
The system operates effectively within a working temperature range of 0ºC to 50ºC, making it a versatile solution for different climates and conditions. Whether installed in the chill of a cold storage facility or the warmth of a server room, the Fire Detection Tube maintains full functionality and continuous protection against fire threats.
The cylinder is finished in a vivid red color—a universal signal for caution and safety. This high-visibility finish allows for easy location during an emergency, serves as a deterrent to potential wrongdoers, and enables quick identification during maintenance checks and inspections.
Effective fire suppression depends on the correct quantity of agent. The Fire Detection Tube requires a minimum of 2.5 kg of extinguishing agent per cubic meter, ensuring sufficient agent to control and extinguish fires quickly and effectively. This precise agent-to-space ratio is essential for adequate protection, minimized damage, and safe evacuation procedures.
In summary, the Fire Detection Tube is an innovative fire detection and suppression system characterized by its aluminum alloy construction for optimal storage pressure at 20ºC, ease of installation, broad working temperature range, high-visibility red cylinder, and precise agent requirements. It provides a reliable first line of defense against fires—offering peace of mind and safety for property and lives, whether for a new construction project or retrofitting an existing space.
| Parameter | Specification |
|---|---|
| Product Name | Fire Detection Tube |
| Max. Working Pressure | 4.2 MPa |
| Working Temperature | 0ºC–50ºC |
| Supply Ability | 30,000 Sets Per Week |
| Specification | FM200 Clean Agent / CO2 |
| Installation | Easy To Install |
| Minimum Order | 5 Sets |
| Actuation | Automatic |
| Min. Agent Needed Per Unit | 2.5 kg/m³ |
| Max. Length of Fire Tube | 20 m |
The Fire Detection Tube, manufactured by Guangzhou Xingjin Fire Equipment Co., Ltd. under model number WZ-Q/T-QZ3-XJ60, is a highly efficient and responsive fire protection solution designed to ensure maximum safety across a wide variety of environments. Originating from Guangzhou, Guangdong, China, this product represents cutting-edge fire safety technology, primed for immediate deployment in numerous scenarios.
One of the most compelling attributes of the Fire Detection Tube is its remarkably swift response time of ≤5 seconds, making it an essential asset in critical situations where every second counts. This rapid action can mean the difference between a minor incident and a catastrophic event, providing peace of mind for both property owners and occupants. With a maximum tube length of 20 meters, the system can cover a substantial area, ensuring no corner is left unprotected.
The robust construction of the Fire Detection Tube allows it to maintain a working pressure of CO2 at 12.1 MPa and FM200 at 4.2 MPa, demonstrating its ability to withstand extreme conditions while remaining operationally effective. This is particularly important in environments where the tube may be exposed to harsh elements or where fire risk is heightened by volatile substances. With a maximum filling rate of 1.12 kg/L, the system is filled to optimal capacity to handle fires swiftly and efficiently.
Application occasions are vast and varied. The system is ideally suited for industrial settings such as manufacturing plants, warehouses, and chemical processing facilities, where fire risk is heightened by the presence of flammable materials. It can also be utilized in commercial kitchens, server rooms, data centers, and electrical cabinets, where rapid detection and suppression are critical to preventing data loss, equipment damage, and significant downtime.
Scenarios that particularly benefit from installation include high-risk areas with limited accessibility or those left unattended for extended periods. The system’s autonomous nature means it can activate and suppress fires without human intervention—crucial in remote locations or off-hours operations such as unmanned warehouses or transport containers in transit. In the event of a fire, the tube’s pre-engineered design delivers a quick and direct suppression method, minimizing damage and potentially saving lives.
Thank you for choosing our Fire Detection Tube for your safety needs. Our product is designed with the latest technology to provide reliable fire detection in a variety of settings. To ensure optimal performance and longevity, we offer a comprehensive suite of technical support and services.
Our goal is to ensure you are fully satisfied with your Fire Detection Tube and the support we provide. We are dedicated to offering top-tier services to assist you in protecting your premises against the threat of fire.
The Fire Detection Tube is meticulously packaged in a durable, heat-resistant material designed to ensure the integrity of the product during transit. Each tube is encased in a protective sleeve, accompanied by silica gel packets to absorb any moisture. The product is then placed in a sturdy cardboard box with custom-fit foam inserts that provide additional cushioning and stability. The exterior of the box is clearly marked with the appropriate hazard and handling symbols to alert carriers to the sensitive nature of the contents.
All orders of the Fire Detection Tube are dispatched via our trusted logistics partners, who specialize in the handling and transportation of fire safety equipment. Our shipping process includes real-time tracking and requires a signature upon delivery to guarantee the secure and prompt arrival of your product. We advise customers to inspect the package for any signs of damage before accepting delivery. In the rare event of transit damage, please report it immediately to our customer service team for prompt resolution.
A1: The brand name of the Fire Detection Tube is Guangzhou Xingjin Fire Equipment Co., Ltd.
A2: Yes, the model number for the Fire Detection Tube is WZ-Q/T-QZ3-XJ60.
A3: The Fire Detection Tube is manufactured in Guangzhou, Guangdong, China.
A4: The Fire Detection Tube detects the presence of heat and flames in an environment and triggers an alarm or a fire suppression system. It is designed to respond rapidly to a fire, helping to minimize damage and ensure safety.
A5: The Fire Detection Tube is versatile and can be used in a variety of settings, including industrial, commercial, and residential environments. It is especially useful in areas where traditional smoke detectors may not be practical or where quick detection is critical.