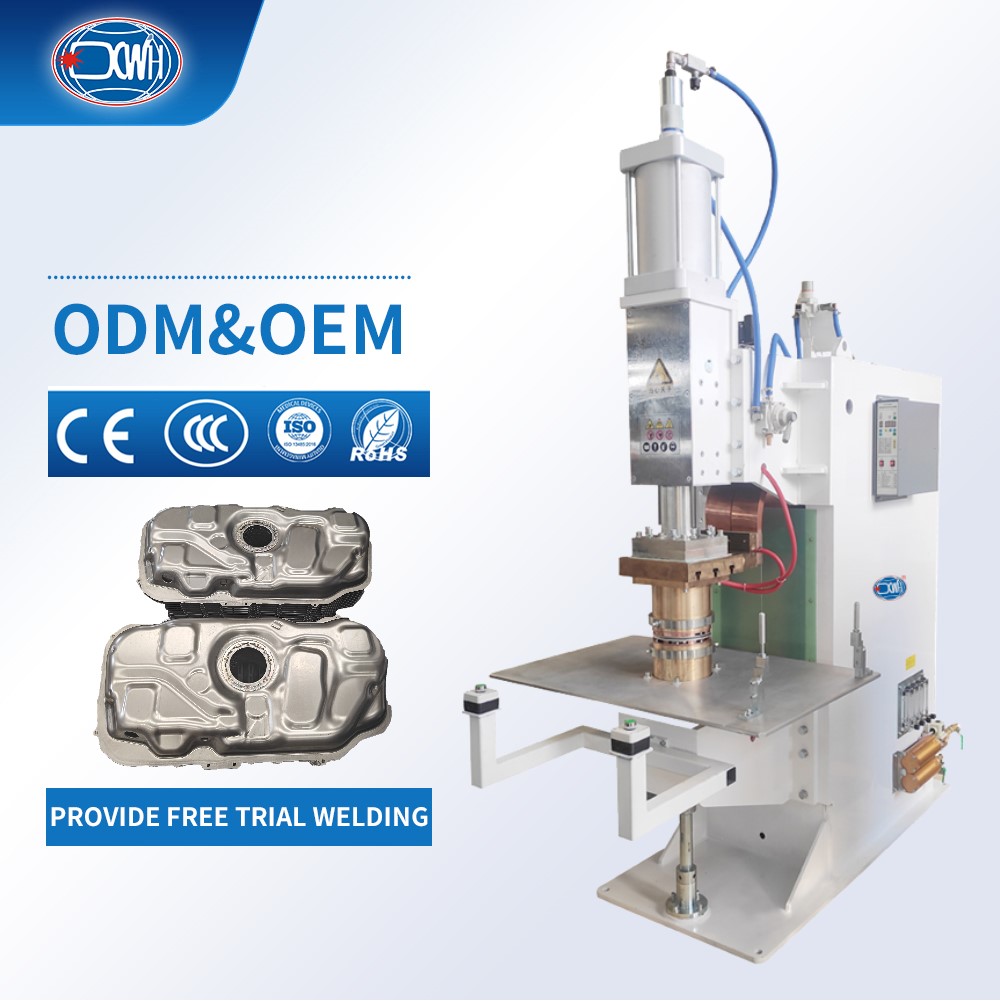
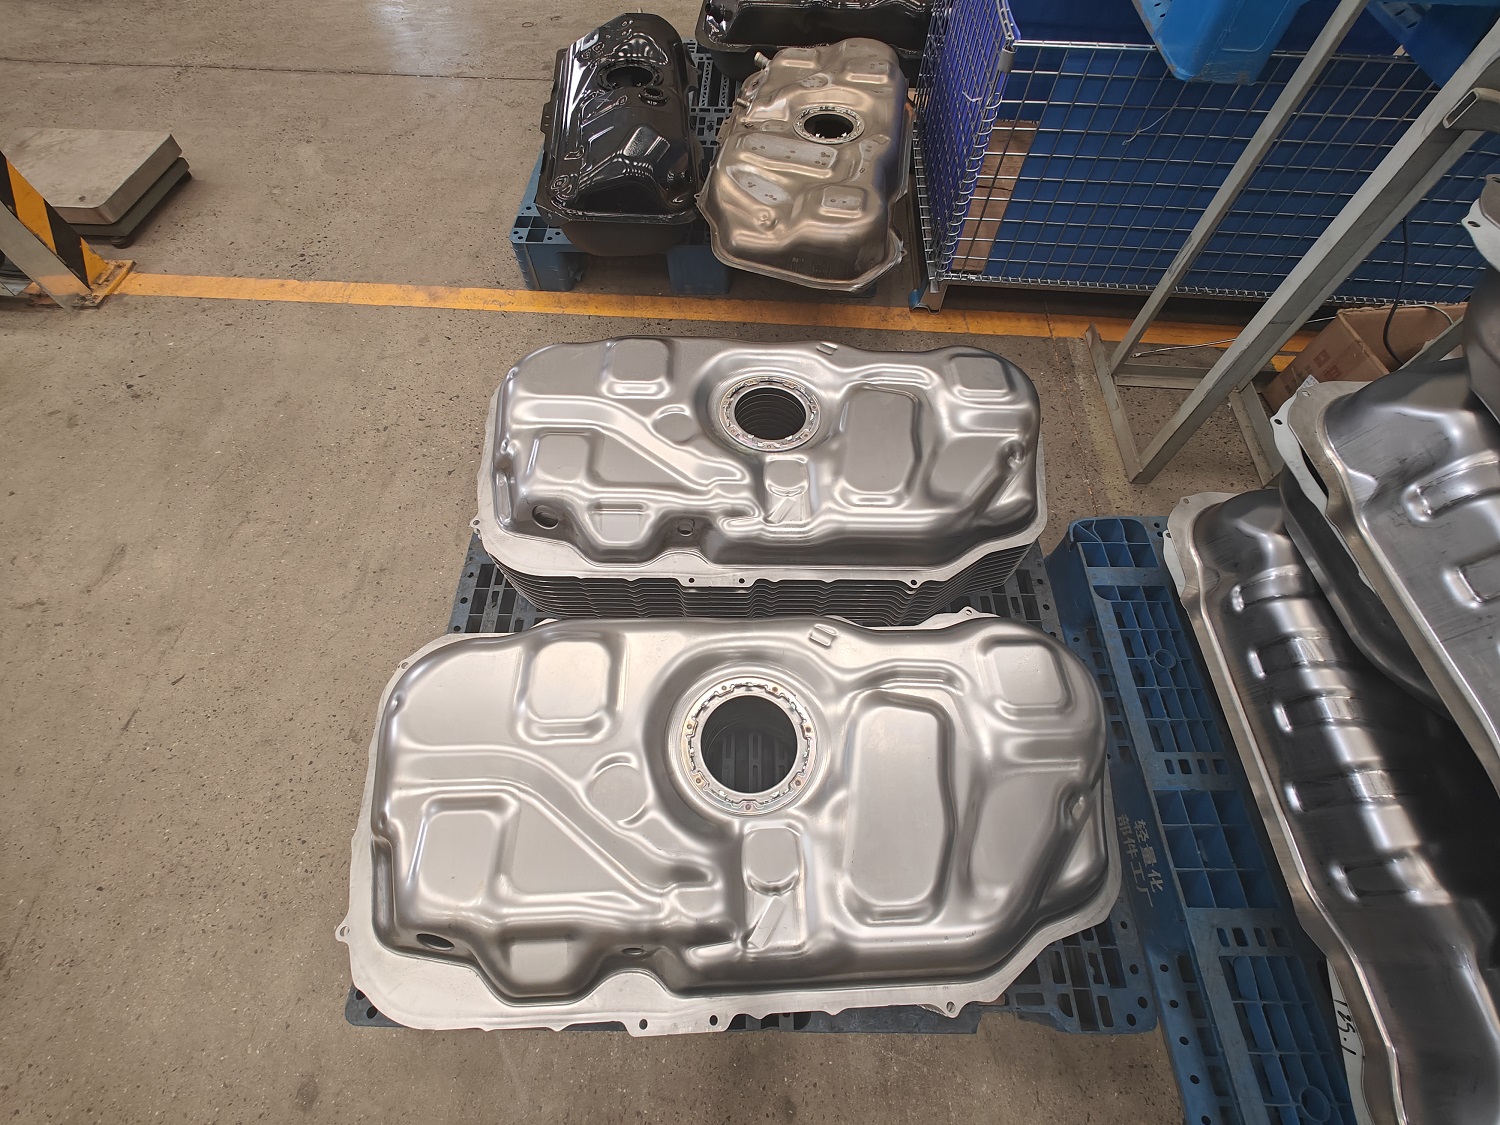
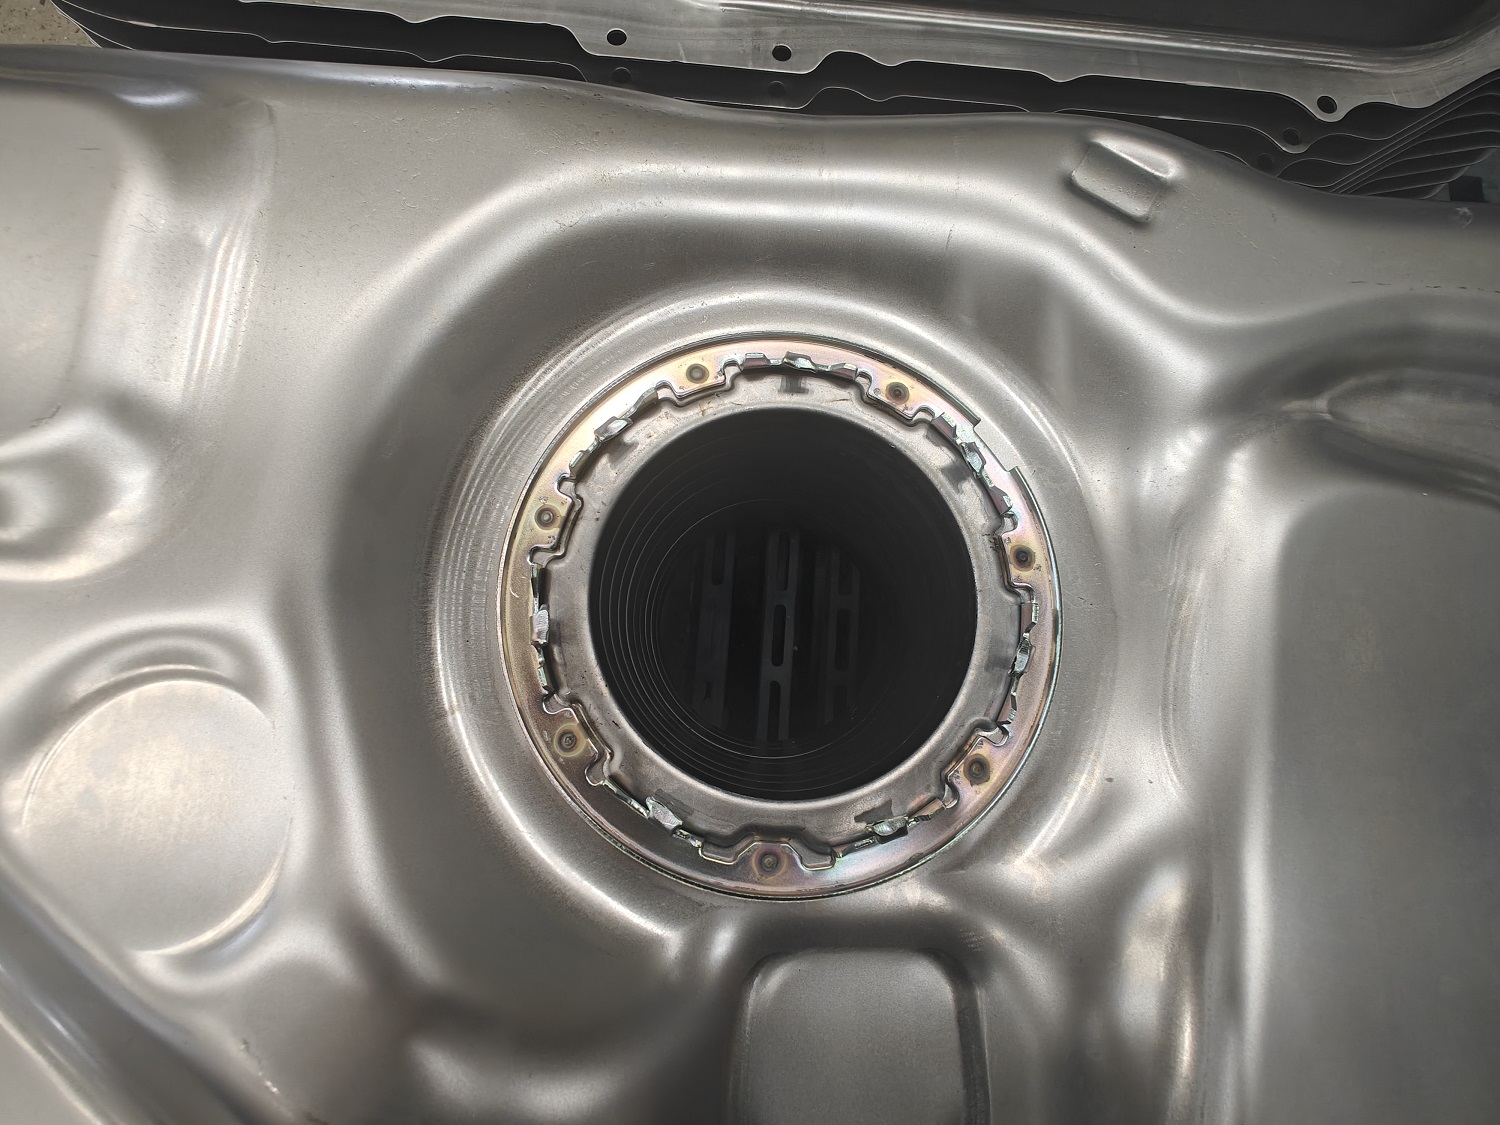
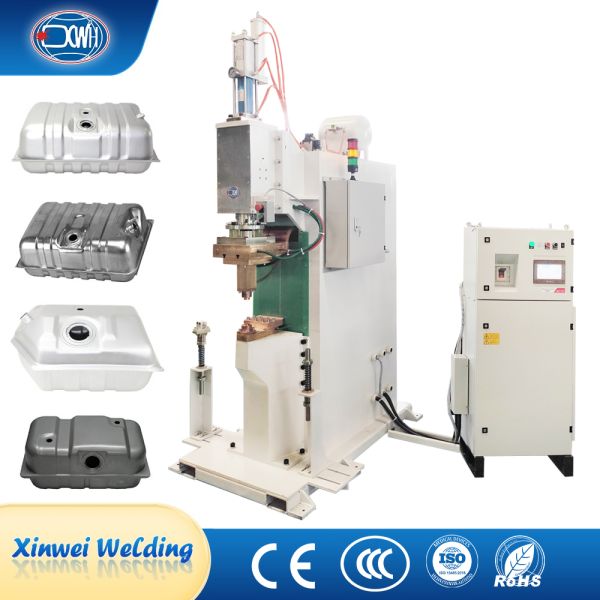
Engineered for high-volume fuel tank production, this DN100 pneumatic resistance spot and projection welding machine streamlines the joining of tank shells with metal rings. The unit replaces the conventional single-electrode approach with a full annular electrode ring assembly, enabling seven welds to be completed simultaneously in a single press cycle. This semi-automatic system is well suited for manufacturers producing fuel tanks across multiple diameters and wall thicknesses, delivering consistent joint quality while reducing cycle time per workpiece.
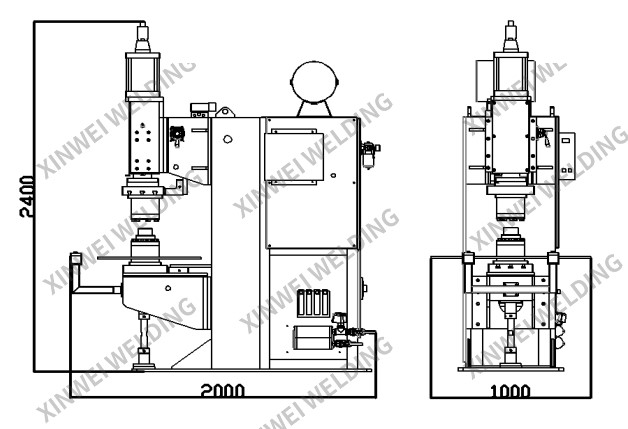
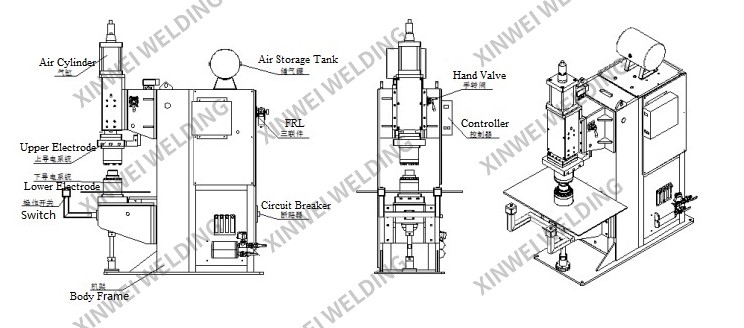
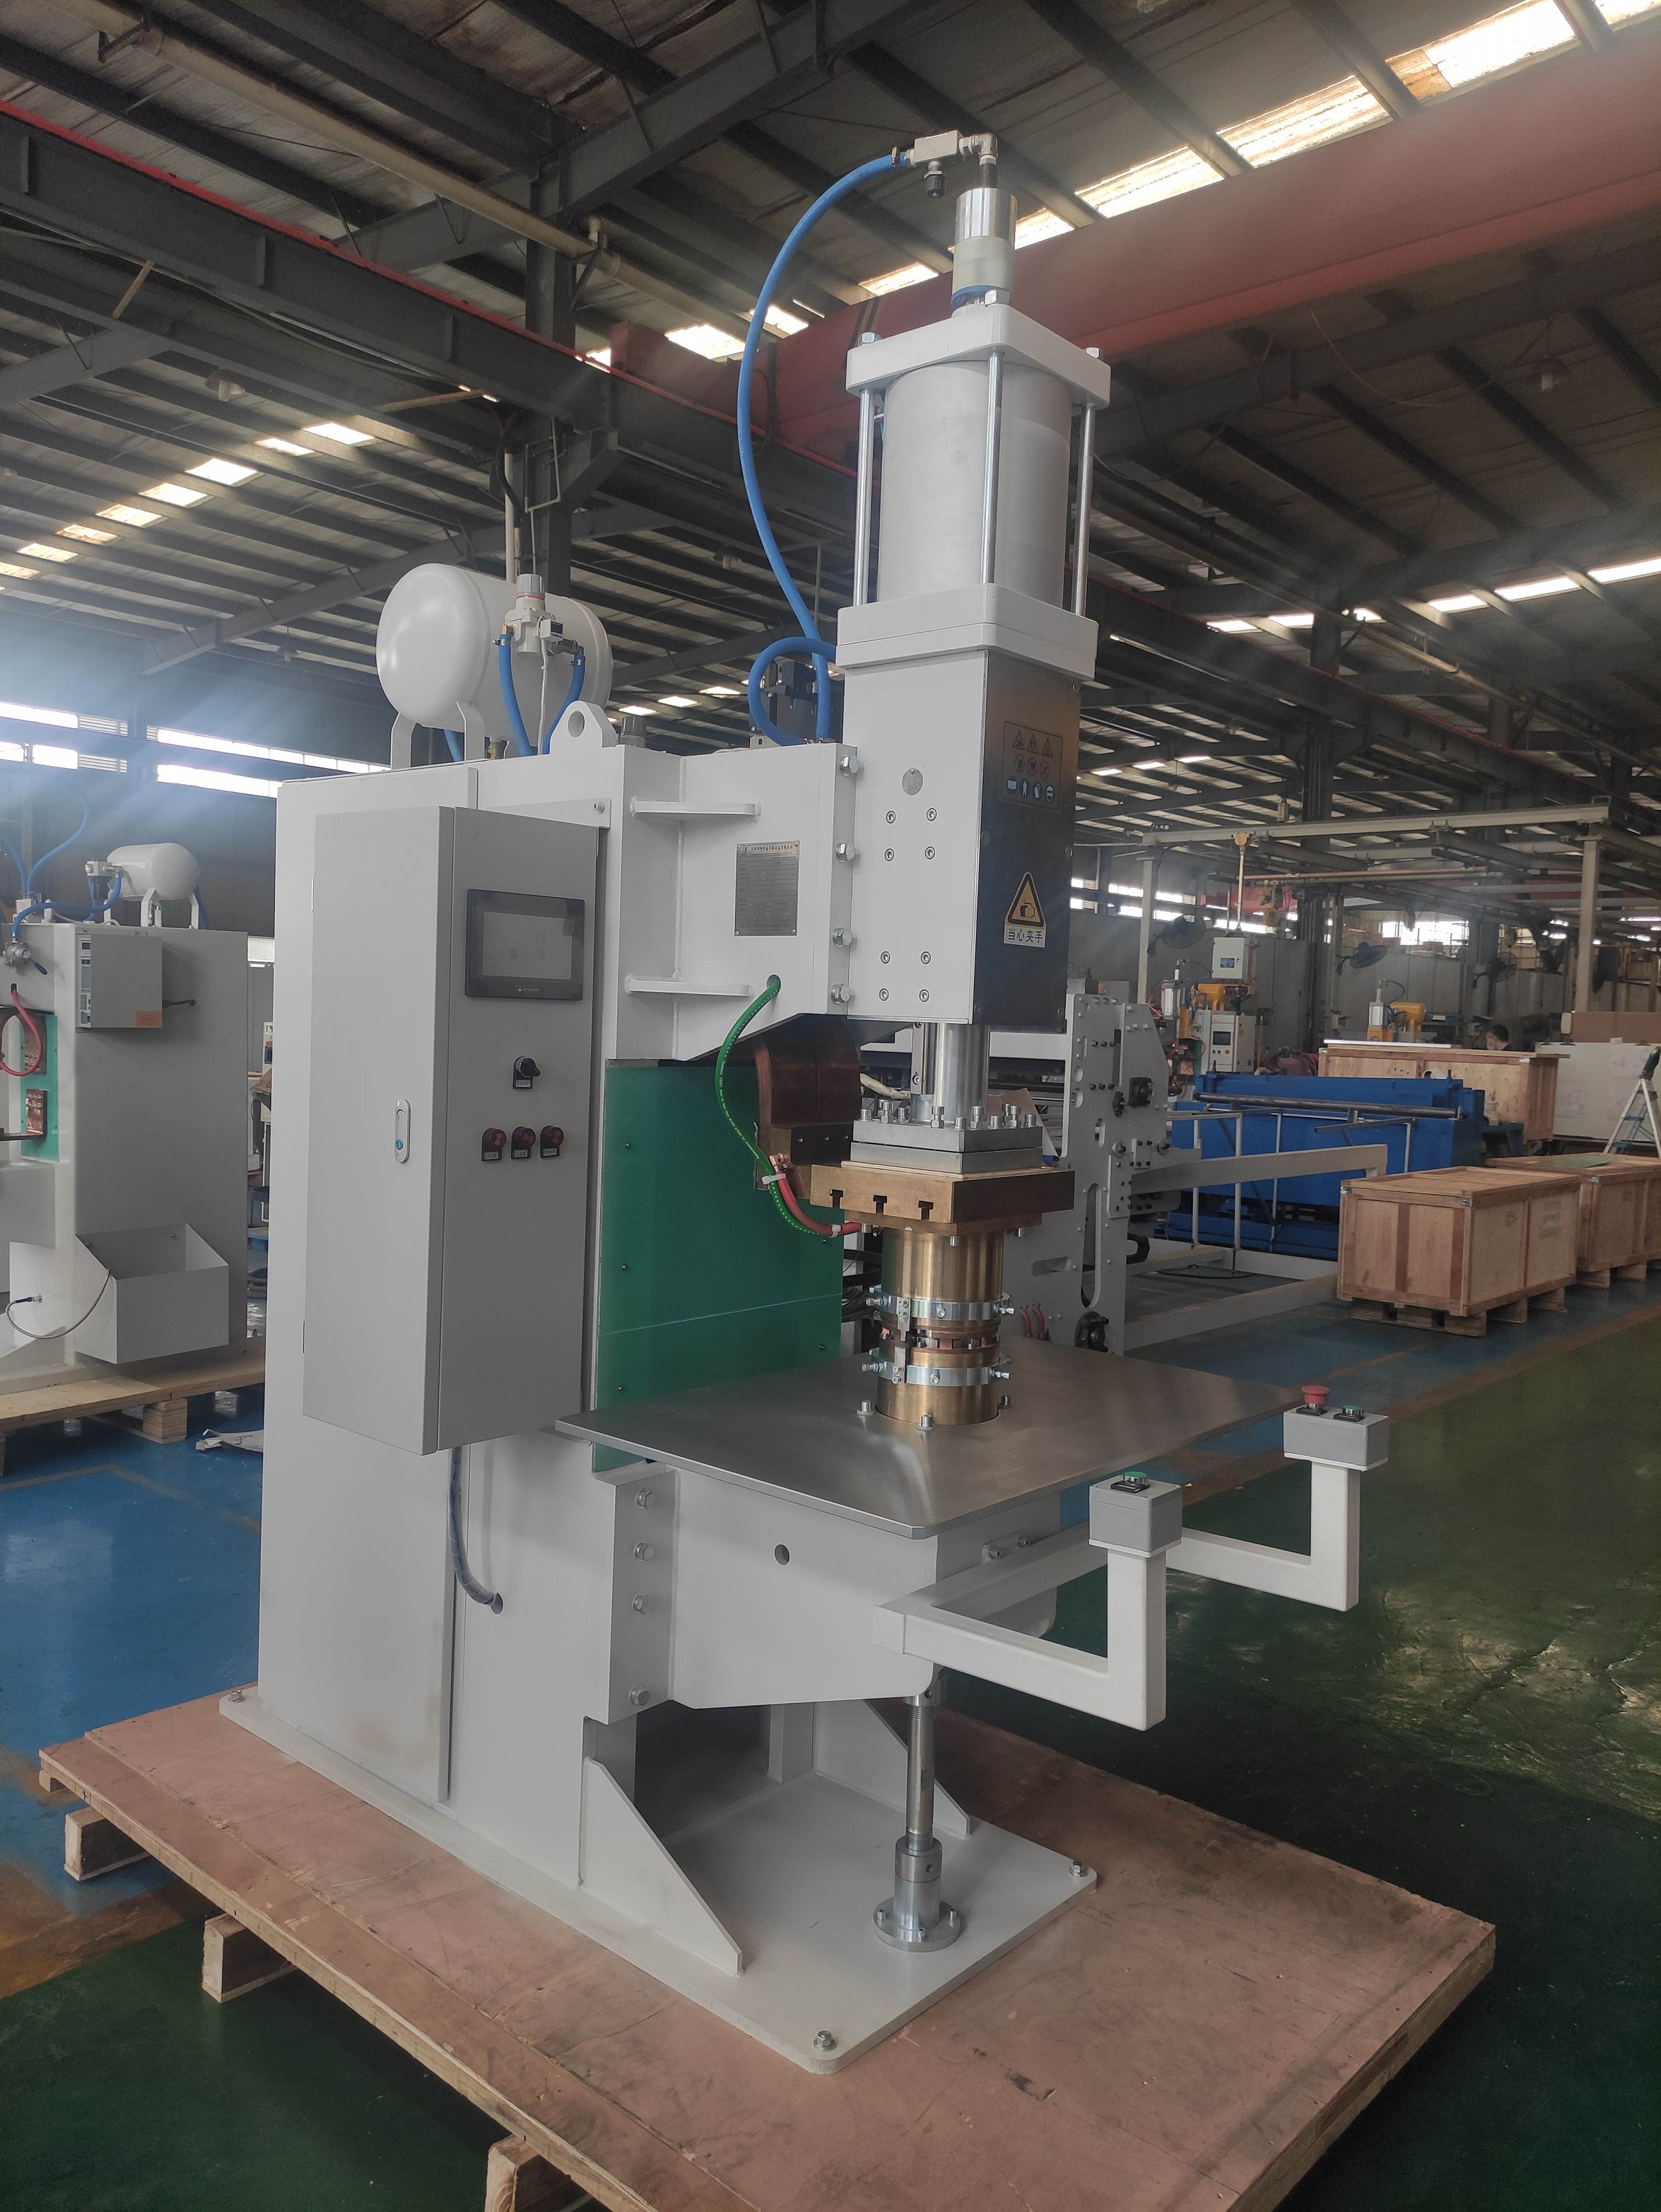
Built around a heavy-duty pneumatic press frame with an integrated gas storage tank, the machine maintains stable electrode force during each weld, minimizing splash and weld inconsistency. The controller stores multiple weld schedules, so operators can switch between different tank shell materials or thicknesses with one click. With dual spot and projection welding capability, this equipment also handles general resistance welding tasks beyond circular fuel tank rings, offering plant managers a flexible, production-ready solution.
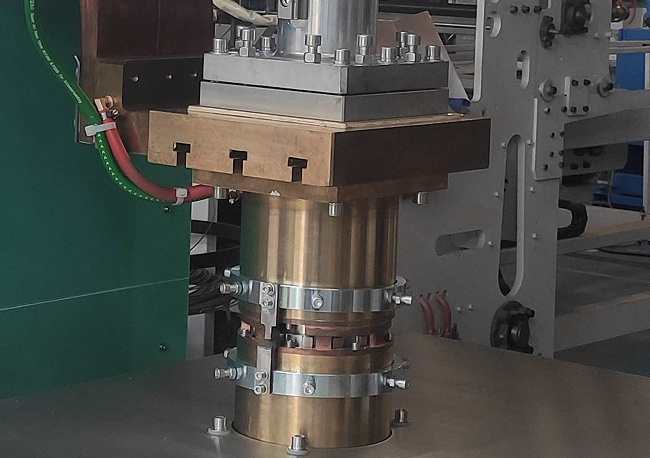
Each annular electrode ring carries seven fixed convex points. When the upper and lower rings press together, power is applied at all seven locations at once, forming seven uniform weld nuggets in a single stroke. This design shortens cycle time and keeps the weld distribution even around the circumference.
The upper and lower electrode rings attach through standardized quick-install interfaces. When switching from one tank diameter to another, the operator replaces the full ring assembly without recalibrating electrode alignment, preserving coaxiality and reducing changeover downtime.
The controller retains multiple weld recipes, each with its own current, time, and pressure values. This allows quick process switching for different shell thicknesses or material combinations, keeping small-batch and multi-variety production economical.
Beyond annular fuel tank ring welding, the machine accepts interchangeable electrode forms for general projection and spot welding tasks. This dual-function design broadens the equipment’s process range and improves return on investment for job shops.
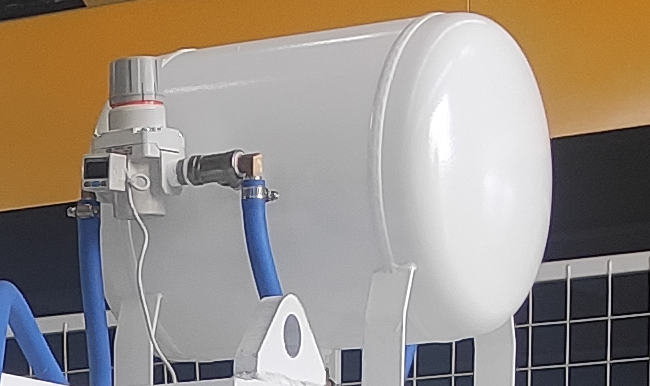
The dedicated gas storage tank buffers pressure fluctuations during the welding cycle, ensuring the electrode force remains steady from the first weld to the last. This contributes to repeatable nugget quality across long production runs.
| Industry | Typical Workpiece | Welding Mode |
|---|---|---|
| Fuel Tank Manufacturing | Tank shell half section with metal ring | Annular projection welding, 7 points per cycle |
| Automotive Components | Fuel filler necks, brackets, mounting plates | Spot welding with interchangeable electrodes |
| General Metal Fabrication | Nuts, studs, and sheet metal projections | Projection welding with flat platen |
| New Energy Equipment | Battery housing covers, sealed containers | Spot and projection welding |
The machine applies low-voltage, high-current resistance heating at the interface between the fuel tank shell and the pre-formed metal ring. A pneumatic cylinder drives the upper electrode ring downward, pressing the workpiece against the lower ring. Current flows through the seven convex points on the ring, generating localized heat that fuses the materials. The gas storage tank stabilizes air pressure during the squeeze cycle, while the controller manages weld time, current amplitude, and electrode force. After the weld solidifies, the cylinder retracts and the finished part is removed.
| Parameter | Unit | DN-40 | DN-63 | D(T)N-80 | D(T)N-100 | D(T)N-125 | D(T)N-160 | D(T)N-200 |
|---|---|---|---|---|---|---|---|---|
| Rated power At 50% | KVA | 40 | 63 | 80 | 100 | 125 | 160 | 200 |
| Rated primary power | V | 380 | 380 | 380 | 380 | 380 | 380 | 380 |
| Secondary Voltage | V | 5.2 | 6.7 | 7.9 | 8.3 | 8.6 | 9.1 | 10.6 |
| Rated frequency | HZ | 50/60 | 50/60 | 50/60 | 50/60 | 50/60 | 50/60 | 50/60 |
| Max.Short Circuit Current | KA | 14 | 15 | 16 | 18 | 20 | 28 | 34 |
| Max. weld power | KVA | 62 | 86 | 170 | 280 | 300 | 330 | 410 |
| Throat | MM | 400 | 400 | 400 | 450 | 450 | 450 | 450 |
| Max.Froce at electrodes | N | 6000 | 6000 | 10000 | 10000 | 10000 | 12000 | 12000 |
| Working stroke | MM | 20 | 20 | 30 | 40 | 40 | 50 | 50 |
| Cooling Water Consumpion 2.5bar | L/min | 6 | 6 | 8 | 8 | 8 | 10 | 10 |
| Electrodes tip | MM | Φ13*45 | Φ13*45 | Φ16*45 | Φ16*45 | Φ16*45 | Φ20*45 | Φ20*45 |
| Arms | MM | Φ50*150 | Φ50*150 | Φ80*220 | Φ80*220 | Φ80*220 | Φ80*220 | Φ80*220 |
| Projection Clamping Plate | MM | 125*125 | 125*125 | 200*200 | 200*200 | 200*200 | 200*200 | 200*200 |
| Max.Welding Capaciry A3 steel | MM | 2.5+2.5 | 3+3 | 4+4 | 4.5+4.5 | 5+5 | 5+5 | 6+6 |
Replace the annular electrode ring pair with the size matching the workpiece. The quick-install interface locks the ring in position without re-aligning individual electrodes. Then recall the corresponding weld schedule from the controller, and the machine is ready for the next batch.
Yes. By swapping the annular electrode assembly for standard spot welding arms or a projection welding platen, the machine handles general resistance welding tasks such as nut projection, bracket spot welding, and sheet metal joining.
For a typical fuel tank shell and metal ring assembly, each welding cycle can be completed in roughly 8 seconds, including manual loading and unloading. Actual cycle time depends on material thickness, electrode condition, and operator skill.
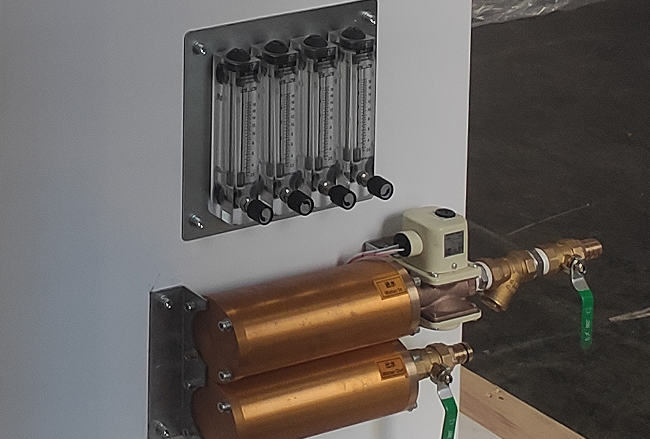
All waterway components are surface-treated to resist rust. Cooling water flows through the electrode rings and returns to the tank. Operators can inspect the return flow to detect and clear any blockages early.
Yes. We offer free sample welding and process design services. Send us your workpiece drawings or physical samples, and our engineering team will validate the solution before you commit to production.
Send us your workpiece drawings and production requirements. Our engineering team will evaluate your application, configure the optimal solution, and provide a detailed proposal with electrode design and automation integration options.
Send Drawing | Request Welding Test | Get Custom Solution