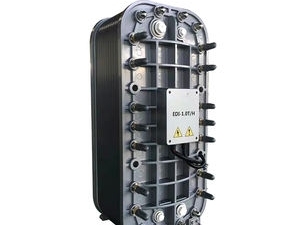
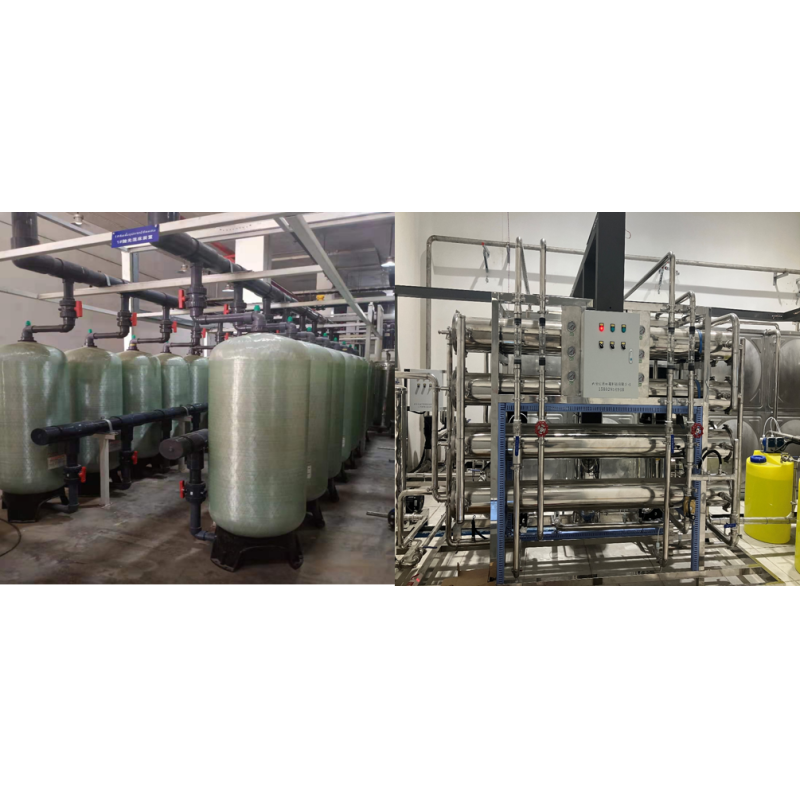
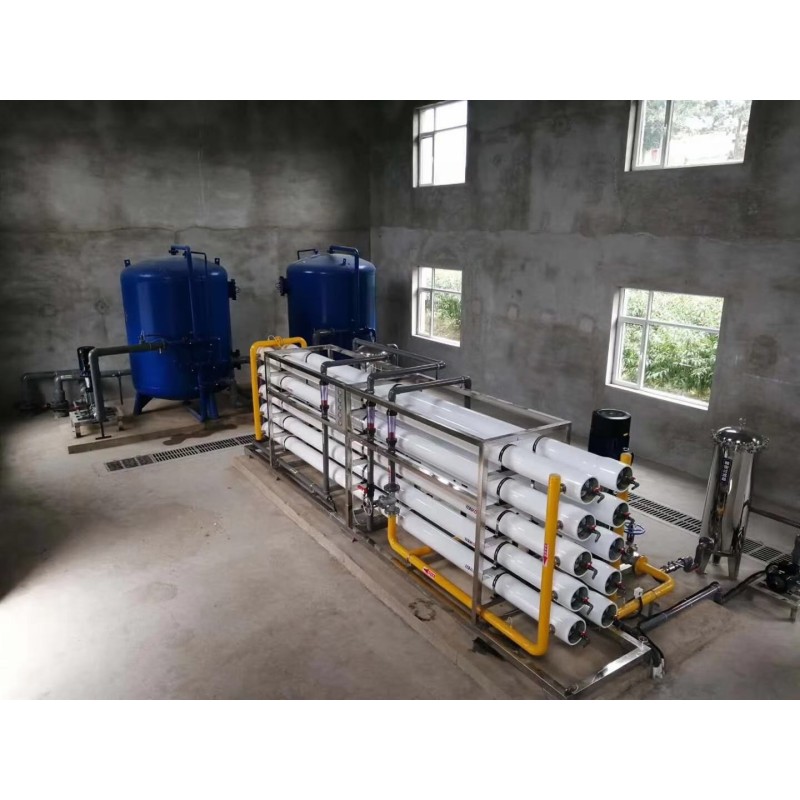
This High Flow EDI System is a large-capacity industrial deep deionization water treatment equipment specifically customized for new energy battery manufacturing, lithium battery processing, battery material production, and new energy industrial supporting projects. New energy battery production requires massive, stable high-purity deionized water for electrode cleaning, material blending, workshop process water, and equipment rinsing.
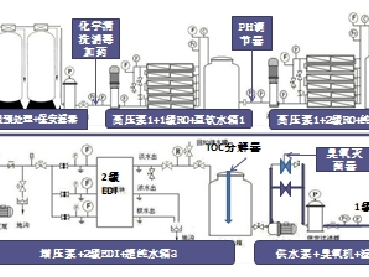
Conventional small-flow EDI equipment cannot meet the continuous large-volume water demand of battery mass production and is prone to insufficient water yield and unstable water quality under long-term full-load operation. This high-flow EDI unit adopts upgraded large-flux membrane stack structure and industrial enhanced purification technology, matched with two-stage RO pretreatment system.
It supports high-volume continuous water output, efficiently removes trace ions, micro impurities, and conductive substances in water. Featuring non-chemical automatic operation, strong load resistance, and stable high-flow water supply capacity, it serves as the standard core supporting water treatment equipment for large-scale new energy battery factories.
Stable qualified water after two-stage RO purification uniformly enters the high-flow industrial EDI membrane stack. Under continuous stable DC electric field, the high-flux ion exchange resin inside the equipment rapidly adsorbs residual trace cations, anions, and tiny conductive impurities.
Impurity ions complete directional migration and precise separation through high-permeability selective ion exchange membranes, and are concentrated and discharged through large-flow concentrated water channels. The system realizes automatic electric regeneration of internal resin during high-load continuous operation without chemical additives, ensuring zero secondary pollution and long-term stable purification capacity.
Equipped with industrial high-power supporting control system and real-time water quality monitoring modules, the equipment intelligently adjusts operating voltage and flow parameters according to production water consumption changes. It maintains stable high-flow and high-purity water output to meet the uninterrupted water demand of new energy battery production lines.
| Applicable Scenarios | New energy battery manufacturing factories, lithium battery production lines, battery material processing, new energy industrial park water projects |
| Customizable Water Flow | 5-100m³/h (large industrial flow customizable) |
| Matching Pretreatment | Two-stage RO reverse osmosis purification system |
| Outlet Water Standard | New energy battery industrial grade deionized water |
| Stable Water Resistivity | 15-18.2 MΩ*cm |
| Comprehensive Desalination Rate | ≥99.5% |
| Core Feature | Large flux, high-load resistance, stable high-flow water output, non-chemical operation |
| Operation Mode | 24-hour full-load automatic continuous unattended operation |
| Control System | Industrial PLC intelligent linkage + real-time water quality monitoring |
The equipment adopts export-standard fumigated wooden case packaging, equipped with complete installation drawings, wiring diagrams and professional operation and maintenance manuals.
Quality Warranty: Core high-flow EDI membrane stacks, intelligent control cabinets and precision monitoring sensors enjoy 1-year quality warranty.
Custom Solutions: We provide personalized large-flow customized configuration and system matching solutions according to factory daily water consumption.
Technical Support: Offering long-term remote technical support and global after-sales service for new energy industry water treatment projects.