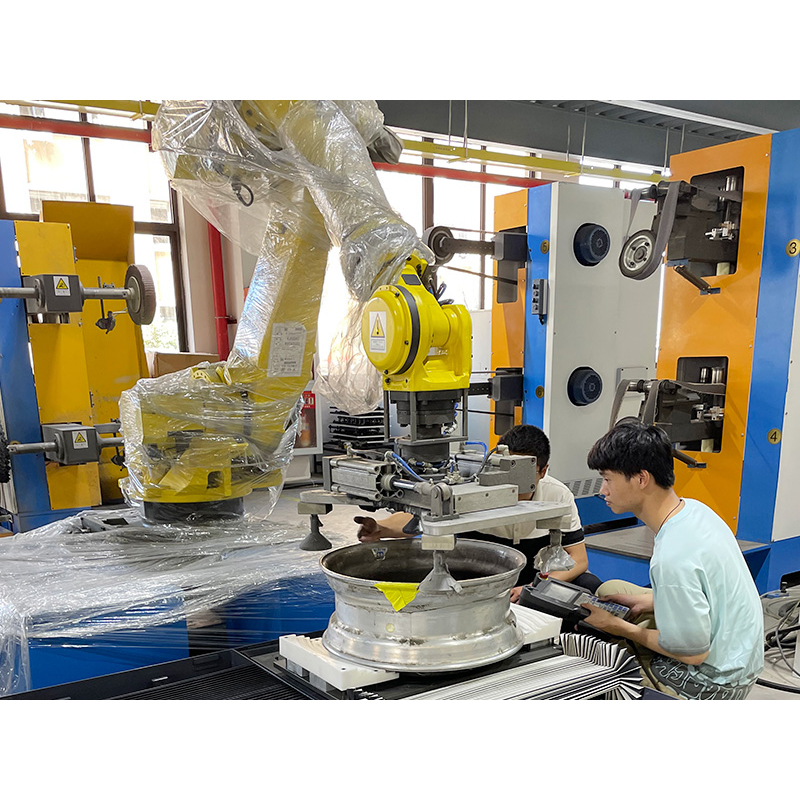
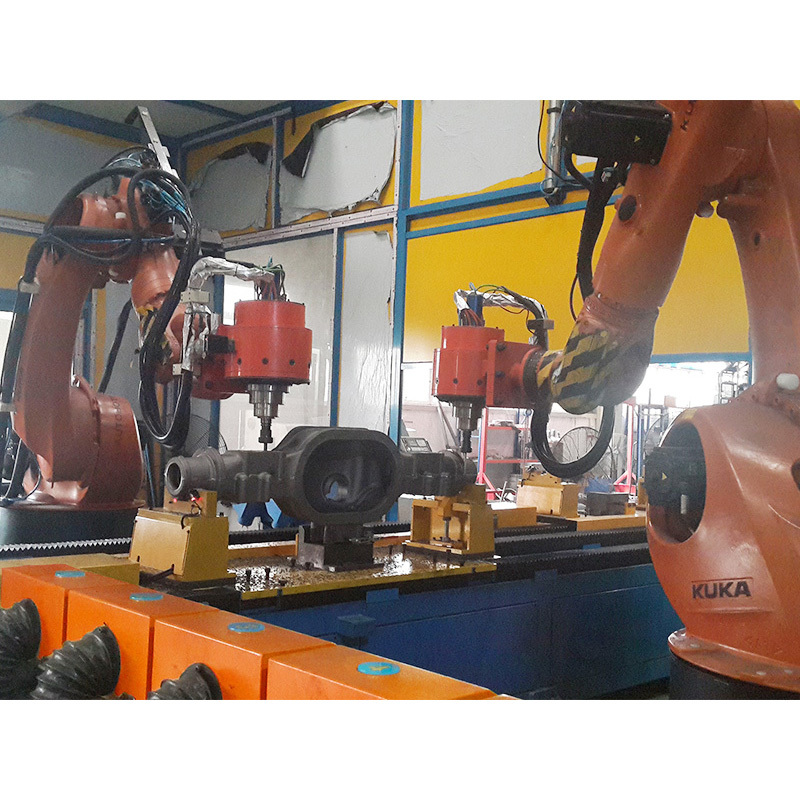
Zero Over-Cutting. 100% Repeatable Edge Radius. Turn Bottleneck Manual Deburring into a 24/7 Lights-Out Automated Process.
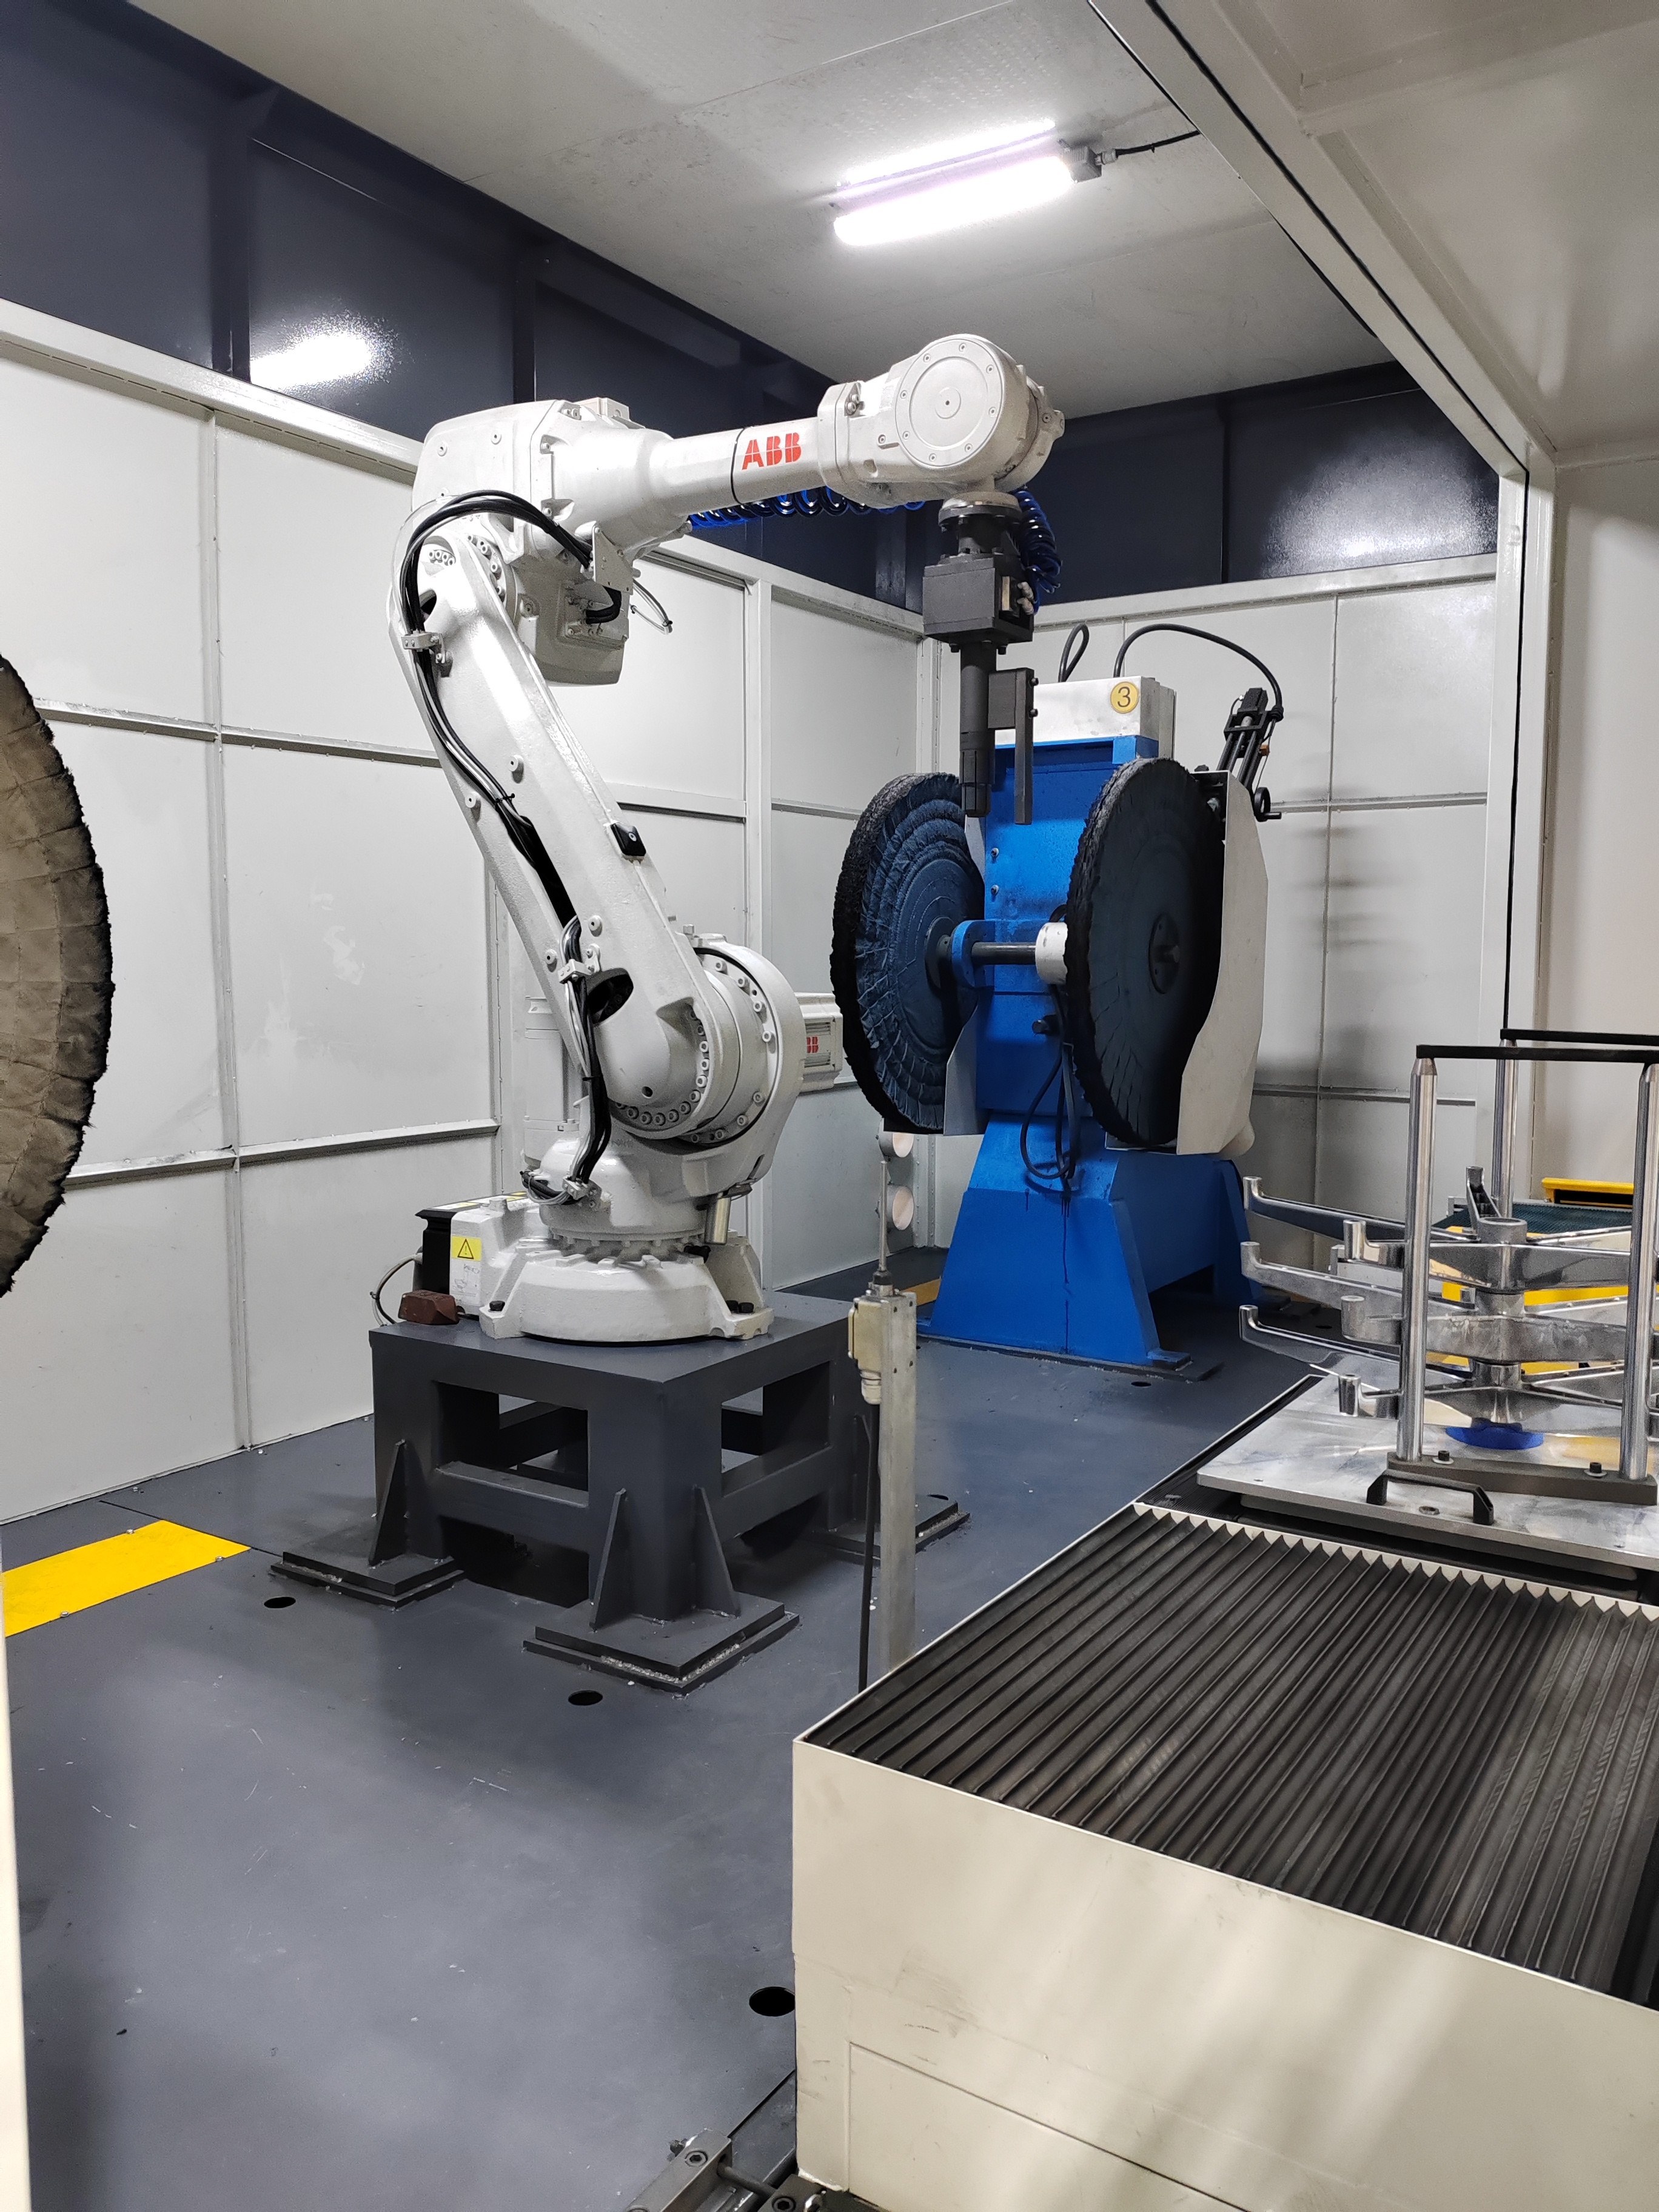
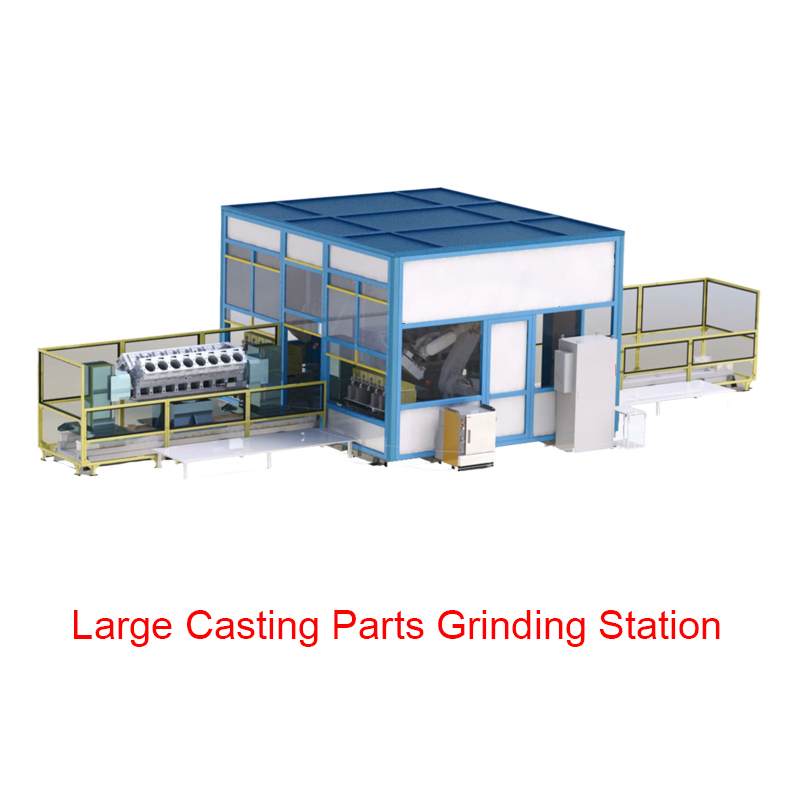
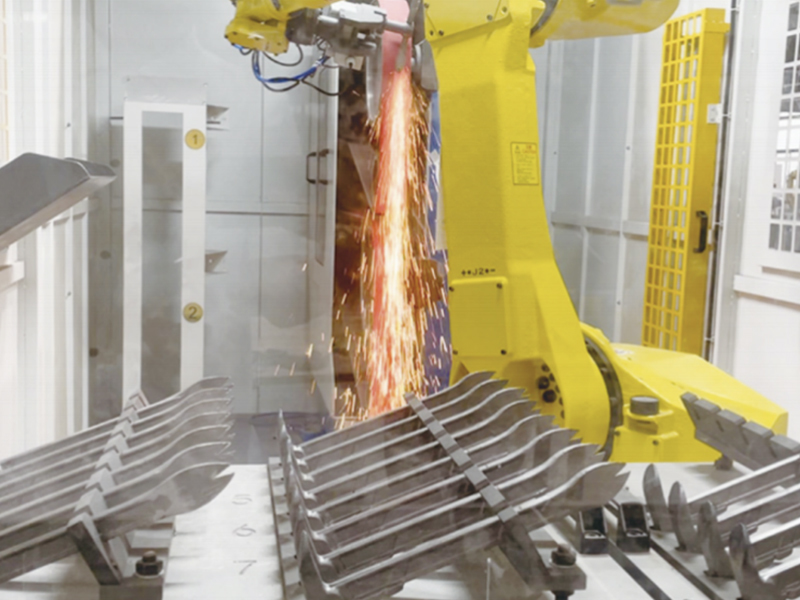
Engineered with 6-axis articulated robotics and active pneumatic/servo force compensation, the [Model: ARD-06A] delivers micron-level edge breaking, chamfering, and flash removal across complex CNC-machined aerospace components, precision castings, and heavy industrial parts.
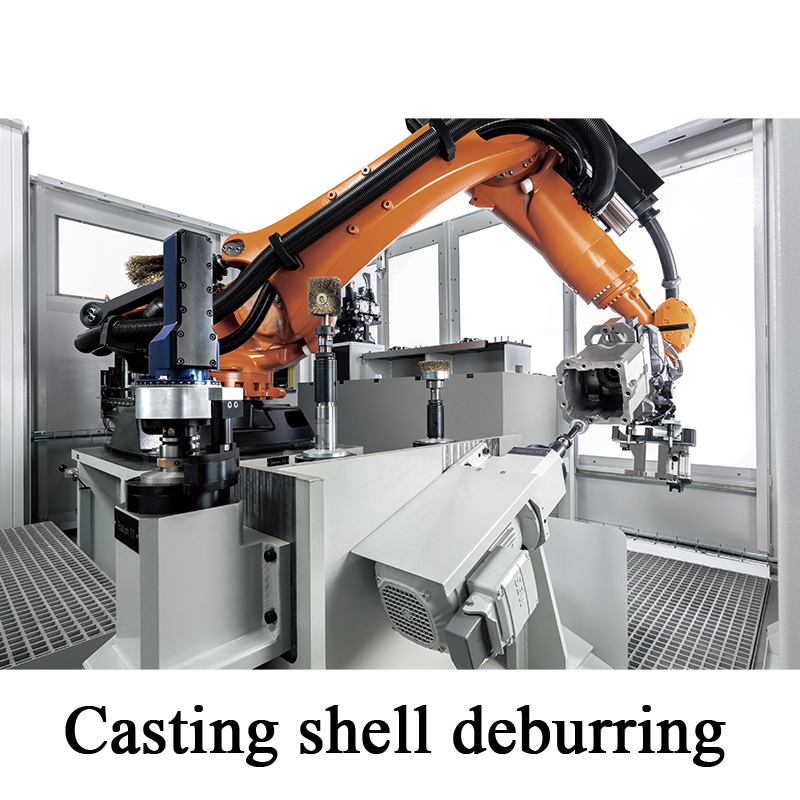
Unlike rigid CNC machines that require perfect part positioning, our robotic deburring head features real-time axial and radial compliance. Whether removing heavy casting flash or delicate CNC milling burrs, the spindle dynamically adjusts contact pressure (2N – 200N adjustable) to absorb part-to-part dimensional variations up to ±3–8 mm.
Complex parts require more than one tool. The built-in 4-to-8 station ATC rack allows the robot to execute coarse flash removal, precision chamfering, cross-hole deburring, and final nylon/ceramic brushing in a single clamping cycle—eliminating secondary handling.
No complex robot coding required on the shop floor. Import your part's 3D CAD model (STEP / IGES) directly into our offline programming software to generate collision-free deburring trajectories in minutes. Ideal for High-Mix, Low-Volume (HMLV) aerospace production.
As abrasive brushes and grinding wheels wear down, the system automatically measures tool diameter/length via a laser or touch sensor and adjusts TCP (Tool Center Point) speed and offset—ensuring the 1,000th part looks identical to the 1st.
Q1: How does the robot avoid gouging or over-cutting when my castings or forgings have dimensional variations?
A: Our machine integrates an active compliant floating spindle (available in precision pneumatic or closed-loop servo-electric versions). Instead of following a rigid path like a CNC mill, the spindle maintains a constant programmed contact force against the workpiece edge—automatically floating up to ±6–8 mm to absorb casting tolerances, fixture errors, and thermal warpage.
Q2: We manufacture High-Mix, Low-Volume (HMLV) aerospace parts. Is programming new parts time-consuming?
A: Not at all. With our Offline Programming (OLP) software, you can generate tool paths directly from your part's 3D CAD model on a PC while the machine continues running production. Combined with zero-point quick-change fixtures, mechanical and program changeover between part families takes less than 10–15 minutes.
Q3: Can this machine deburr internal cross-holes, deep pockets, and back-side edges?
A: Yes. By combining a 6-axis industrial robot with an automatic tool changer (ATC), the system can switch from a standard chamfer mill to specialized lollipop cutters, back-deburring tools, or micro abrasive brushes to reach intersecting holes, undercuts, and deep cavities in a single cycle.
Q4: How do you handle tool wear on abrasive brushes and grinding wheels?
A: The cell includes an automated Tool Wear Compensation System. After a preset number of cycles, the robot touches off the brush or wheel against an in-cabin sensor, calculates the diameter loss, and automatically offsets the TCP path and spindle RPM to maintain consistent material removal.