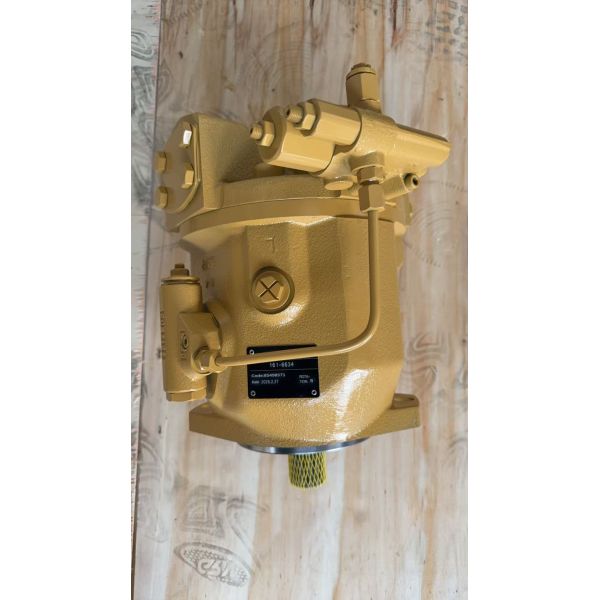
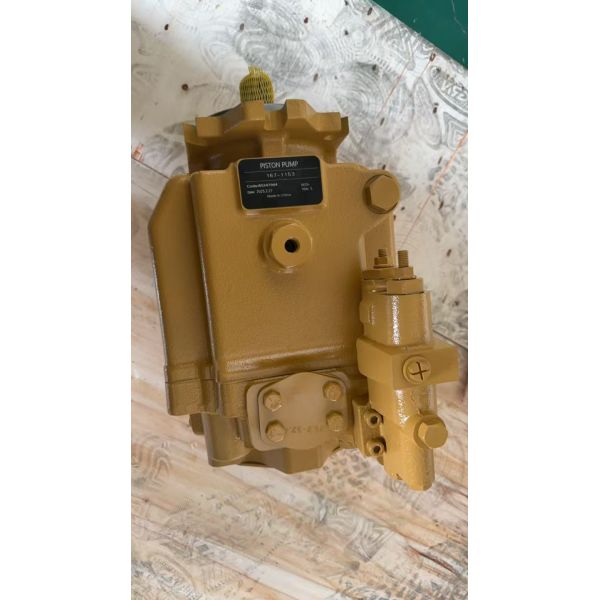
The 162-0770 (superseded from 10R-0855) hydraulic pump is a critical drivetrain-mounted gear pump engineered for CCAT 966G and 972G Wheel Loaders. These mid-size loaders are workhorses in quarry face loading, aggregate handling, and heavy construction material movement, where the hydraulic pump must deliver consistent flow to the loader's lift arms, bucket tilt cylinders, and auxiliary circuits across continuous 10-12 hour duty cycles. This replacement pump is manufactured to CCAT OEM engineering specifications, with every critical dimension verified on a CMM (Coordinate Measuring Machine) against original equipment blueprints.
ProblemCCAT 966G and 972G operators commonly encounter a progressive decline in hydraulic performance characterized by slow bucket lift speed, delayed tilt response, and insufficient breakout force when digging into compacted material piles. These symptoms indicate the 162-0770 pump is losing volumetric efficiency—internal gear-to-housing clearance has widened beyond the service limit of 0.08 mm, causing pressurized oil to bypass internally rather than reaching the work cylinders. In severe cases, operators report that the loader can no longer lift a full bucket of 2.9–3.5 metric tons to maximum dump height within the OEM-specified 6.5-second cycle time. The financial impact extends beyond reduced productivity: a 966G burning an extra 3-4 liters of diesel per hour to compensate for hydraulic inefficiency adds approximately USD 8,000–12,000 to annual fuel costs per machine.
CauseThree primary failure mechanisms degrade the 162-0770 pump in wheel loader applications. First, shock loading: when the bucket strikes an immovable object (bedrock, reinforced concrete) at full hydraulic pressure, instantaneous pressure spikes exceeding 5,000 PSI can deform gear tooth profiles and crack bearing cage retainers. Second, contaminated oil circulation: wheel loaders operating in dusty quarry environments ingest airborne silica particles through breather caps and cylinder rod wipers; particles measuring 10-20 microns become embedded in the aluminum alloy wear plates that sandwich the gear set, creating abrasive tracks that progressively deepen and increase internal leakage. Third, inadequate warm-up procedures in cold climates: operators who immediately engage full-load digging with oil viscosity above 1,000 cSt starve the pump inlet, causing cavitation erosion that pits gear faces and the suction-side housing bore within the first 50 hours of operation.
SolutionOur 162-0770 replacement pump integrates targeted durability upgrades to combat each failure mode. Gear sets are CNC-ground from 20CrMnTi alloy steel and subjected to cryogenic treatment (-185°C deep freeze followed by controlled tempering), which transforms retained austenite to martensite and increases wear resistance by 25-35% over conventionally heat-treated gears. The wear plates are upgraded from standard aluminum alloy to leaded-tin-bronze (CuSn10Pb10), a bearing-grade material with embedded solid lubricant that maintains a low-friction interface even during momentary oil starvation events. Pressure-balanced bearing blocks with laser-engraved lubrication grooves distribute oil film evenly across the gear face, eliminating dry spots that cause localized overheating. Each pump undergoes a rigorous 45-minute test protocol including 10 shock-load cycles at 125% rated pressure to validate structural integrity before shipment. For heavy-duty quarry applications, we offer an optional high-capacity inlet strainer upgrade rated at 150 microns absolute filtration with a built-in magnetic core to capture ferrous debris before it enters the pump.
Key Features| Parameter | Specification |
|---|---|
| Part Number | 162-0770 (Supersedes 10R-0855) |
| Pump Type | External Gear Pump (Fixed Displacement) |
| Displacement | Refer to OEM Specification (Approx. 80–100 cc/rev) |
| Maximum Operating Pressure | 3,500 PSI (241 bar) Continuous |
| Peak Intermittent Pressure | 4,000 PSI (276 bar) for <10 Seconds |
| Rated Speed Range | 500–2,200 RPM |
| Shaft Drive Type | Splined Shaft (Matches OEM Engine PTO Coupling) |
| Port Configuration | SAE 4-Bolt Split Flange (ANSI/SAE J518) |
| Housing Material | High-Strength Gray Cast Iron (HT250, ISO 185/JL/250) |
| Gear Material | 20CrMnTi Cryo-Treated Alloy Steel (HRC 60-63) |
| Wear Plate Material | CuSn10Pb10 Leaded-Tin-Bronze (Self-Lubricating) |
| Seal Type | Triple-Lip FKM Shaft Seal with Dust Exclusion Lip |
| Net Weight | Approx. 22–26 kg |
| Certification | ISO 9001:2015, Individual Test Certificate with CMM Dimensional Report |
The 162-0770 hydraulic pump is purpose-designed for the following CCAT Wheel Loader platforms:
Cross-reference note: The 10R-0855 is the CCAT Reman part number for this same pump assembly. Both 162-0770 (new OEM) and 10R-0855 (remanufactured) share identical form, fit, and function. This replacement pump is compatible with either designation and is suitable as a cost-effective alternative to both OEM new and reman channels.
Selection GuideTo ensure correct pump selection for your CCAT wheel loader, follow this verification procedure:
Each 162-0770 pump is shipped in a reinforced export plywood crate with shock-absorbing polyurethane foam inserts specifically contoured to the pump profile. The pump assembly is vacuum-sealed in multi-layer VCI (Volatile Corrosion Inhibitor) barrier film, providing 24 months of indoor corrosion protection. All ports are sealed with desiccant-filled plugs and tamper-evident caps. A QR-coded quality certificate affixed to the crate links to a digital test report containing: serial number, build date, flow curve (L/min vs. RPM at 3 pressure points), volumetric efficiency percentage, case drain flow measurement, noise level in dBA at 1 meter, and the CMM dimensional inspection summary. We maintain digital records for 5 years and can retrieve historical test data for any serial number upon request.