Product Introduction
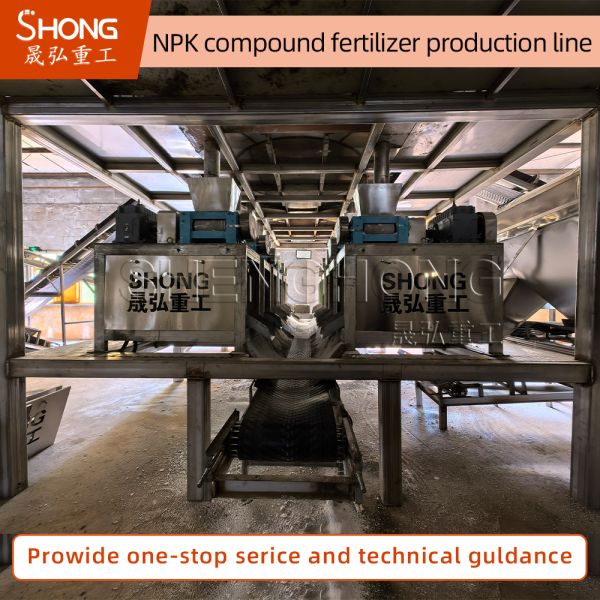
Environmental compliance and raw material loss are two major challenges facing modern industrial chemical processing. Our cutting-edge Waste-Free Eco-Friendly Double Roller Compactor Plant is engineered specifically to eliminate these factory bottlenecks.
This innovative zero waste fertilizer machine utilizes a continuous dry mechanical compaction loop that discharges no wastewater, releases no hazardous gases, and generates no industrial waste residue. Built around a state-of-the-art eco-friendly granulation process, the system automatically captures and redirects 100% of fine chemical powders back into the production cycle, making it the perfect dust-free fertilizer processing solution for eco-conscious enterprises.
Sustainable Industrial Process Flow & Working Principle
This zero waste fertilizer machine runs on a synchronized, clean-technology processing loop:
1. Sealed Negative-Pressure Material Ingest
Fine raw powders enter the system through a fully sealed vacuum feeding mechanism, preventing dry chemicals from escaping into the surrounding factory atmosphere.
2. Homogeneous Moisture-Free Blending
A fluidless paddle mixer agitates the raw powder particles, establishing a uniform matrix ready for instant high-pressure physical bonding.
3. Eco-Press Mechanical Compaction
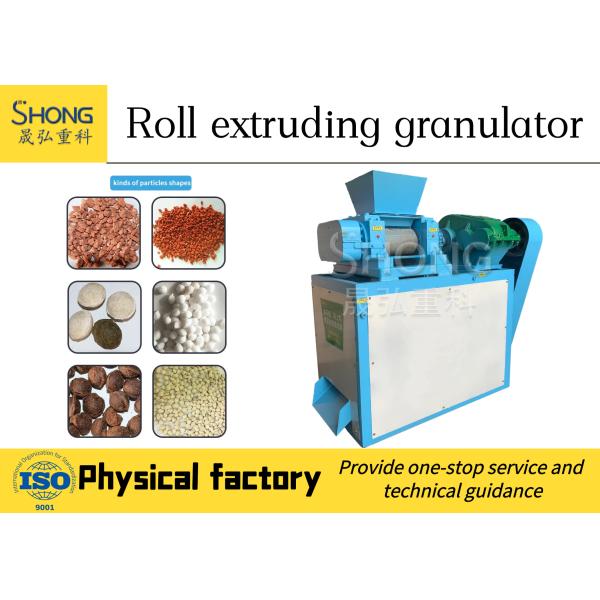
The dry powder drops into the main roller cavity. Two massive alloy rollers compress the loose mix into ultra-dense hard sheets without using steam or water-based chemical additives.
4. Low-Dust Mechanical Flake Crushing
The solid compressed sheets are guided into an enclosed under-roller granulating mill, which uses specialized slow-speed teeth to crack the flakes into raw granules while minimizing dust creation.
5. High-Frequency Separation & Sifting
The broken fragments travel through an enclosed rotary screening machine to extract standard commercial granules (2-4mm).
6. Automated Vacuum Powder Reclamation
All undersized fine dust passing through the sifter screen is collected by an underlying vacuum hopper and instantly conveyed via a closed elevator right back into the main feeder.
7. Micro-Glazing Protective Coating
Qualified granules enter a compact rotary coating drum. A micro-layer of organic anti-caking agent is mist-sprayed to seal the particles, increasing shelf-life and preventing degradation during long-term storage.
8. Dust-Free Quantitative Packing
The finished clean granules move into an automated weighing and bagging station, where they are packaged into 25kg/50kg commercial bags with integrated air-extraction sealing to ensure zero dust leakage.