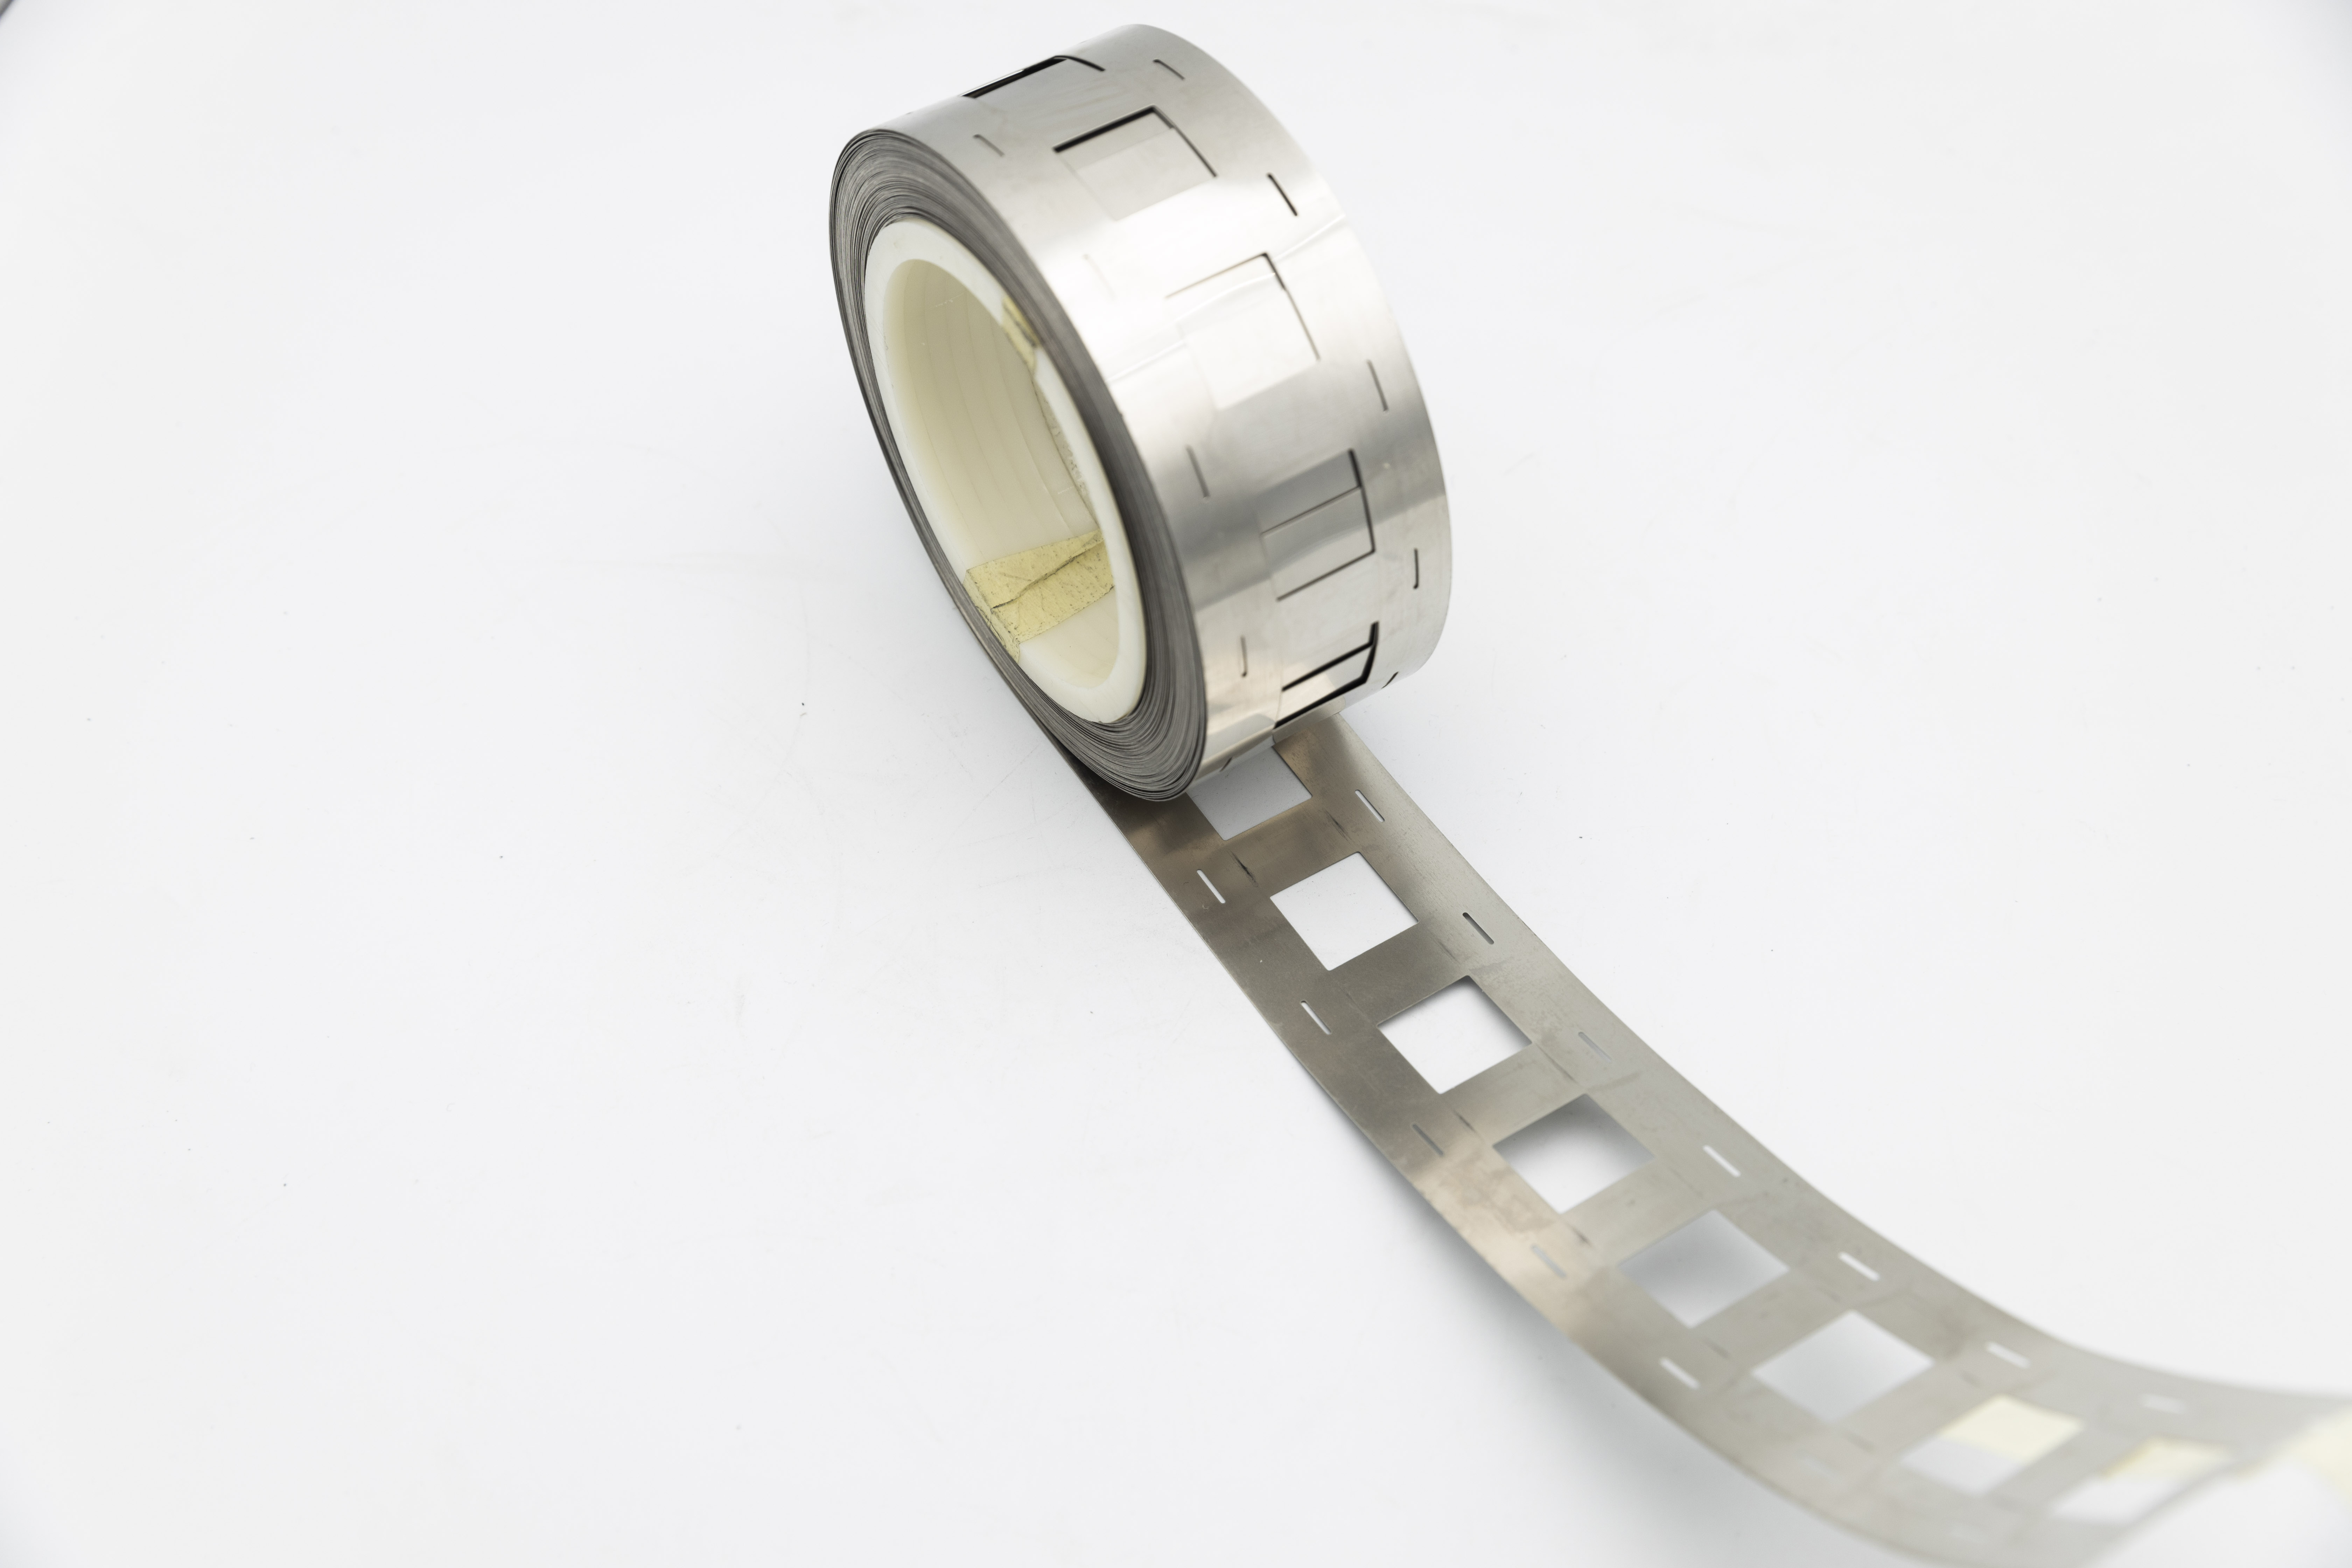
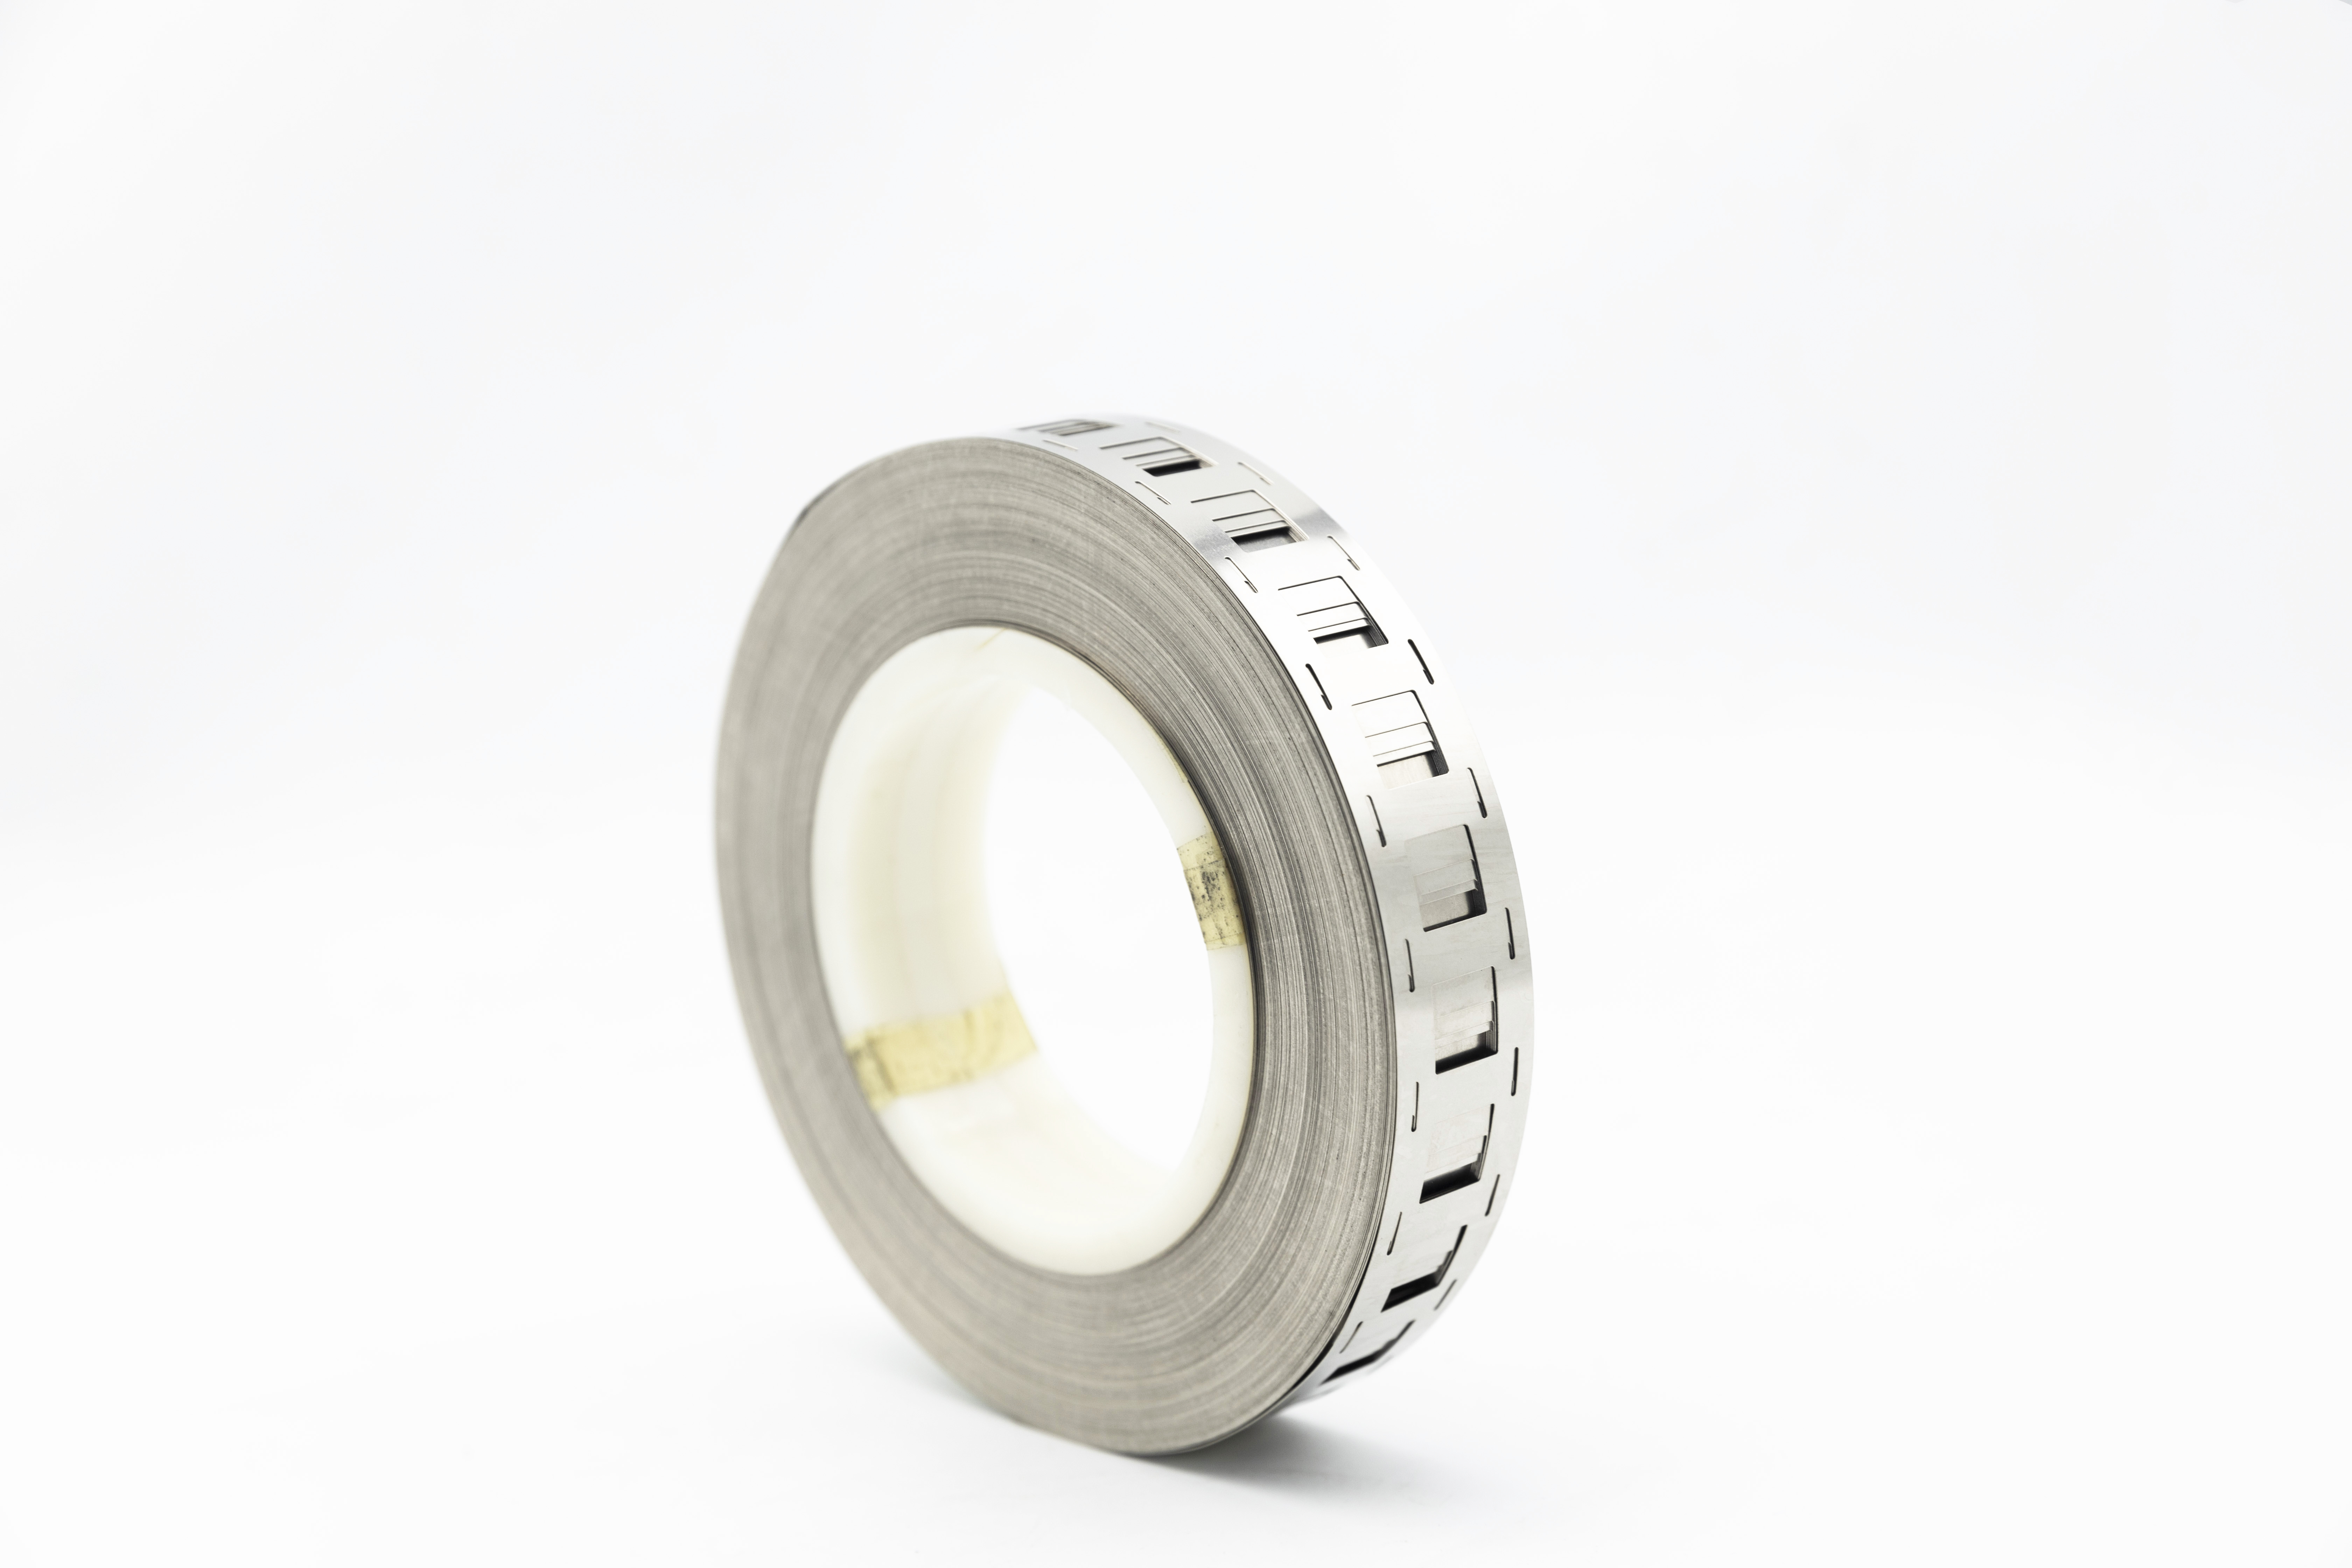
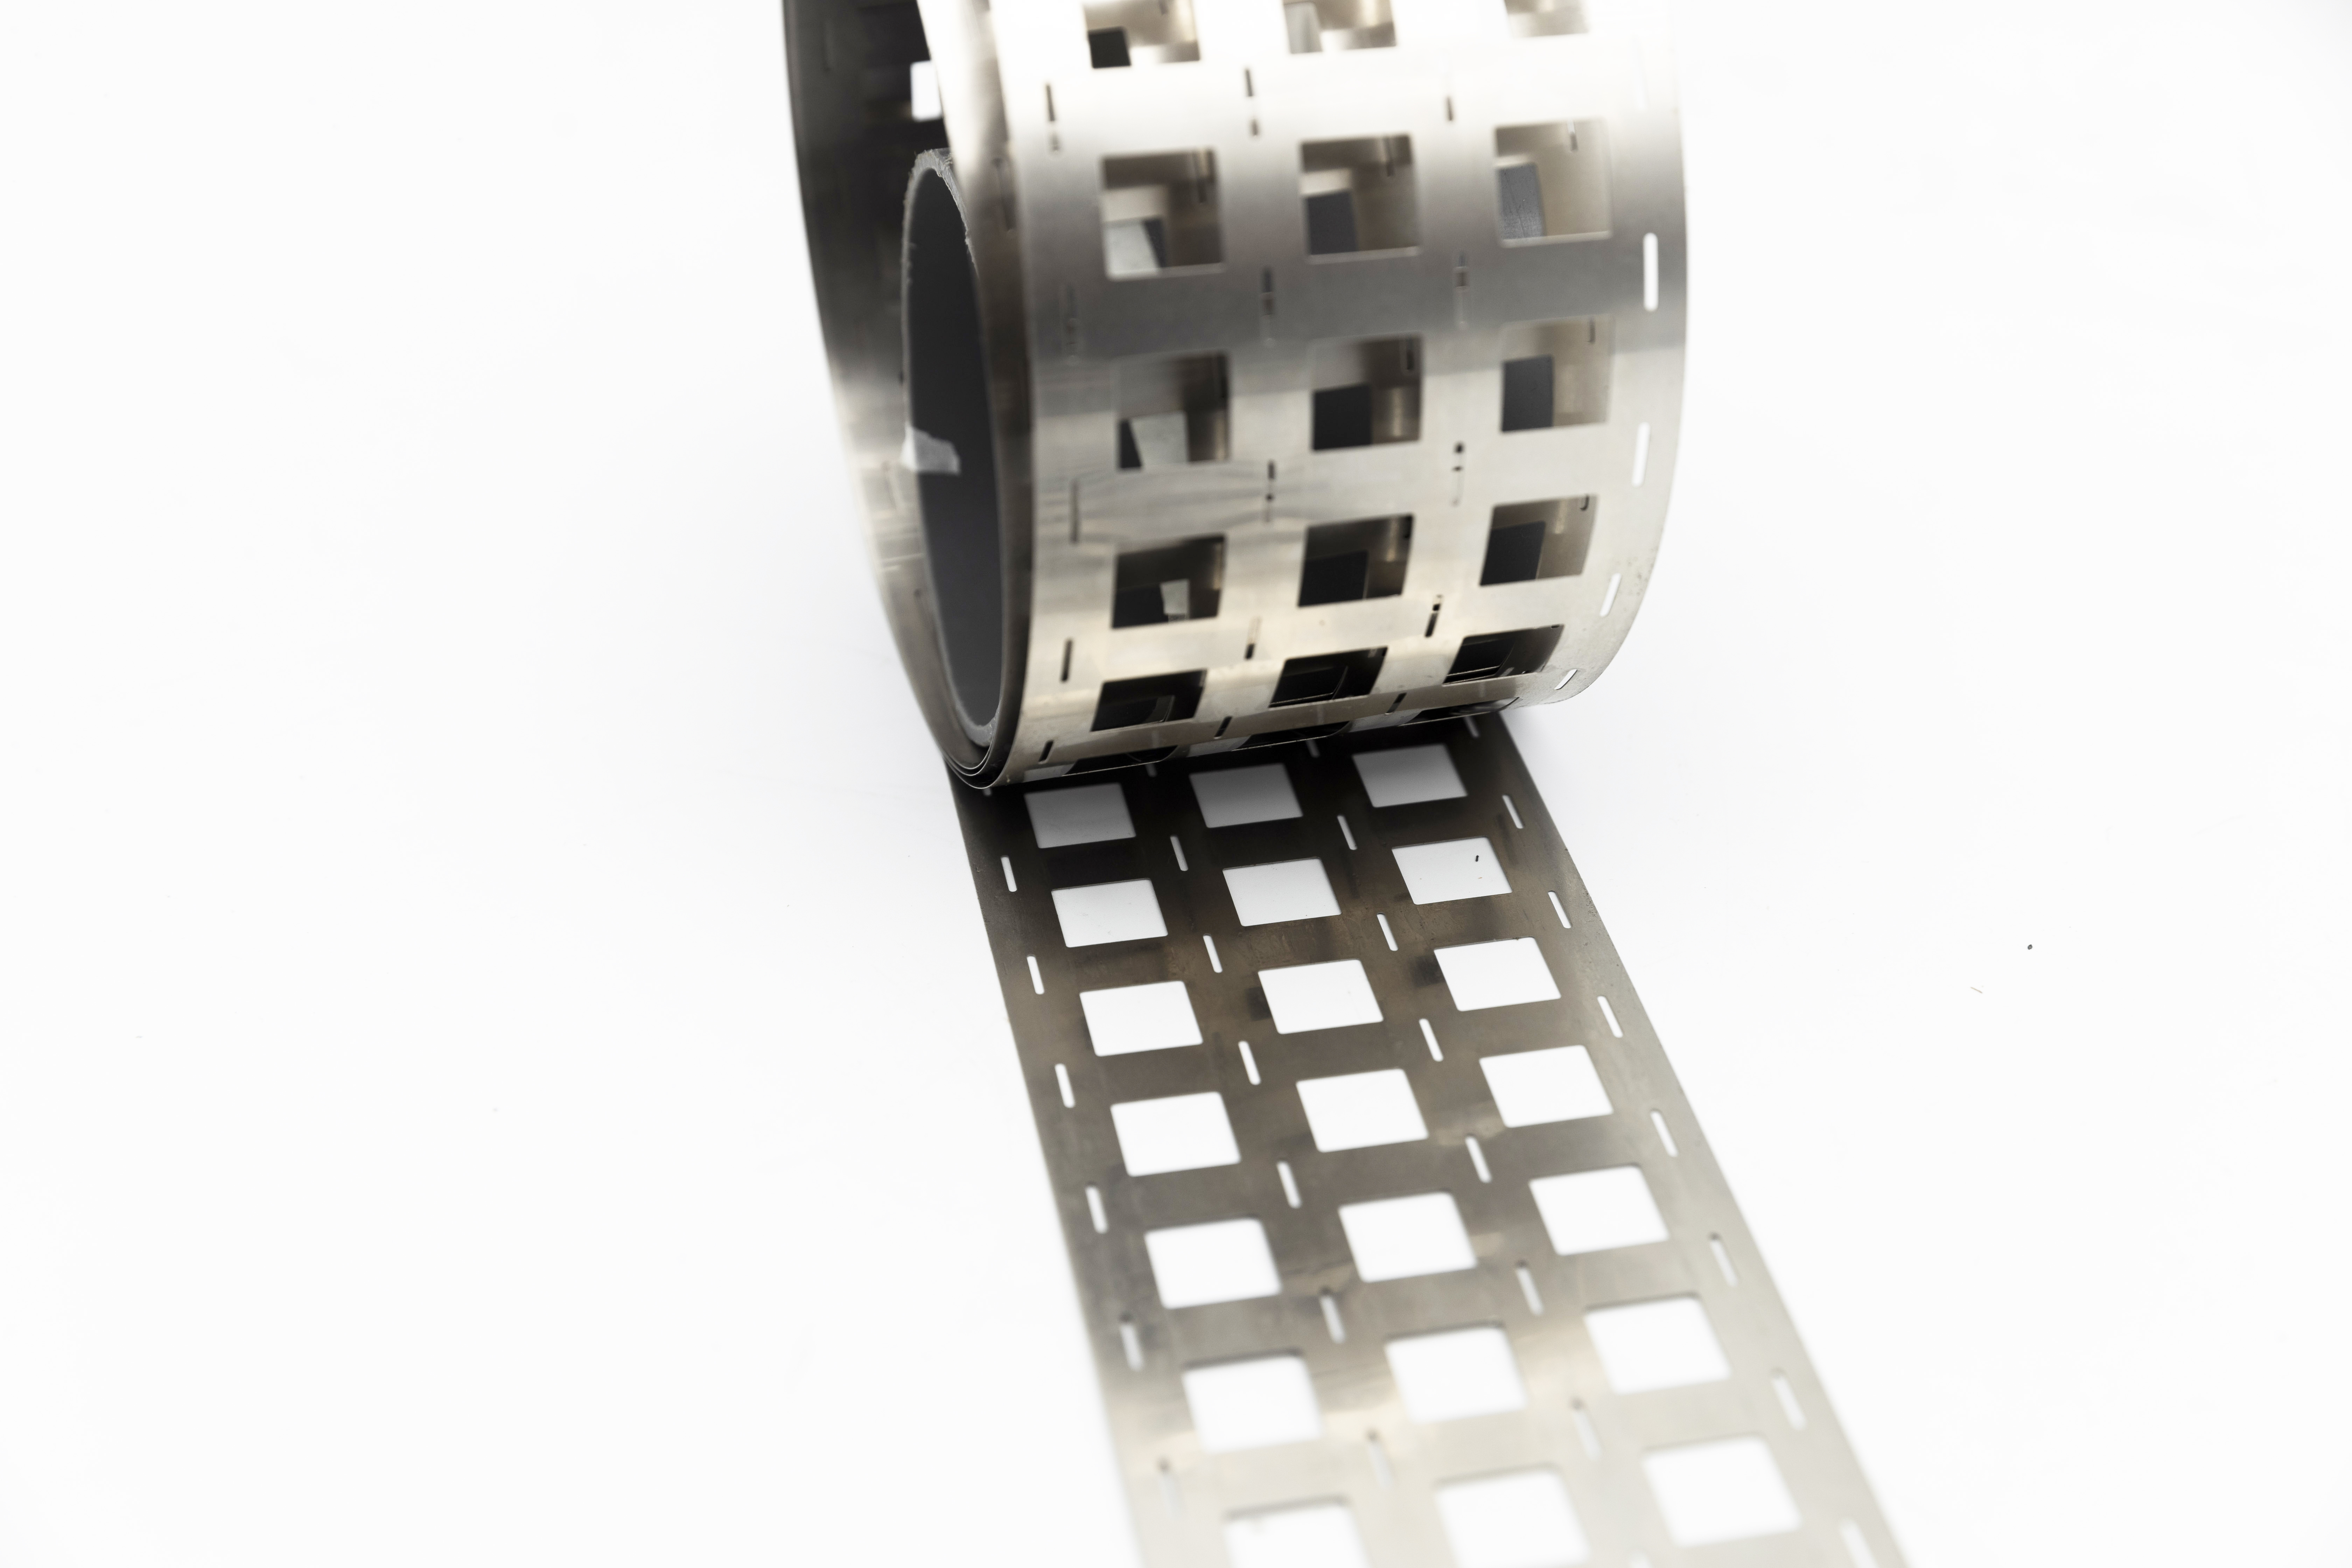
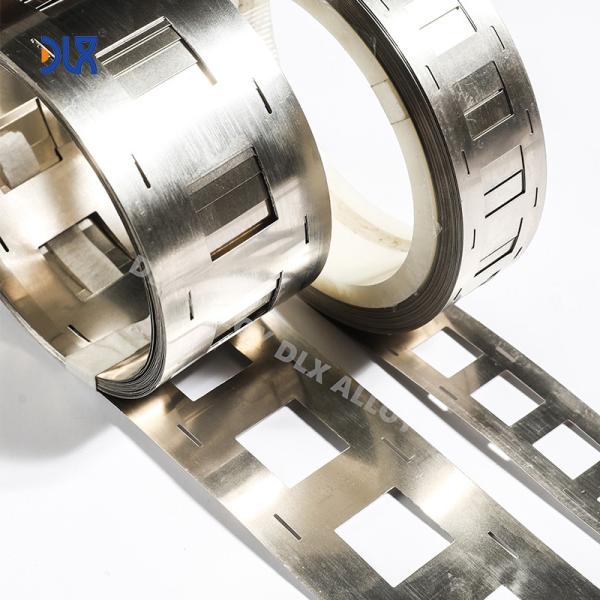
DLX Alloy supplies 2P pure nickel welding strip for 18650 battery pack assembly and industrial battery manufacturing applications. Designed for battery pack connection processes, this strip is available in pure nickel material options, including Ni200 and Ni201, subject to grade and specification confirmation.
For battery manufacturers, battery pack assemblers, OEMs and industrial distributors, selecting the right nickel strip requires more than matching a material name. Strip thickness, width, connection layout, material composition and welding process compatibility all influence production consistency and assembly performance.
DLX Alloy supports B2B buyers with material selection, dimension confirmation, customized supply requirements and quotation services. Contact our team with your battery configuration and technical requirements to confirm the appropriate specification.

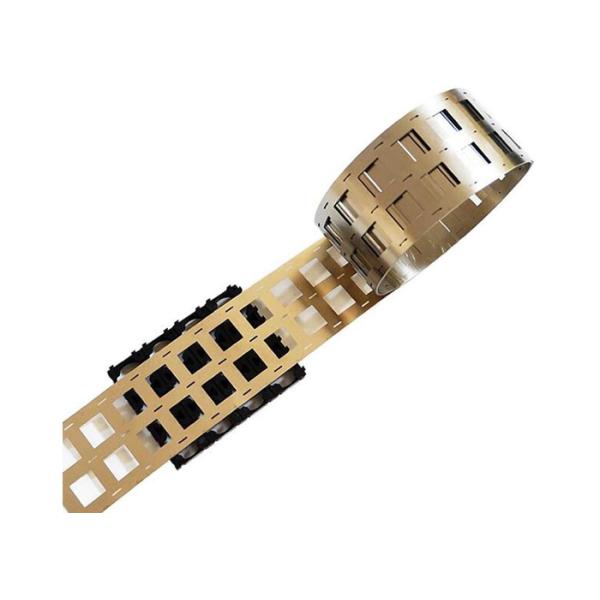
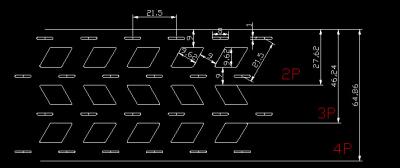
The 2P pattern is produced for 18650 battery packs, with strip thickness of 0.05-0.5 mm (hot-sale 0.15/0.2 mm) and a battery width series of 2-15 mm. Pattern geometry, available space and tolerances are confirmed against the drawing before production and locked in the batch record.
Key Product Features

Ni200 and Ni201 pure nickel options are available subject to the required grade and applicable material standard.
The product is intended for 2P battery interconnection layouts. The final pattern, cell arrangement and connection dimensions should be confirmed against the customer's drawing.
Thickness, width, pitch and finished geometry can be specified according to project requirements, subject to production feasibility and confirmation.
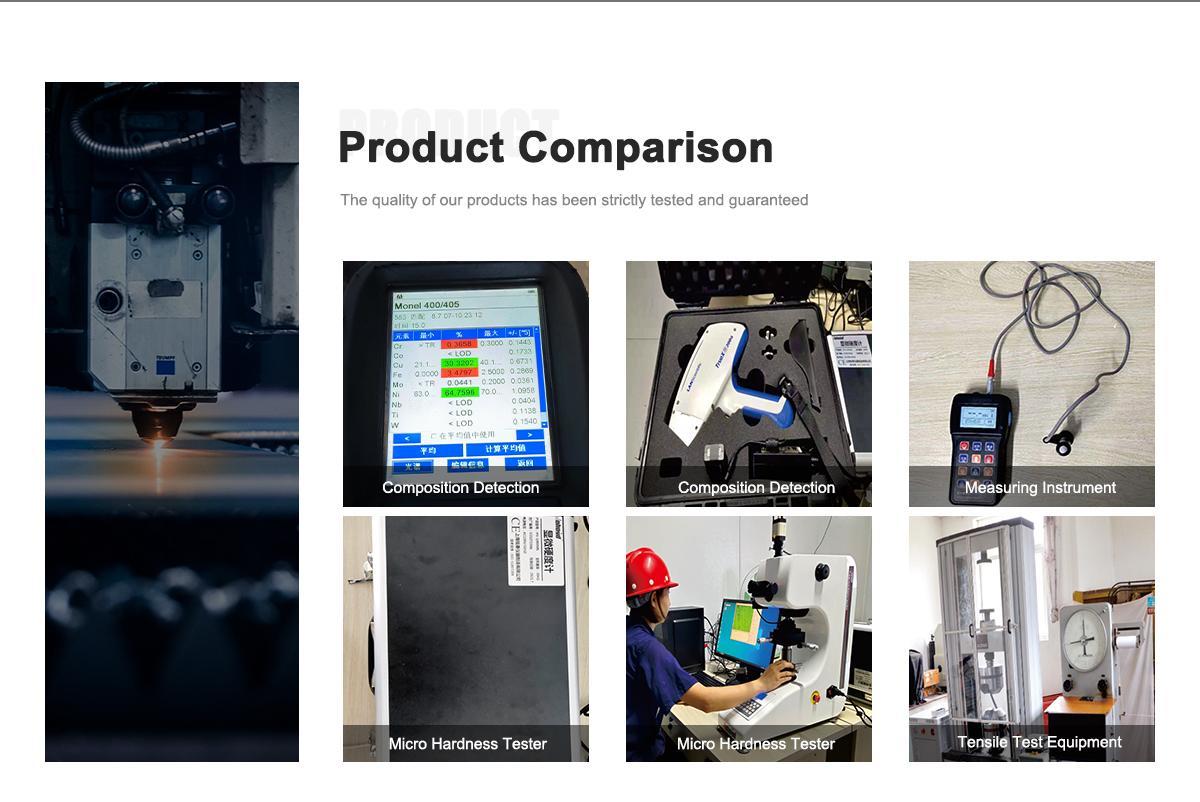
Dimensional inspection, material documentation and surface checks can be discussed according to the agreed purchase specification. Applicable inspection records should be confirmed before ordering.
Technical Considerations for Battery Pack Assembly
A 2P battery pack typically refers to two cells connected in parallel within the relevant battery configuration. The strip geometry and connection points depend on the actual pack design. Buyers should provide a technical drawing to confirm the intended 2P pattern and finished dimensions.
The electrical resistance of a battery interconnection depends on material resistivity, strip dimensions, current path length, contact conditions and weld quality. Material data alone cannot determine the performance of the completed connection.
Welding results depend on the strip material and thickness, cell terminal material, electrode condition, welding parameters and equipment. Buyers should evaluate representative samples under their intended production conditions before approving a material for mass production.
| Item | Detail |
|---|---|
| Product standards | ASTM B162 (nickel and nickel alloy plate, sheet and strip); GB/T 2072-2020 (nickel and nickel alloy strip) |
| Mill documentation | EN 10204 3.1 mill test certificates, batch composition and dimensional records |
| Management system | ISO 9001 certified; SGS audited |
| Traceability | Batch numbers tied to the drawing from melt to shipment |
| Grade | Ni Content | Best Application | Reference Price (FOB, USD/kg) |
|---|---|---|---|
| N4 (NP1) | ≥99.9% | Vacuum electronics | 420-480 |
| Ni201 | ≥99.0% | High-temp service | 350-390 |
| Ni200 | ≥99.2% | Battery, chemical | 340-380 |
| N6 (NP2) | ≥99.5% | Industrial corrosion | 300-340 |
The bands above are indicative for standard strip sizes. Pattern products (2P) are quoted per drawing — pattern geometry, grade, thickness, width and quantity determine the final price.
| Element (wt%) | N4 | N6 | Ni201 | Ni200 |
|---|---|---|---|---|
| Ni | — | — | ≥99.0 | ≥99.2 |
| Ni+Co | 99.9 | 99.5 | — | — |
| Cu | ≤0.015 | 0.1 | ≤0.25 | ≤0.25 |
| Si | ≤0.03 | 0.1 | ≤0.35 | ≤0.35 |
| Mn | ≤0.002 | 0.05 | ≤0.35 | ≤0.35 |
| C | ≤0.01 | 0.1 | ≤0.02 | ≤0.15 |
| Mg | ≤0.01 | 0.1 | — | — |
| S | ≤0.001 | 0.005 | ≤0.01 | ≤0.01 |
| P | ≤0.001 | 0.002 | — | — |
| Fe | ≤0.04 | 0.1 | ≤0.4 | ≤0.4 |
| Property | Value |
|---|---|
| Density | 8.908 g/cm³ |
| Melting Point | 1435-1446 °C |
| Curie Temperature | 358 °C |
| Tensile Strength | ≥462 MPa (annealed) |
| Elongation | ≥35% (annealed) |
| Hardness | 90-120 HB |
| Electrical Resistivity | 0.096 μΩ·m (20 °C) |
| Thermal Conductivity (Ni200) | 70.2 W/m·K |
| Item | Detail |
|---|---|
| Strip Pattern | 2P (2 parallel cells) |
| Compatible Cells | 18650 battery packs |
| Thickness | 0.05-0.5 mm (hot-sale 0.15/0.2 mm) |
| Width | 2-15 mm battery series |
| Custom Sizes | Per drawing (pattern geometry per drawing) |
| Tolerance | Per drawing, locked in batch record |
| Condition | Annealed (soft) standard |
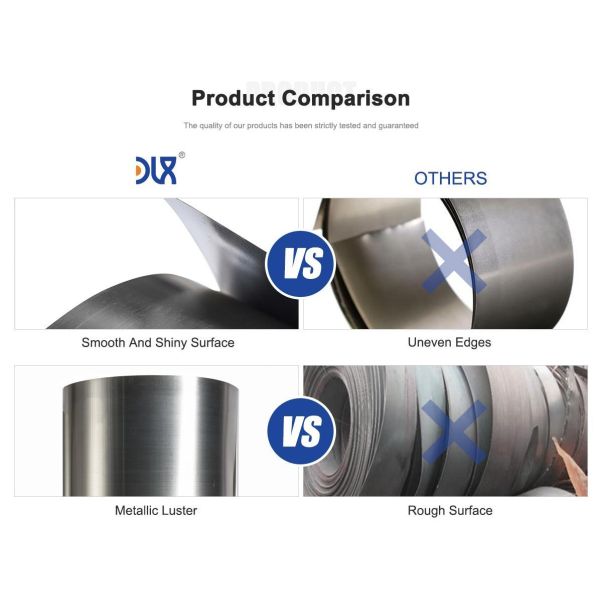
| Surface | Clean, smooth, burr-free |
| Applicable Standards | ASTM B162; GB/T 2072-2020 |


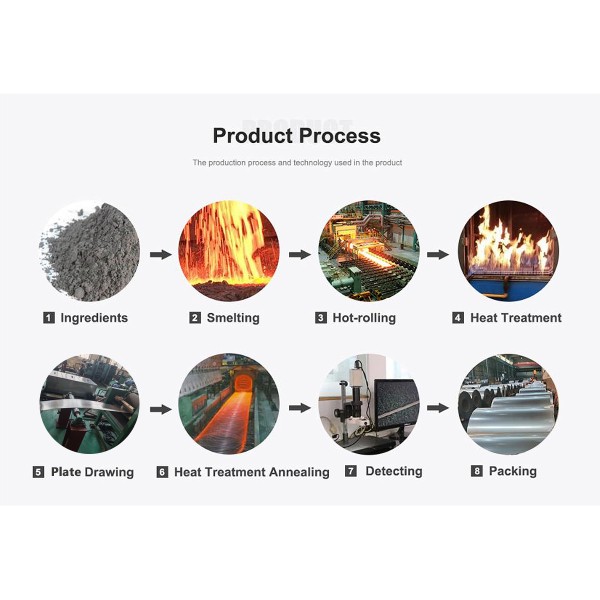
Quality control starts at the melt: raw material composition is verified against UNS N02200/N02201 before rolling, then every batch is gauged for thickness, width and surface condition, and punched patterns are checked for burr and dimensional accuracy against the drawing. Batch records link each order back to the melt, and EN 10204 3.1 mill test certificates ship with every consignment.

2P welding strip is supplied in rolls or cut lengths, edge-protected and moisture-wrapped, then packed in cartons and export wooden cases. Documentation — mill test certificates, batch records and packing lists — accompanies every order, with a standard lead time of 7-15 days from confirmed drawing.

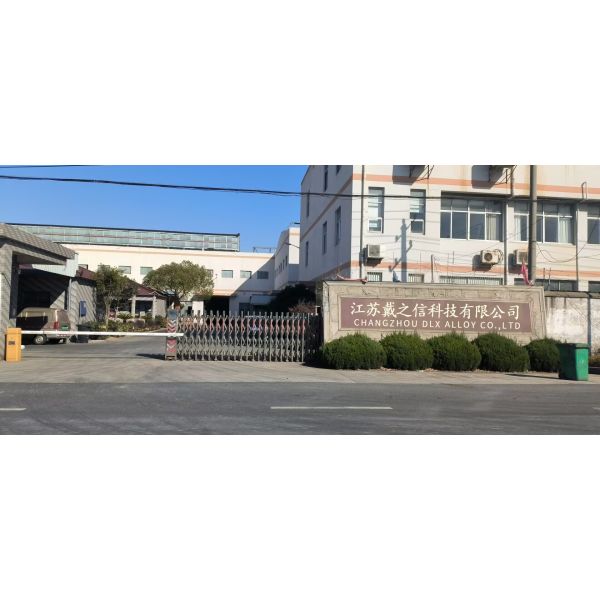
A welding strip is judged by the current it carries across a weld for years. DLX Alloy has run a nickel-only line since 2002 — 12,000 m² of floor space, 1,200 t/yr rated capacity, ISO 9001 certified and SGS audited — punching battery strip to per-drawing patterns, with per-batch composition analysis and EN 10204 3.1 mill test certificates on every shipment.
2P as specified; 3P/4P/5P and other pattern layouts can also be produced per drawing.
Hot-sale thicknesses of 0.15/0.2 mm and battery widths of 2-15 mm; custom per drawing.
Ni200 (≥99.2% Ni) is standard for battery welding strip; Ni201 (≥99.0% Ni, low carbon) covers elevated-temperature service.
5 kg; sample and trial quantities can be discussed per request.
7-15 days from confirmed drawing; EN 10204 3.1 mill test certificates, batch records, ISO 9001/SGS certificates and packing list.