Technical & Engineering-Focused (Ideal for Website Product Pages, Technical Data Sheets)
Title: The 6 mm PCD Micro-Boring Bar: Engineering Certainty in Sub-Millimeter Tolerance Zones
When the machining envelope shrinks to the interior of wristwatch movements, smartphone mid-frame cavities, or thin-wall copper fittings, every micron of tool deflection writes itself directly into the bore wall. Conventional steel shanks at 6 mm diameter flex under cutting loads—especially at deeper reaches—introducing taper, roundness error, and regenerative chatter.
Stiffness is the physical prerequisite for precision.
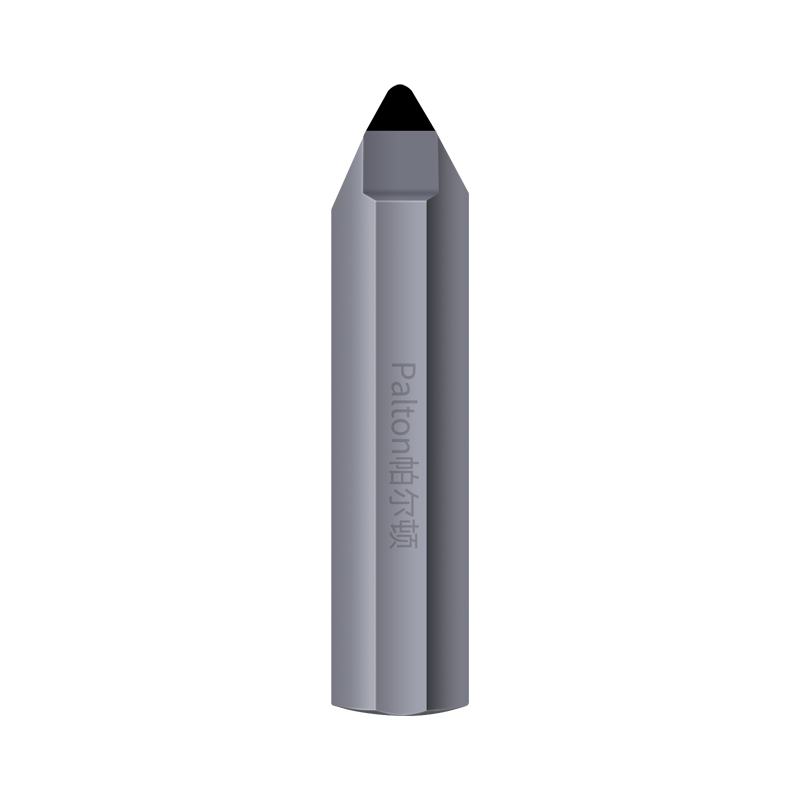
The Palton 6 mm PCD micro-boring bar features a one-piece solid carbide shank, offering an elastic modulus approximately three times that of tool steel. This dramatically reduces tool deflection at the source. Vibration energy is dissipated at the tool-workpiece interface rather than transmitted to the finished surface. The operator's tangible result: true roundness, straight cylindrical walls, surface roughness profiles free of periodic waveforms, and Cpk values that remain stable across thousands of consecutive parts.
PCD Material: A Chemical "Passivation" for Aluminum Machining.
For aluminum alloys—particularly hypereutectic grades like A390—the PCD tip exhibits near-zero chemical affinity with aluminum, fundamentally eliminating built-up edge (BUE) formation at the metallurgical level. Its coefficient of friction is approximately 40% lower than that of coated carbide, and cutting heat is rapidly conducted into the chip stream and evacuated. Edge sharpness is preserved even under high-speed dry machining or MQL (Minimum Quantity Lubrication) conditions.
Grinding-Grade Surface Finish, One Operation Earlier.
On ADC12 die-cast aluminum, the PCD micro-boring bar consistently delivers mirror-quality internal bores at Ra ≤ 0.2 μm with minimal scatter. When the surface finish requirement moves from Ra 0.8 μm down to Ra 0.2 μm, secondary operations such as roller burnishing or honing can be removed from the process routings. Cycle time per part compresses, and throughput bottlenecks dissolve.
Material Coverage Matrix (Non-Ferrous Spectrum):
-
Aluminum & High-Si Alloys: 6061, 7075, 2024, A356, A380, ADC12, hypereutectic grades
-
Copper & Alloys: Pure copper, brass, bronze, beryllium copper
-
Specialty Materials: Magnesium alloys, CFRP, GFRP, graphite, high-temperature engineering plastics
Delivery & Customization:
Standard stocked items ship in 3–7 working days; custom-engineered tools (shank diameters 2–8 mm, overall length, edge geometry) deliver in 10–18 working days. Batch tolerance control to ±0.005 mm, with full re-grinding service support throughout the tool lifecycle.